
Case 1
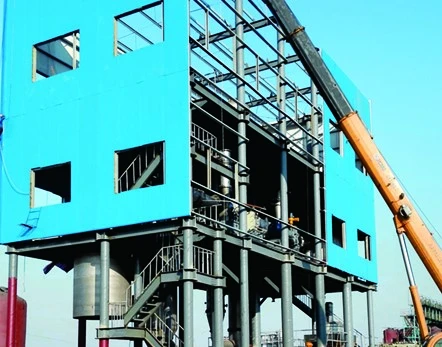
MVR Evaporation Project for Wastewater Treatment with an Evaporation Capacity of 9 Tons per Hour

Case 2
MVR Evaporation Project Currently Under Construction for a Client
Case 3
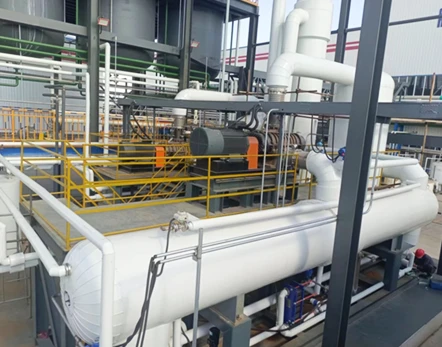
Henan Heptahydrate Zinc Sulfate Project
Following the project upgrade, the evaporation cost per ton of heptahydrate zinc sulfate was reduced by 500 yuan compared to the original evaporation equipment. With an annual production capacity of 10,000 tons, this results in annual savings of 5 million yuan
Case 4
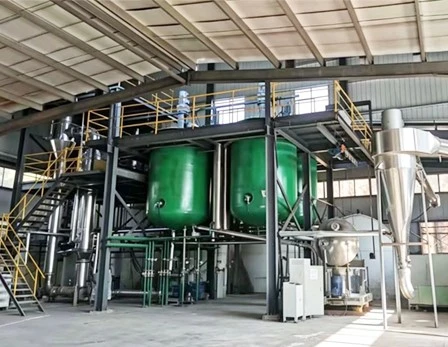
Shanxi Heptahydrate Zinc Sulfate Project
From crystallization process optimization to equipment development, design, installation, commissioning, and operation, Zhuolian Ruike provided the client with a complete R&D and process chain service. The pilot production line, with an annual output of 4,000 tons, has an energy consumption of approximately 191 yuan per ton of product.
Case 5
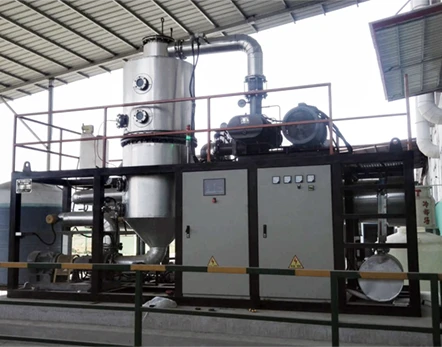
Jiangxi Zinc Sulfate Heptahydrate Project
The skid-mounted zinc sulfate heptahydrate equipment features low energy consumption and produces a product that does not caking.
Case 6
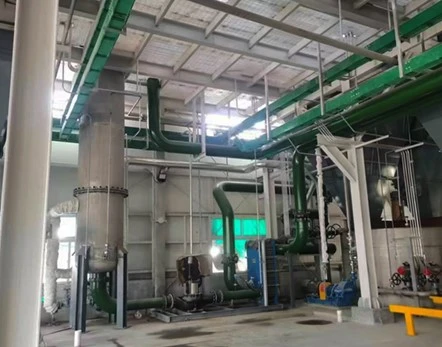
Shandong Project
We configured an automatic control system for the client that automatically detects temperature and adjusts heating/cooling, maintaining the equipment, water, and ambient temperatures at set values. This results in minimal temperature fluctuations and eliminates the need for manual adjustments.