
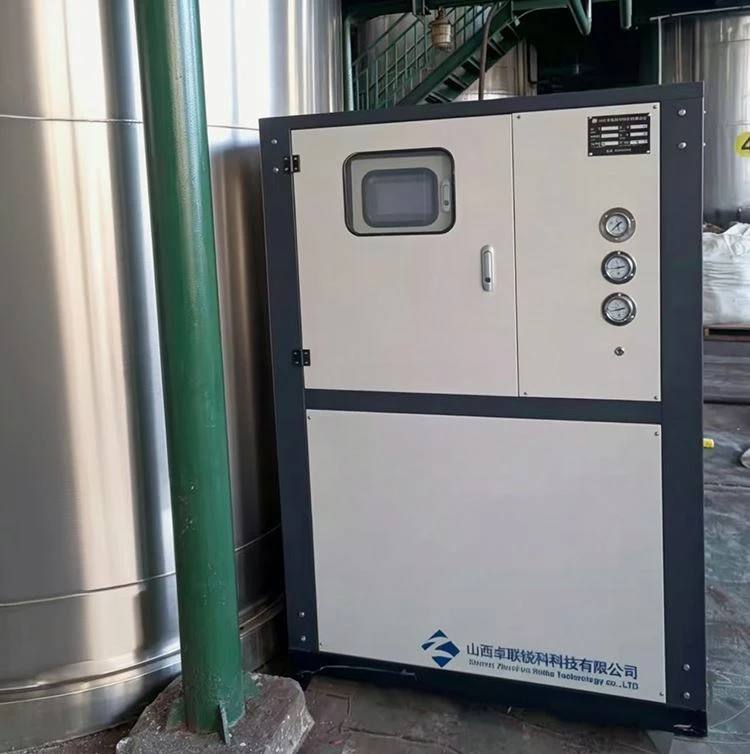
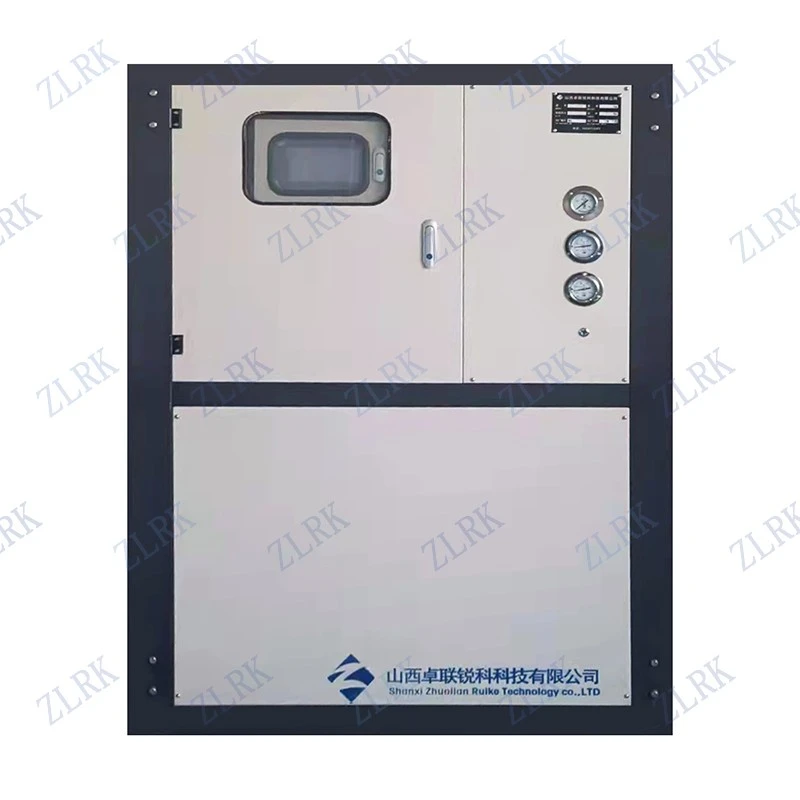
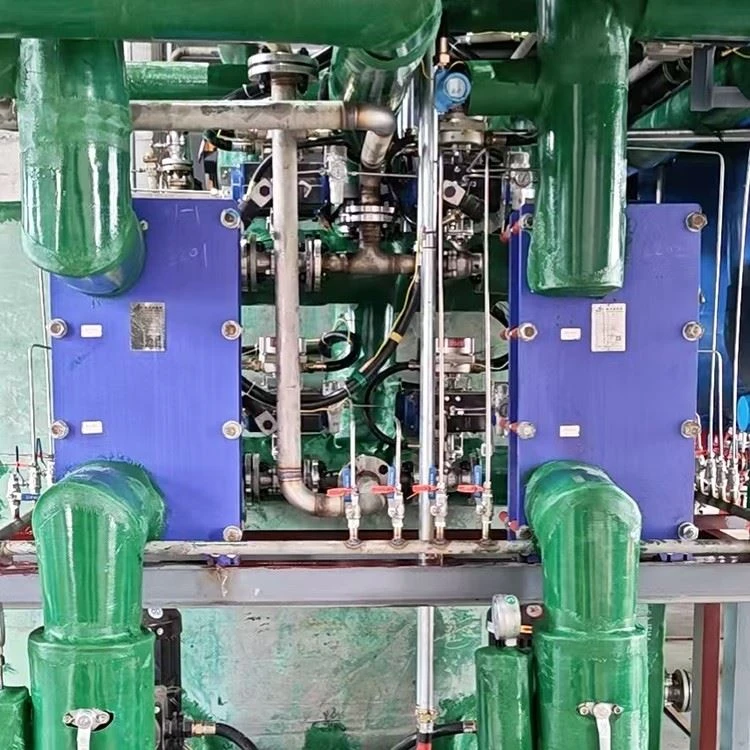
Product Preview
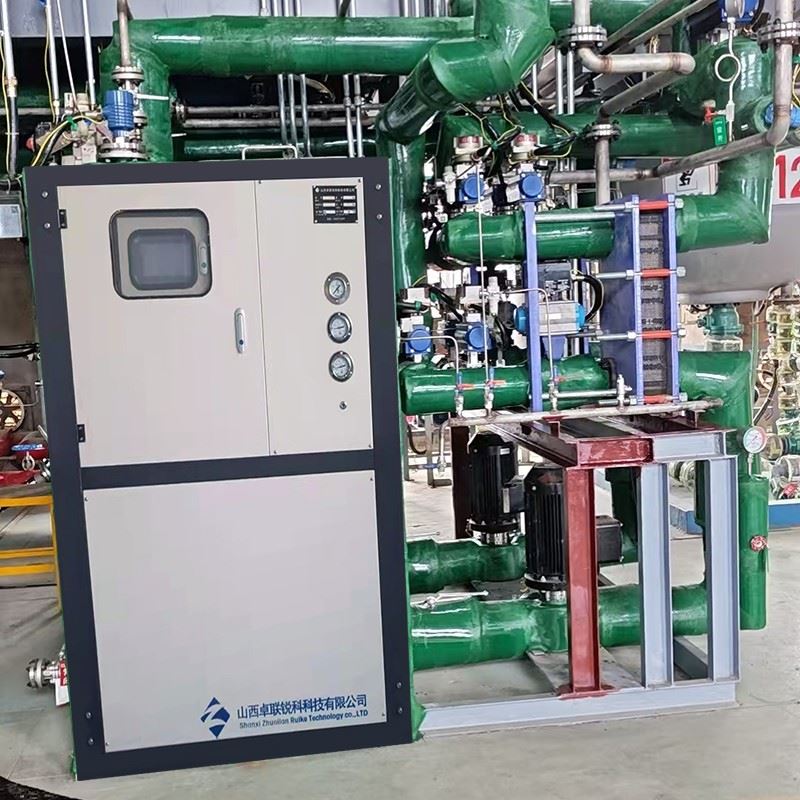
Exclusively engineered and self-developed for heavy-duty 85m3 ultra-large industrial crystallizers, this professional constant temperature controller is a high-load industrial temperature regulation solution tailored for super-scale continuous crystallization production. Unlike conventional temperature control units designed for small and medium-volume tanks, this model is fully optimized for the extreme thermal inertia, ultra-large fluid volume, and vertical-horizontal multi-dimensional temperature difference characteristics unique to 85m3 crystallization systems.
It solves prominent industrial pain points including slow thermal response, cross-layer temperature imbalance, and unstable crystal forming quality in super-large tank batch production. Built for non-stop heavy industrial operation, this dedicated controller delivers high-precision full-tank temperature synchronization, supporting high-efficiency, standardized and low-consumption production for super-large chemical bases, environmental protection zero-discharge projects and mineral resource purification industries.
Working Principle
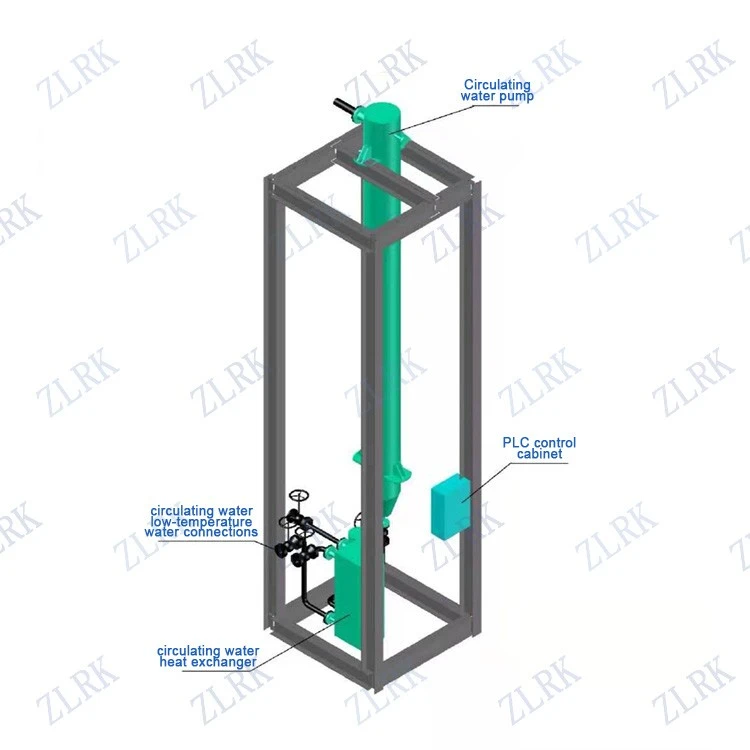
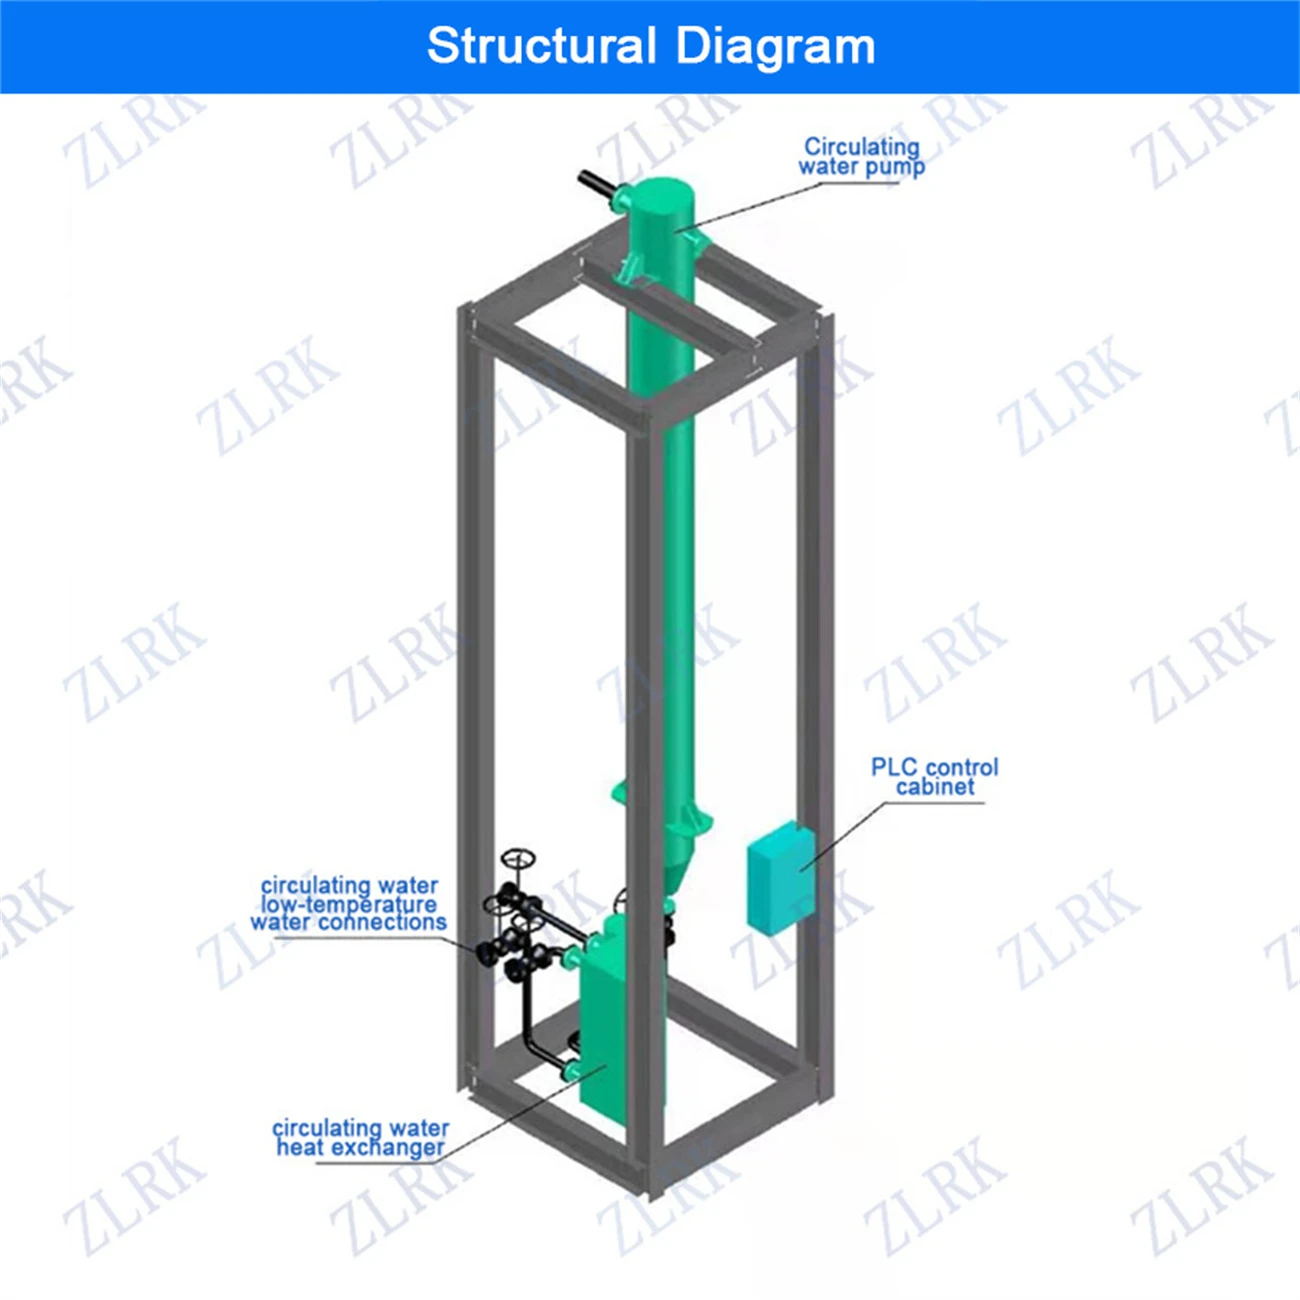
This 85m3 crystallizer matching constant temperature controller adopts a heavy-duty integrated modular architecture, composed of a high-power frequency conversion temperature regulation unit, multi-layer cross-regional sensing system, industrial adaptive core chip and full-range safety linkage protection module. Breaking the limitation of traditional single-plane temperature monitoring, it adopts a three-dimensional grid sensing layout covering the top flow layer, middle static layer and bottom deposition layer of the 85m3 super-large tank, completely eliminating temperature dead zones and layered deviation in ultra-large capacity solutions.
In continuous industrial operation, the grid sensing system collects real-time temperature data of all tank areas and transmits signals for high-speed operational analysis. Aiming at the inherent thermal hysteresis of 85m3 massive solution systems, the equipment adopts dual dynamic regulation of feed-forward prediction and real-time fine correction. It intelligently matches heating and cooling power according to solution viscosity, solid content and ambient working conditions, and adjusts circulating flow parameters in real time to balance the overall temperature field. This stable and accurate temperature control mode standardizes the whole crystal nucleation and growth process, effectively improving batch production consistency and finished product qualification rate of super-large crystallization equipment.
Core Application Scenarios
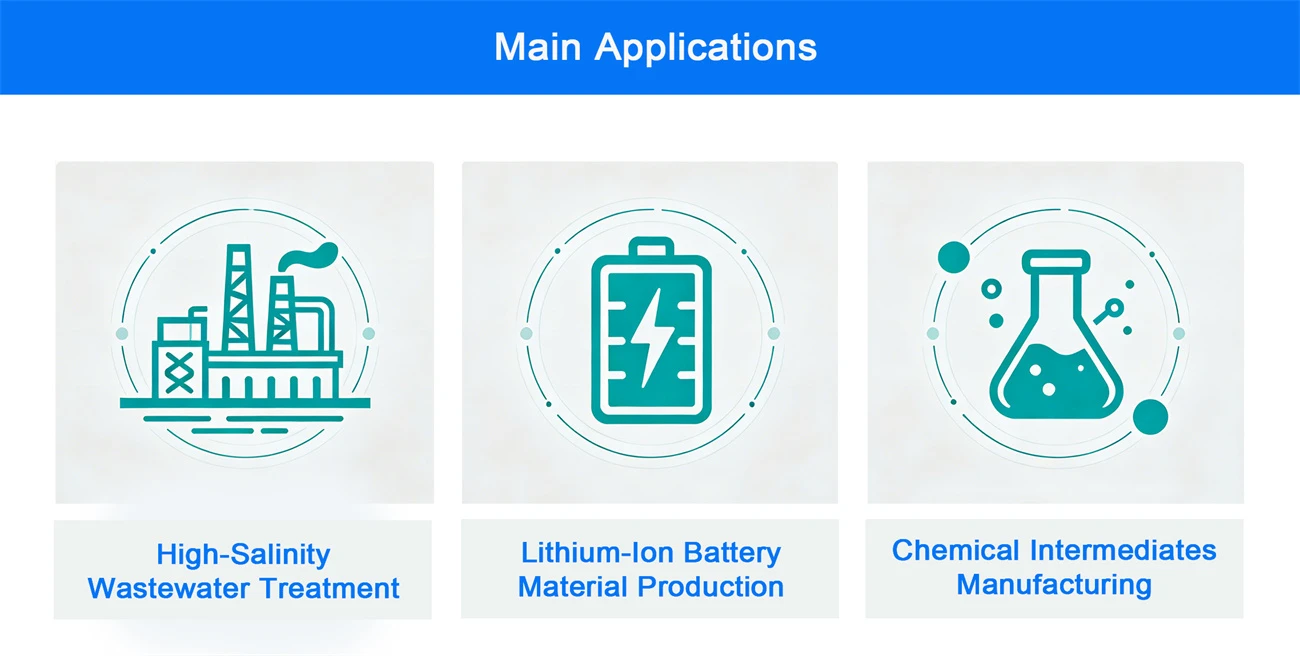
Optimized exclusively for 85m3 ultra-large crystallizer heavy-load working conditions, this temperature controller is widely applied in super-scale industrial production and resource.
Super-Large Mineral Salt Deep Purification: Suitable for large-scale crystallization and high-purity refining of barium salt, calcium salt and other high-value mineral salts. It stabilizes the overall temperature field of 85m3 super-large tanks, standardizes crystal growth cycles, and improves product density and purity for high-end industrial salt supply.
Centralized Industrial Wastewater Treatment: Perfect for super-large park-level high-salt wastewater zero-discharge projects. It maintains stable evaporation and crystallization temperature, improves salt-water separation efficiency and solid-liquid purification accuracy, meeting strict international environmental protection and resource recycling standards.
High-Purity Chemical Mass Production: Adaptable to large-batch crystallization of high-purity chemical raw materials and heat-sensitive intermediates. Accurate cross-layer temperature control avoids material pyrolysis and oxidation deterioration, effectively lifting overall production yield and product stability.
Industrial Grade New Energy Material Processing: Matches super-large crystallization production lines for industrial new energy auxiliary materials. It eliminates mass quality fluctuation caused by temperature deviation in ultra-large volume production, supporting stable batch delivery for large new energy industrial bases.
Core Manufacturer & Product Competitive Advantages
1. Exclusive 85m3 Super-Large Tank Parameter Calibration
Universal temperature controllers cannot adapt to the super thermal storage capacity and three-dimensional temperature gradient of 85m3 crystallization tanks, resulting in poor regulation accuracy. Our equipment undergoes exclusive structural optimization and program iteration targeting 85m3 tank volume and fluid operation characteristics, with customized power configuration and cross-layer balance regulation logic. The overall equipment matching degree and operation stability far exceed universal industrial temperature control products.
2. Feed-Forward Intelligent Regulation & Ultra-Stable Precision
Equipped with a self-developed super-large volume dedicated algorithm, the system realizes temperature trend pre-judgment and active power compensation, fundamentally solving the thermal lag defect of 85m3 high-load operation. The full-tank temperature fluctuation is strictly controlled within ±0.1℃, ensuring uniform crystal particle size and consistent purity for each production batch and enhancing core product competitiveness.
3. Harsh Environment Resistant & Low Energy Consumption Operation
The whole machine adopts upgraded industrial heavy-duty anti-corrosion, explosion-proof and dust-proof configuration, with core components customized for long-term full-load cyclic operation of 85m3 crystallizers, adapting to complex and harsh chemical production environments. The intelligent load energy-saving system dynamically adjusts operating power, reducing comprehensive energy consumption by 23%-30% compared with traditional high-power temperature control equipment and cutting long-term operational costs.
4. Full-System Intelligent Linkage & Remote Management
It supports seamless docking with industrial DCS, PLC and cloud monitoring systems, realizing integrated linkage of temperature regulation, operational data statistics and fault early warning. Equipped with an industrial anti-interference touch screen and remote cloud control function, it supports one-key parameter calling and unattended operation, reducing manual operation costs and realizing intelligent management of super-large production lines.
Innovation R&d & Precision Engineering Design
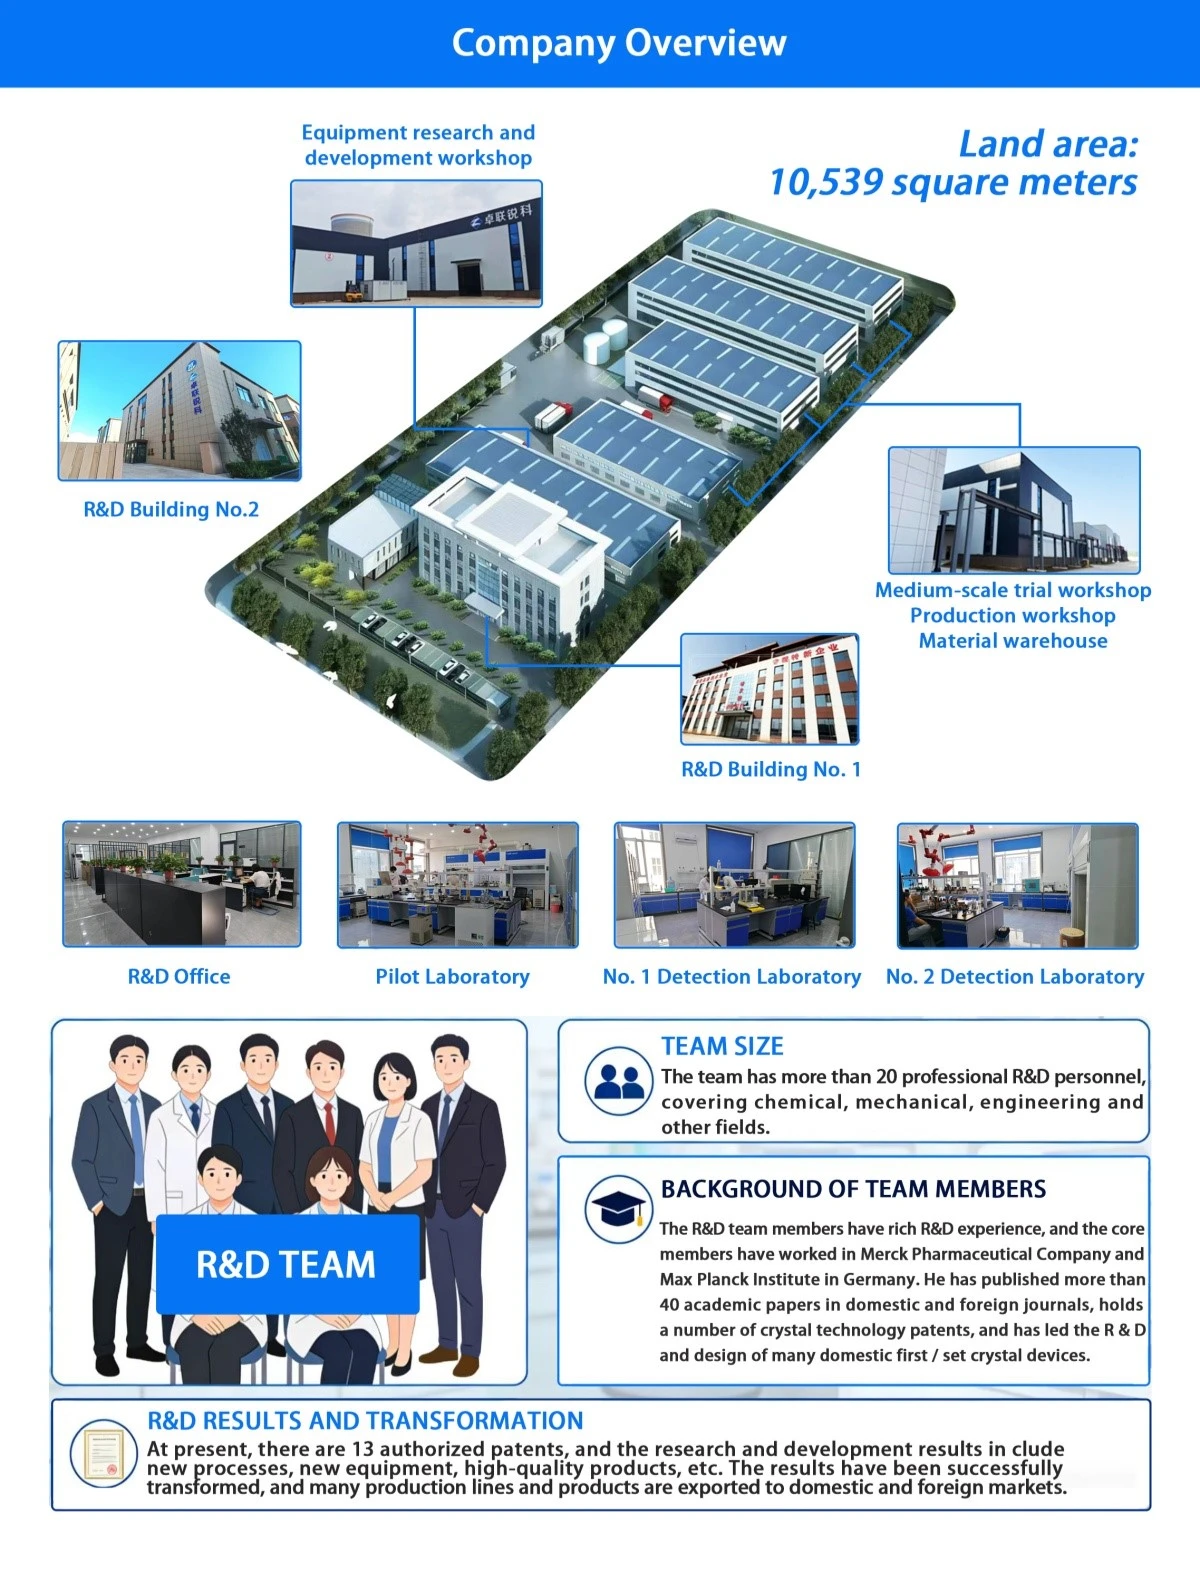
Our R&D team focuses on technical research of temperature control systems for super-large volume crystallization equipment. Targeting the unique industry pain points of unbalanced cross-layer temperature and slow heat transfer efficiency of 85m3 crystallizers, we have completed dozens of super-large flow field simulation tests and extreme working condition iterations.
The independently developed control program is highly adapted to the heat storage and dissipation rules of 85m3 ultra-large solution systems. All key accessories adopt national industrial standard high-grade parts, and each equipment undergoes 120-hour full-load continuous operation test, extreme temperature impact test and anti-interference calibration before delivery. We provide personalized parameter debugging and functional customization according to customer material properties and production process requirements.
Domestic Project Application Experience
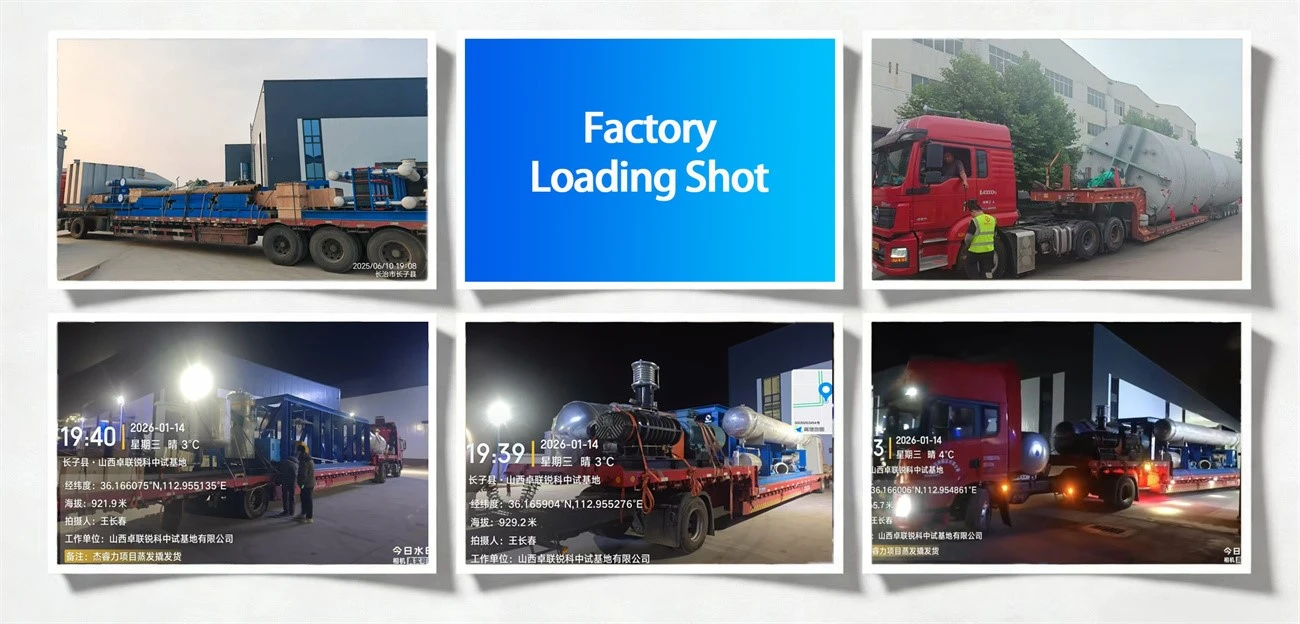
Our 85m3 dedicated constant temperature controllers have been widely applied in multiple domestic super-large chemical industrial parks, environmental protection zero-discharge demonstration projects and new energy bulk material production bases.
We have accumulated rich mature practical experience in temperature control for super-scale continuous crystallization lines, adapting to high-strength, long-cycle industrial production demands.
All delivered equipment operates stably with ultra-low failure rate, effectively helping domestic large-scale enterprises optimize production processes, stabilize batch product quality and improve overall production benefits.
Full-lifecycle Professional After-sales Service
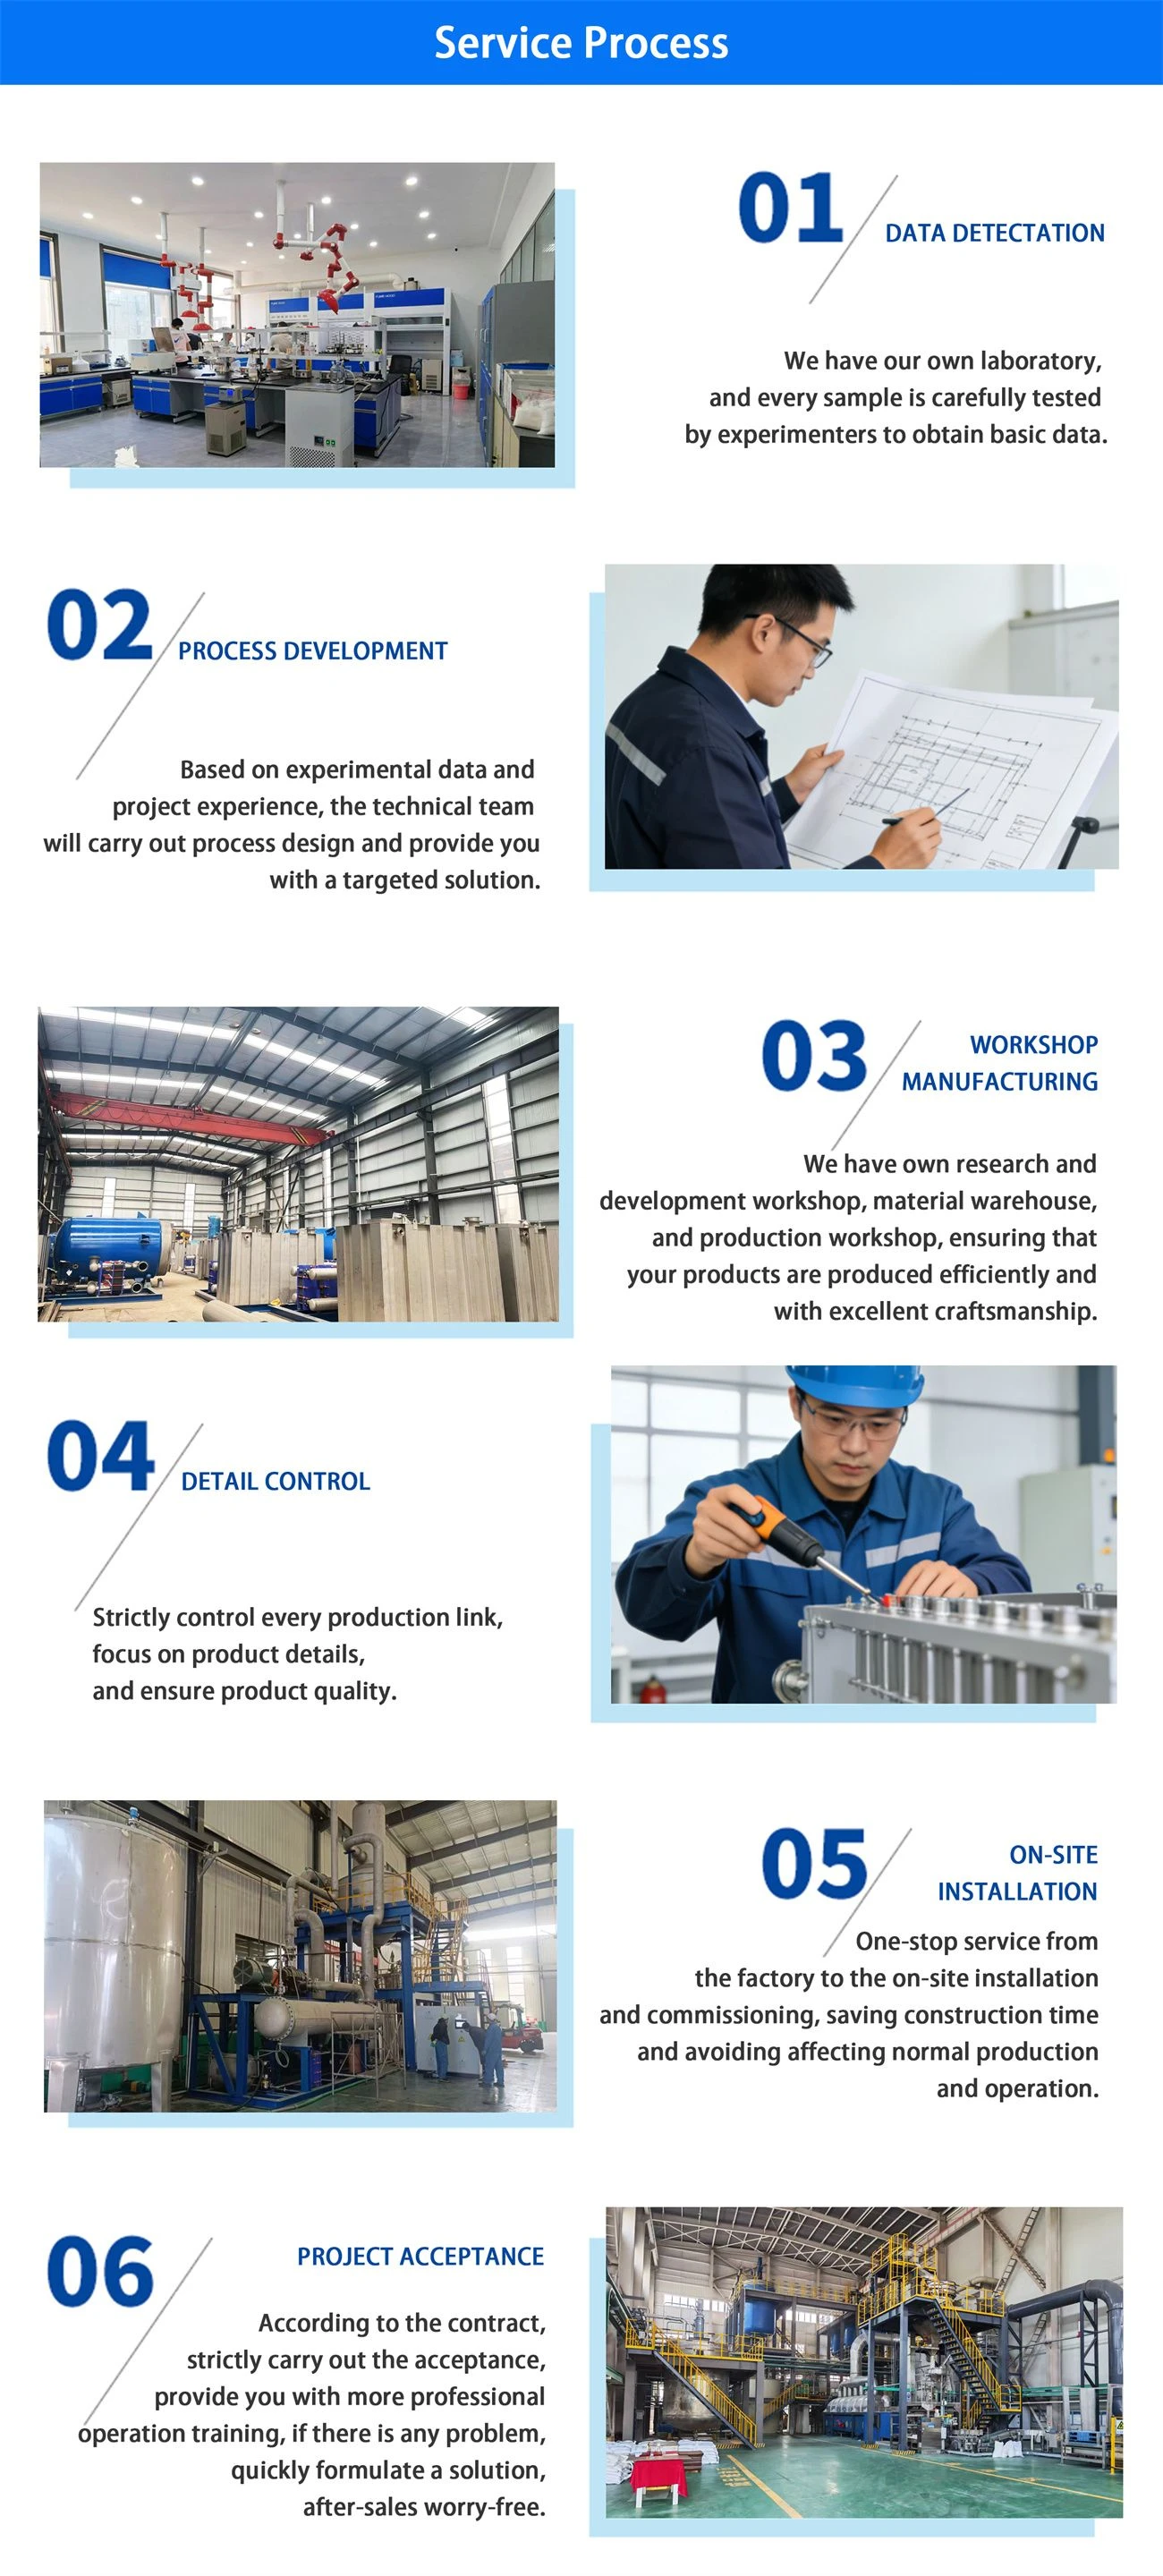
We provide global customers with one-stop full-lifecycle supporting services. In the pre-sale phase, we offer free working condition evaluation, production capacity matching analysis and personalized temperature control scheme design.
During installation and commissioning, we provide professional remote guidance and standardized operator training to ensure rapid production launch.
In the after-sale phase, we implement 24-hour rapid response mechanism, global spare parts supply, regular equipment maintenance and free system upgrade services, fully guaranteeing the long-term stable and efficient operation of customers' 85m3 super-large crystallization production lines.
Contact our team today to acquire detailed equipment parameters, authentic domestic project cases and factory preferential quotations, and customize exclusive temperature control solutions for your super-large crystallization production line!
Hot Tags: constant temprature controller for 85m³, China constant temprature controller for 85m³ manufacturers, suppliers, factory


