

Product categories
MVR Evaporators
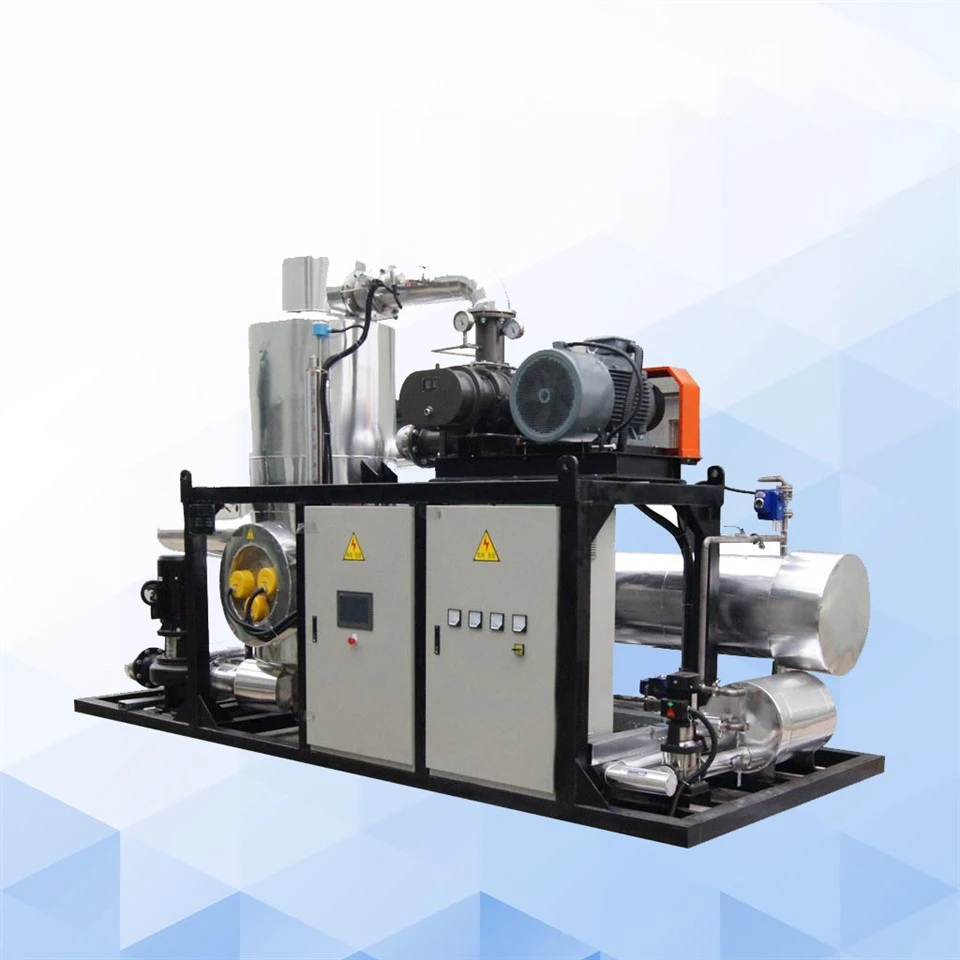
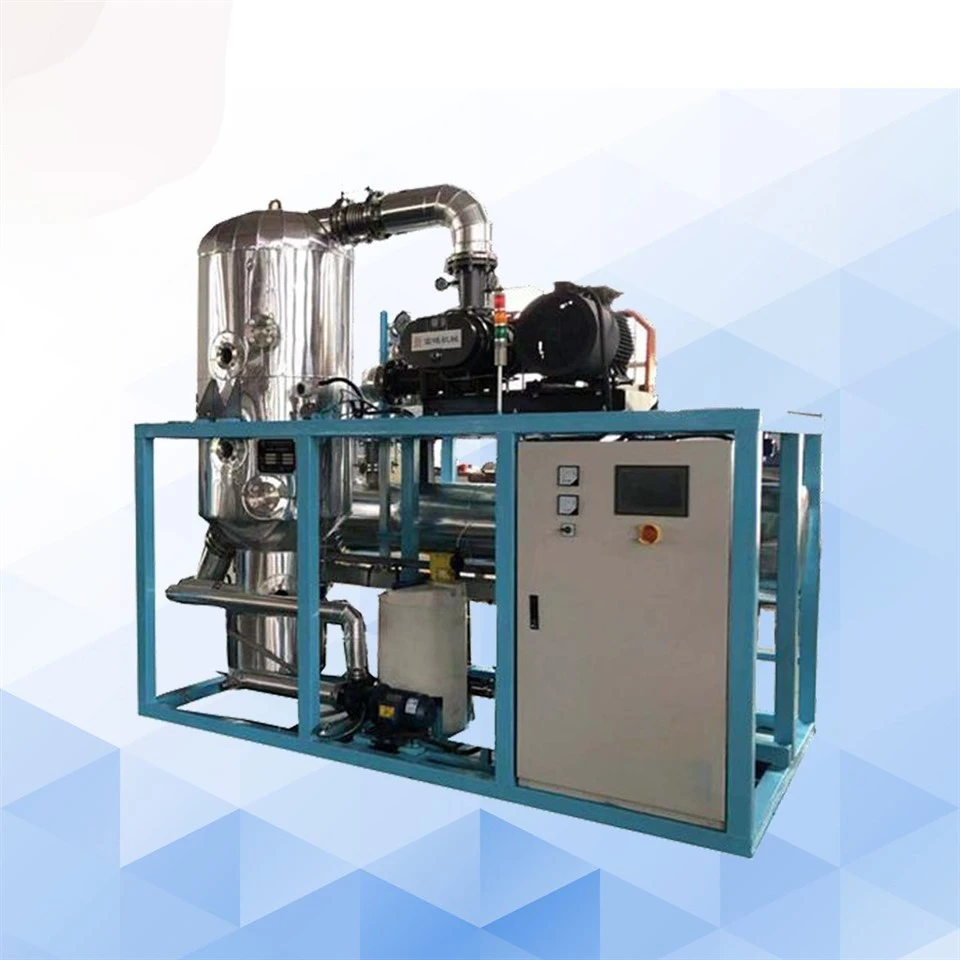
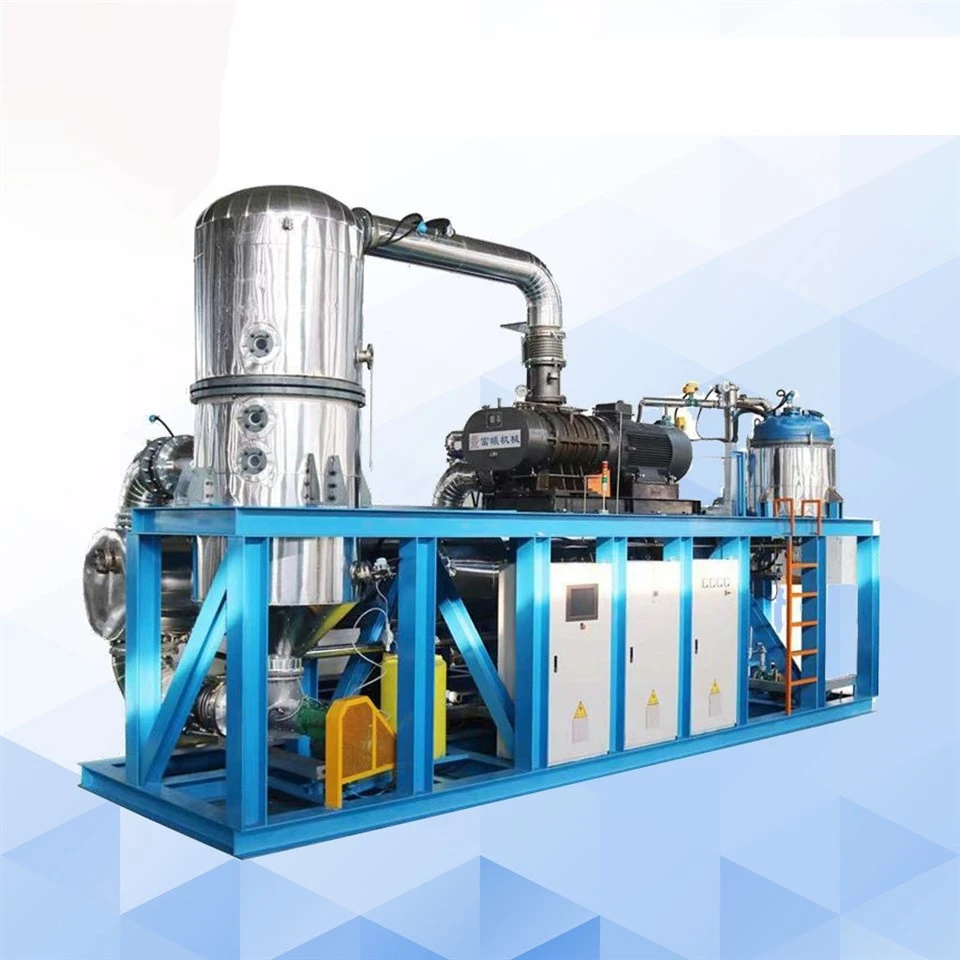
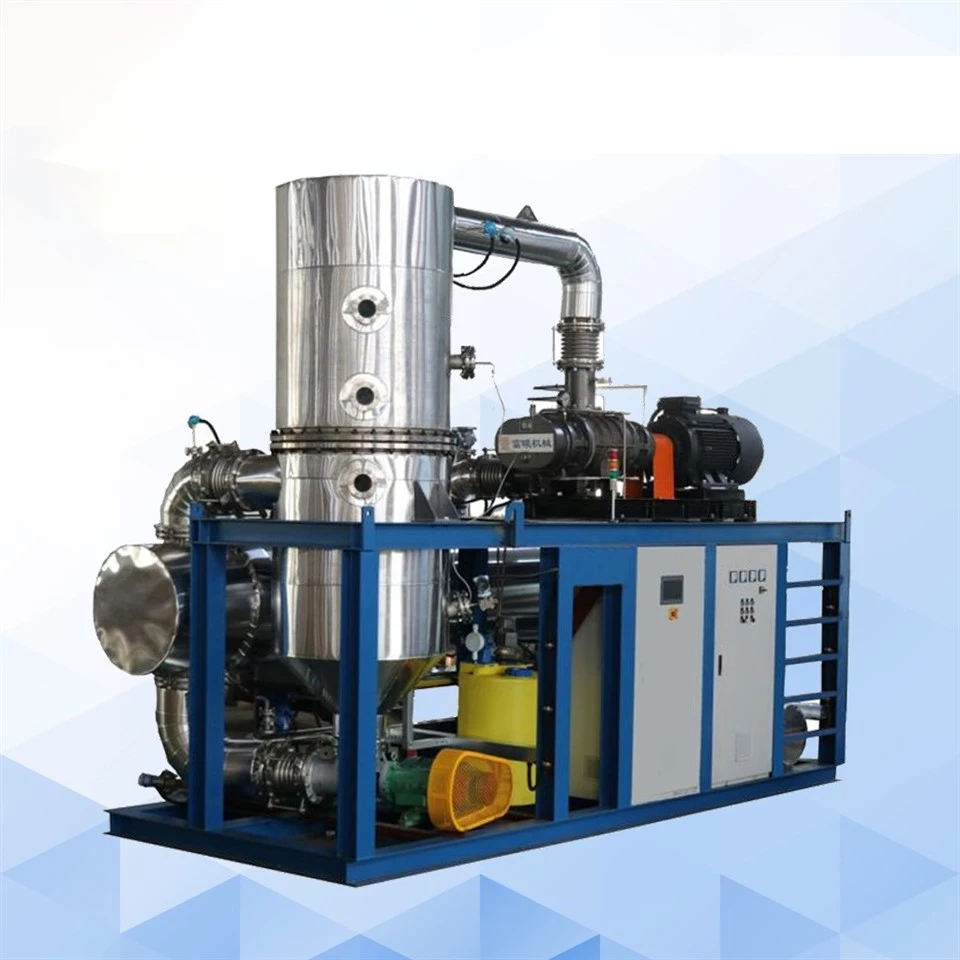
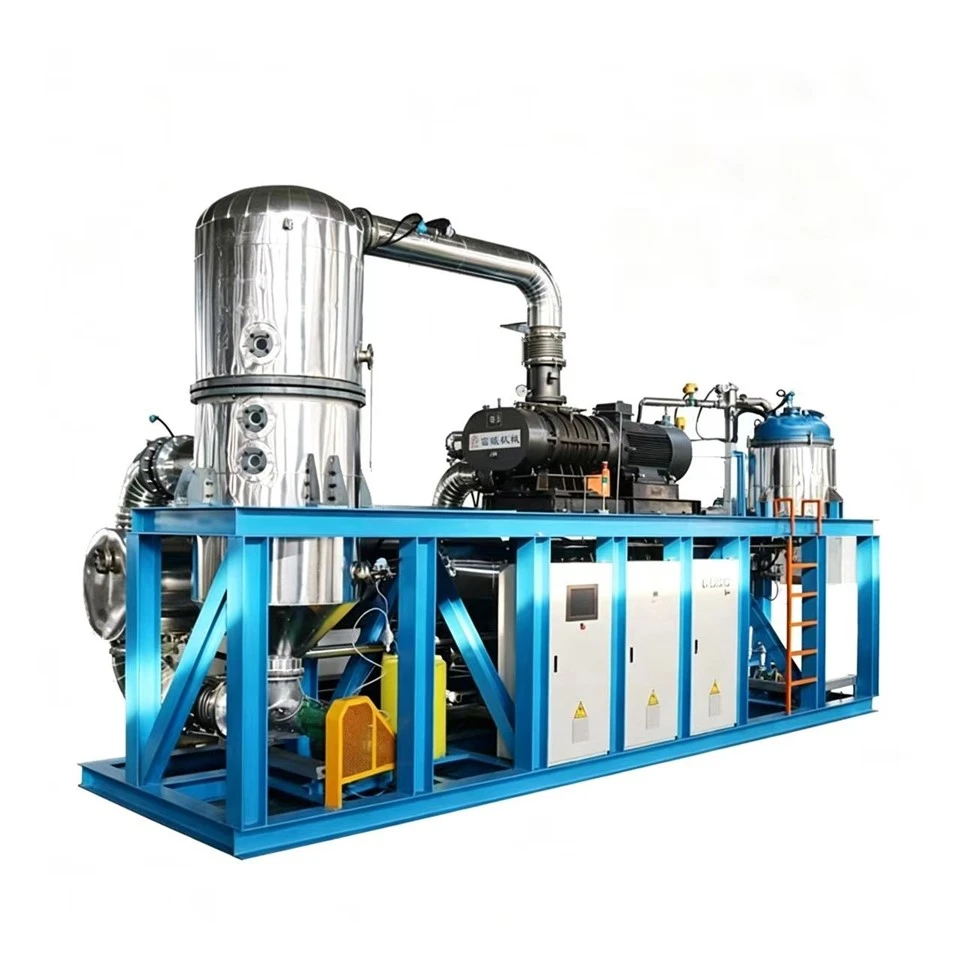
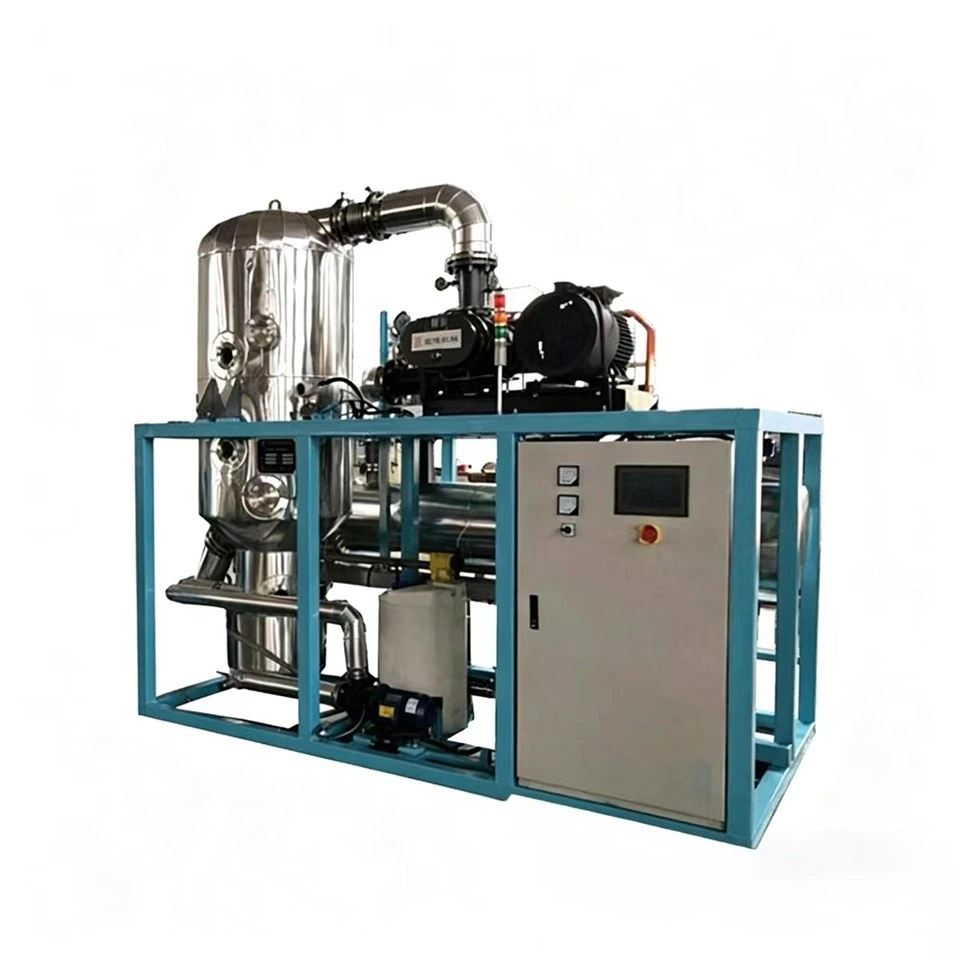
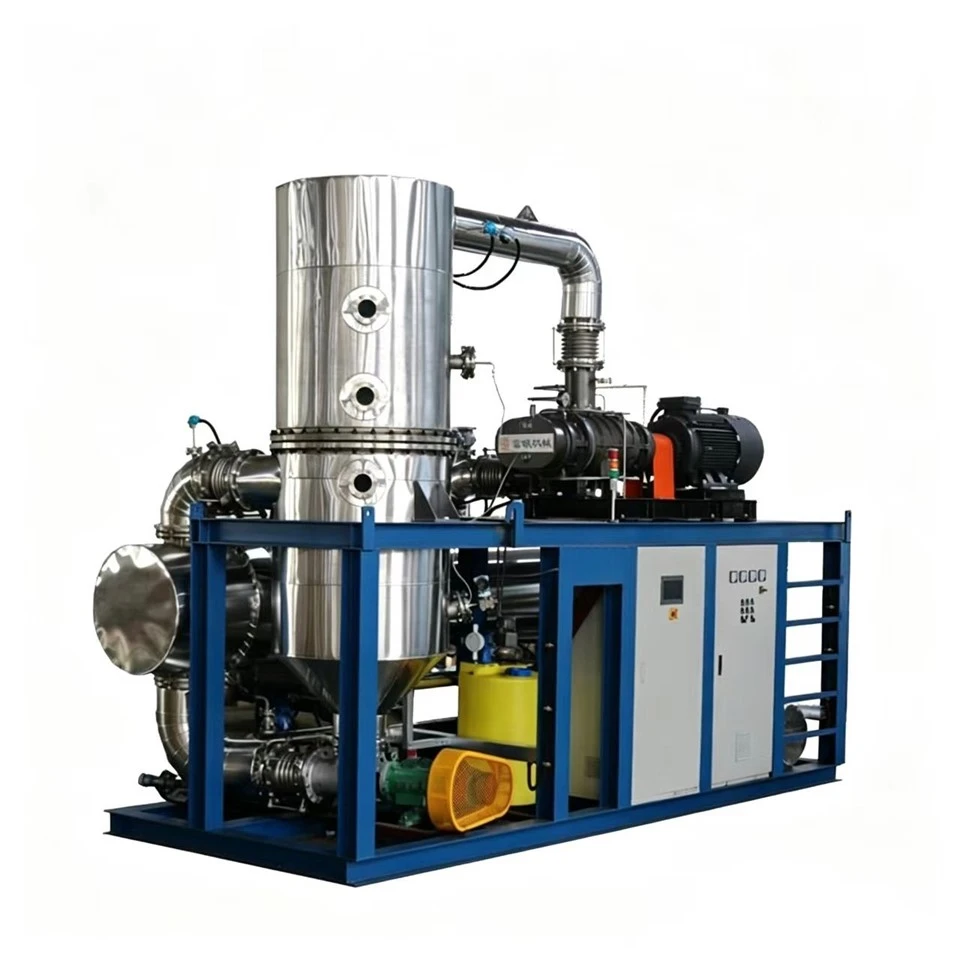
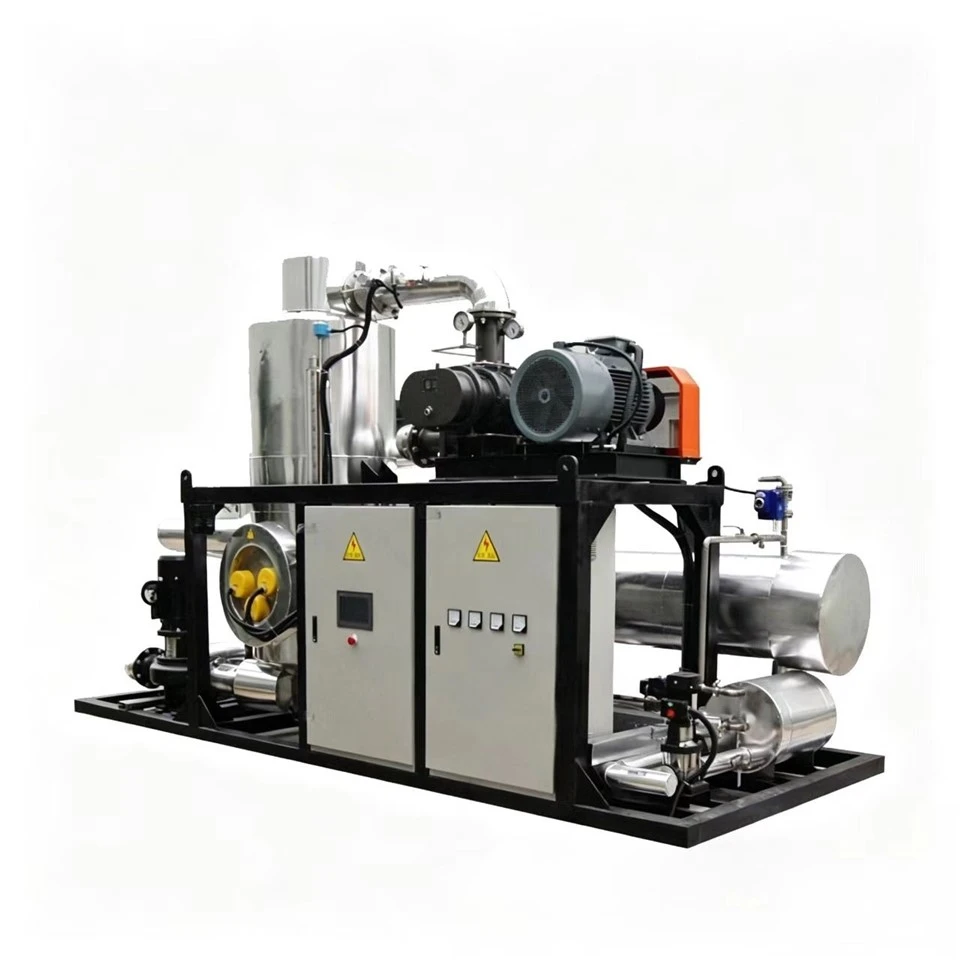
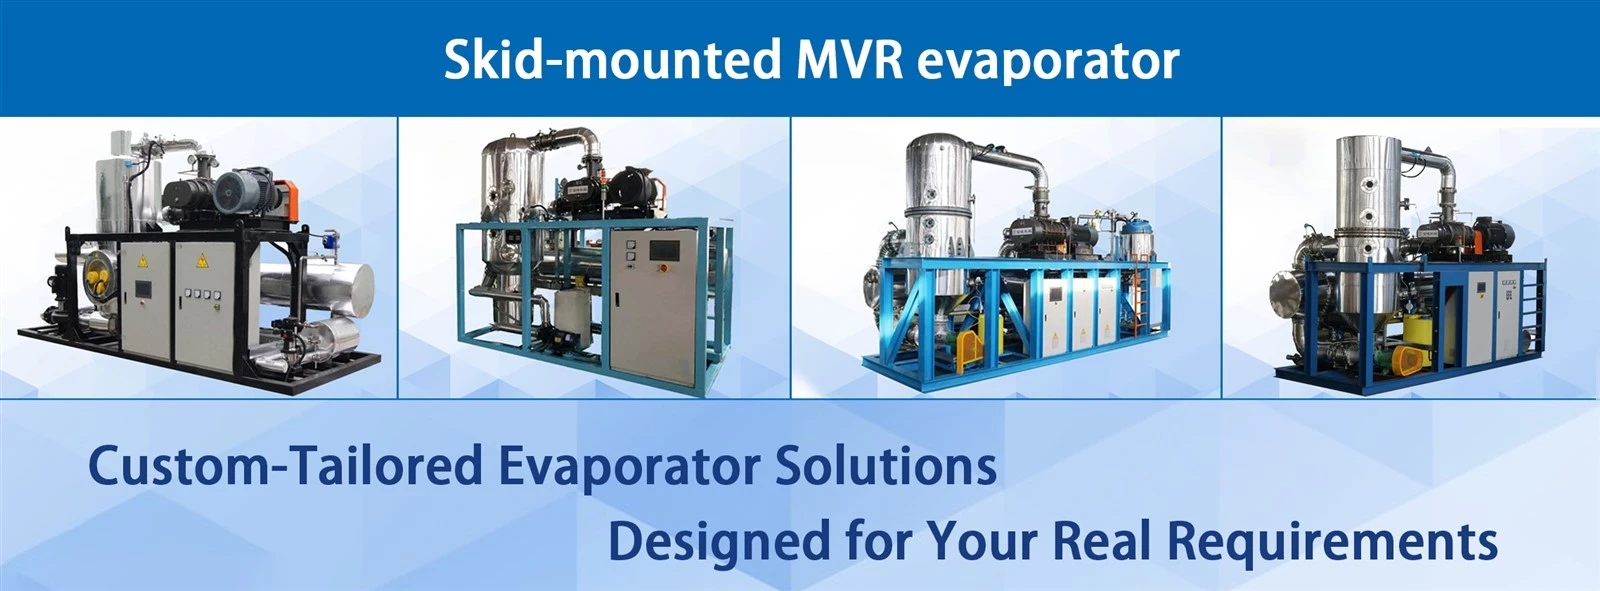
Skid-mounted MVR Evaporator
MVR Evaporator Design
Oslo Evaporation Crystallizer
Multi-effect Evaporator
Double-effect Evaporator
Triple-effect Evaporator
Quadruple-effect Evaporator
Product Keywords
MVR evaporator for salt
MVR evaporator for brine
MVR evaporator for ethanol
MVR evaporator for syrup concentration
Automatic MVR evaporation system
Stainless steel MVR evaporator
Corrosion resistant MVR evaporator
Energy saving MVR evaporator
High efficiency MVR evaporator
Low operating cost MVR evaporator
Product Introduction
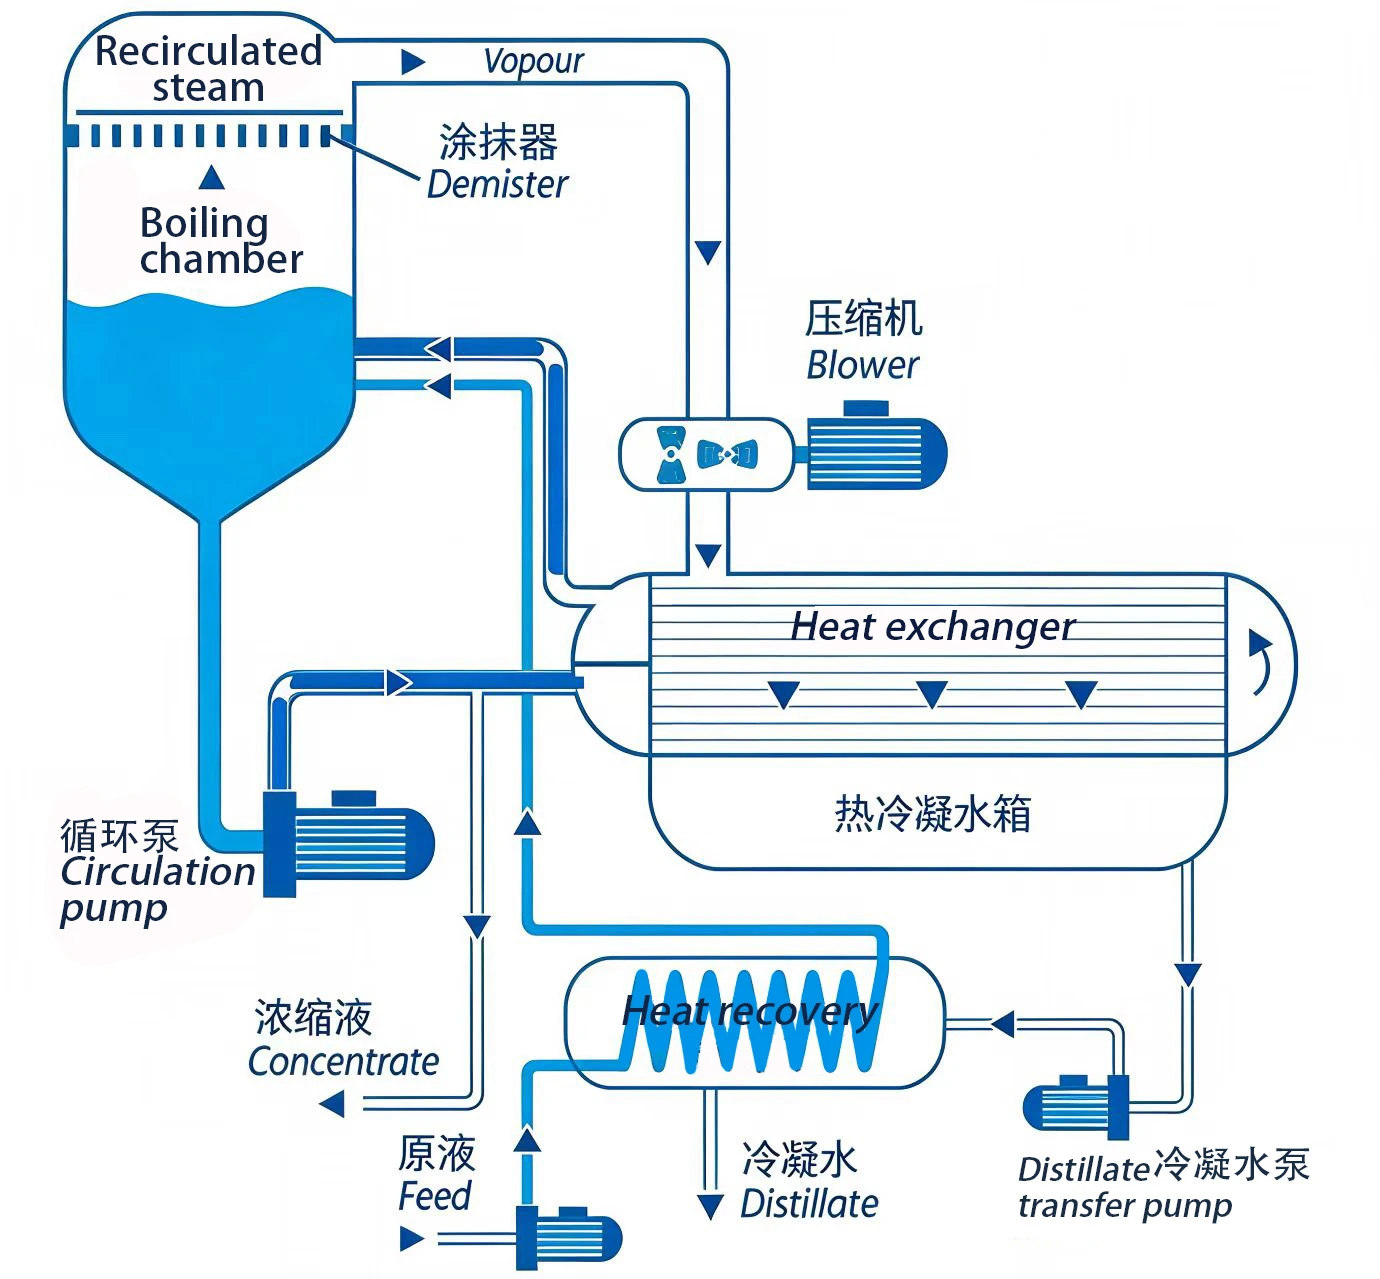
The circulation of the solution inside the evaporator primarily relies on forced flow generated by an external power source. The circulation velocity typically ranges from 1.5 to 3.5 meters per second. This design offers high heat transfer efficiency and production capacity. The feed solution is pumped upward by a circulation pump and flows upward through the tubes in the heating chamber. Upon entering the evaporation chamber, the mixture of steam and liquid droplets separates; the steam is discharged from the top, while the liquid, encountering resistance, falls and is drawn into the circulation pump through the conical bottom, re-entering the heating tubes to continue the circulation.
Advantages of the skid-mounted MVR circulation evaporator
- Energy efficiency;
- High heat transfer coefficient;
- Resistance to salt precipitation and scaling;
- Strong adaptability;
- Ease of cleaning;
- One-click startup, unattended operation.
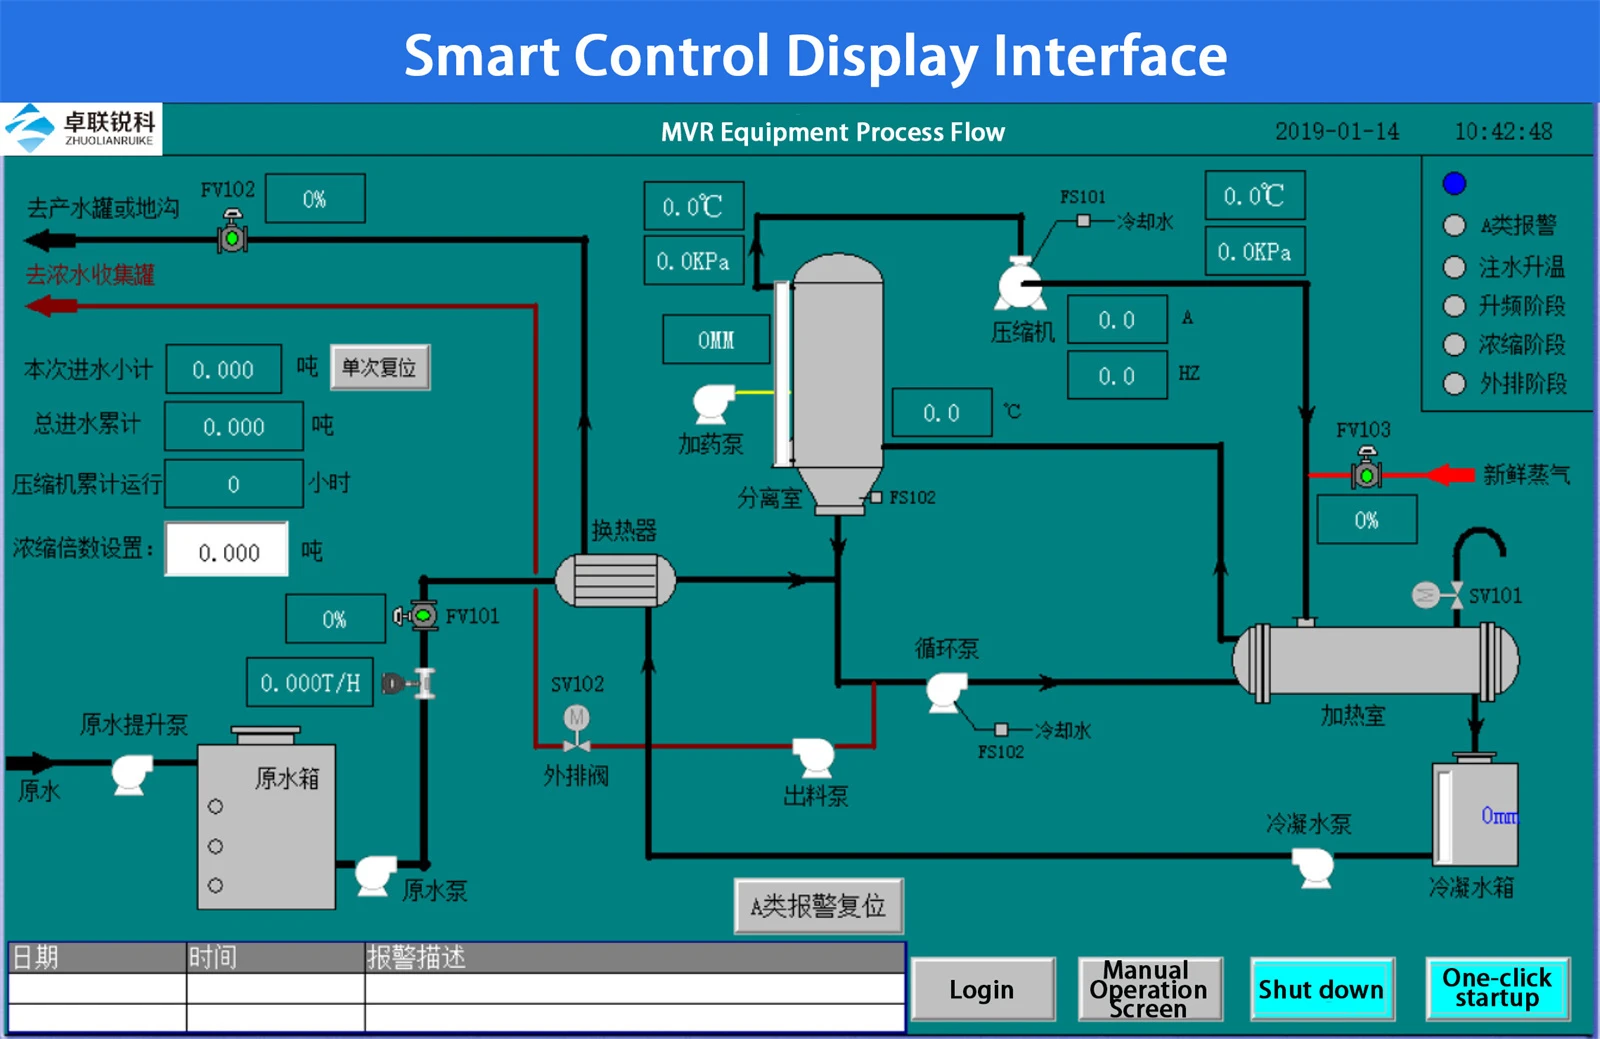
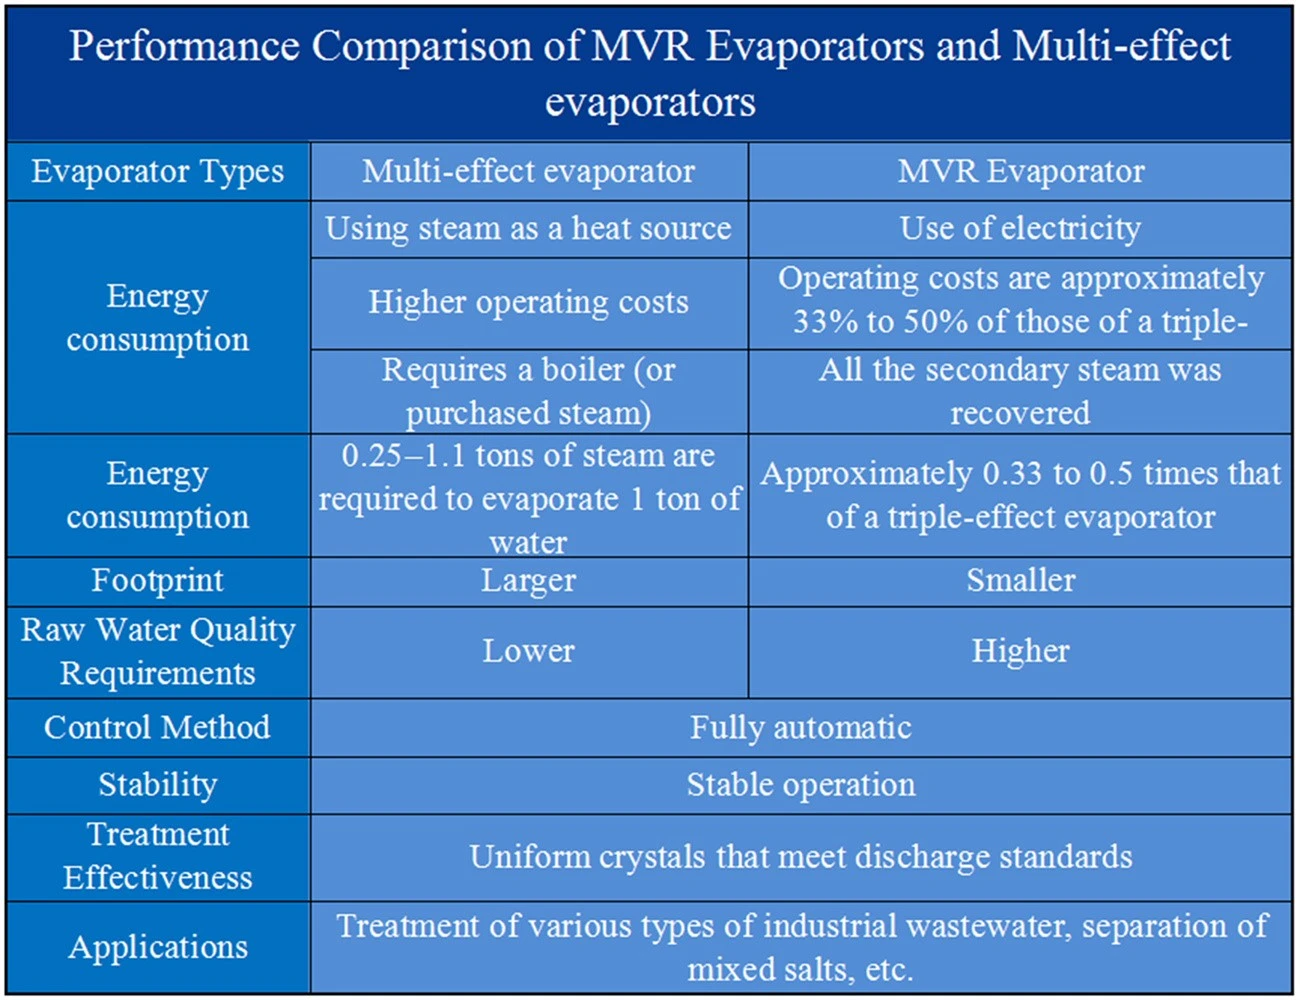
Product Properties:Simple process, resistant to clogging, consumes only 35–40 kWh of electricity to evaporate 1 ton of water, requires minimal floor space, and has low site requirements.
- Automatic MVR evaporation system;
- Stainless steel MVR evaporator;
- Corrosion resistant MVR evaporator;
- Energy saving MVR evaporator;
- High efficiency MVR evaporator;
- Low operating cost MVR evaporator.
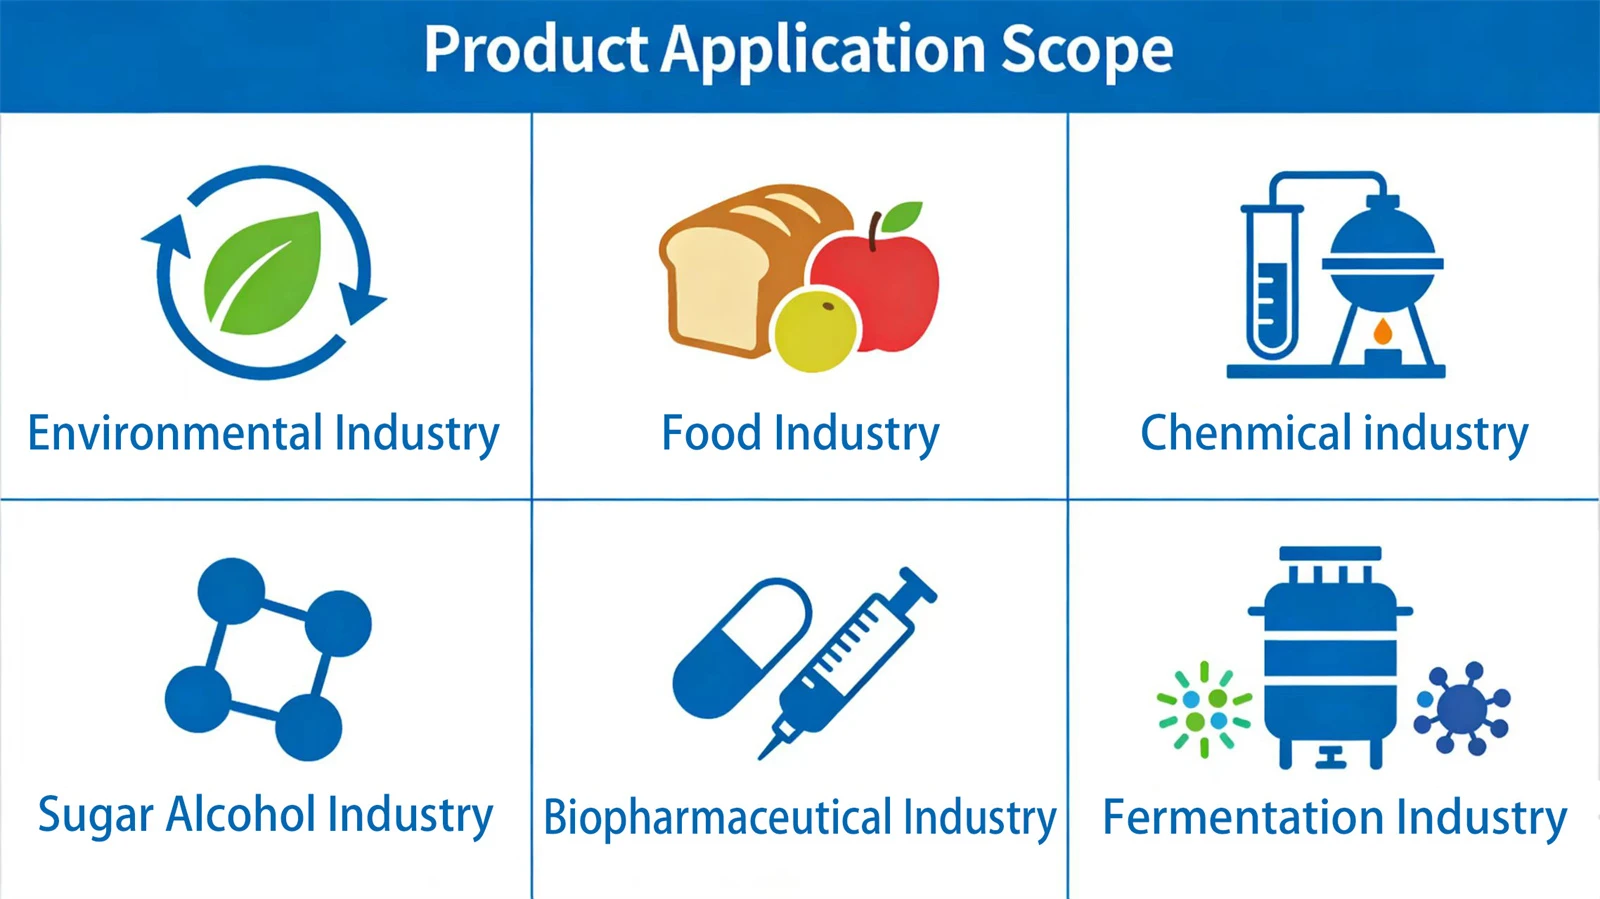
MVR evaporators (Mechanical Vapor Recompression) offer key advantages such as energy efficiency, low-temperature operation, and crystallization capability.
They are suitable for the following applications:
Environmental Protection Industry
Industrial high-salinity wastewater
Wastewater from chemical, coal chemical, electroplating, dyeing, and papermaking industries; concentration and crystallization; near-zero discharge.
Leachate
Concentration and volume reduction; separation of salts and organic matter; reuse of condensate.
Flue gas desulfurization (FGD) wastewater
Wastewater from power plant FGD processes; salt recovery + zero discharge.
Food Industry
Pentose: Addresses issues related to uneven crystal size and excessively low bulk density in the product.
Sugar Alcohol Industry
Mannitol crystallization:addressing issues such as product viscosity, difficulty in centrifugation, and product non-conformity during the customer's production process.
Biopharmaceutical Industry
For example:Oxytetracycline, Kanamycin, Nimocetin, Morpholine hydrochloride, Prednisolone and wastewater treatment for Doxycycline.
Other Common Applications
Lithium-ion Battery Industry:
Lithium recovery, concentration of wastewater from ternary precursor production.
Seawater/Salt Lakes:
Desalination, lithium extraction, salt crystallization.
Metallurgy/Rare Earths:
Heavy metal (nickel, chromium) recovery, salt separation.
Introduction to Key Components
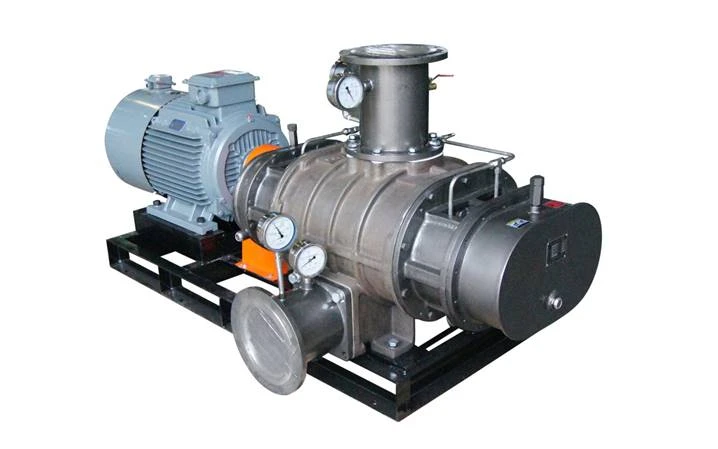
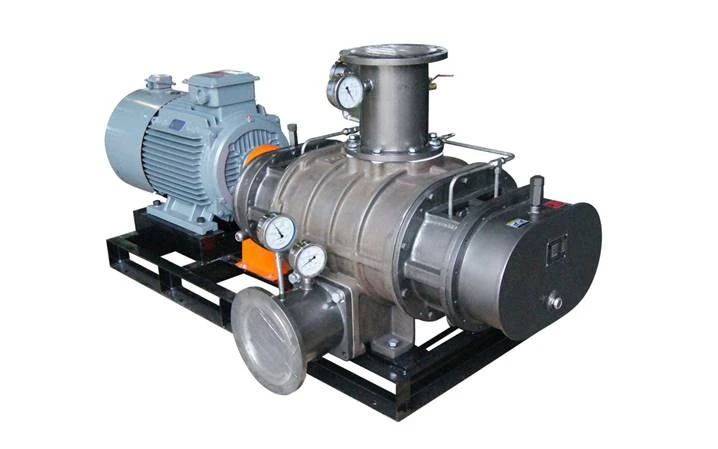
1.Introduction to the Roots Steam Compressor
All flow-through components are made of 2205 duplex stainless steel, offering excellent resistance to cavitation and corrosion.
Precision-fit components such as rotors and chambers are manufactured using CNC machining, ensuring universal interchangeability.
The pressure differential between the inlet and outlet during normal operation exceeds 65 kPa, far surpassing that of products from other manufacturers.
The first to adopt a dual mechanical seal design, featuring mature technology, effective oil-vapor separation, and worry-free operation.
Low operating speed, rugged and durable construction, and resistance to foaming and liquid carryover issues that plague compressor operation.
2.Introduction to the Forced Circulation Pump
A forced circulation pump operates by generating horizontal thrust along the pump shaft through the rotation of the impeller. Its primary function is to enhance equipment production capacity and improve the heat transfer coefficient by facilitating forced circulation.
3.Its advantages are as follows:
- Low rotational speed, generally within 980 RPM, meeting the requirements for stable operation during the crystallization process.
- Excellent hydraulic performance, with 70% of the operating range in the high-efficiency zone, and strong resistance to cavitation.
- The flow direction is vertical inlet and horizontal outlet, minimizing the impact force of the water flow on the impeller and mechanical seal.
- The pump body is integrally cast, ensuring high rigidity.
Company R&D Environment and Capabilities
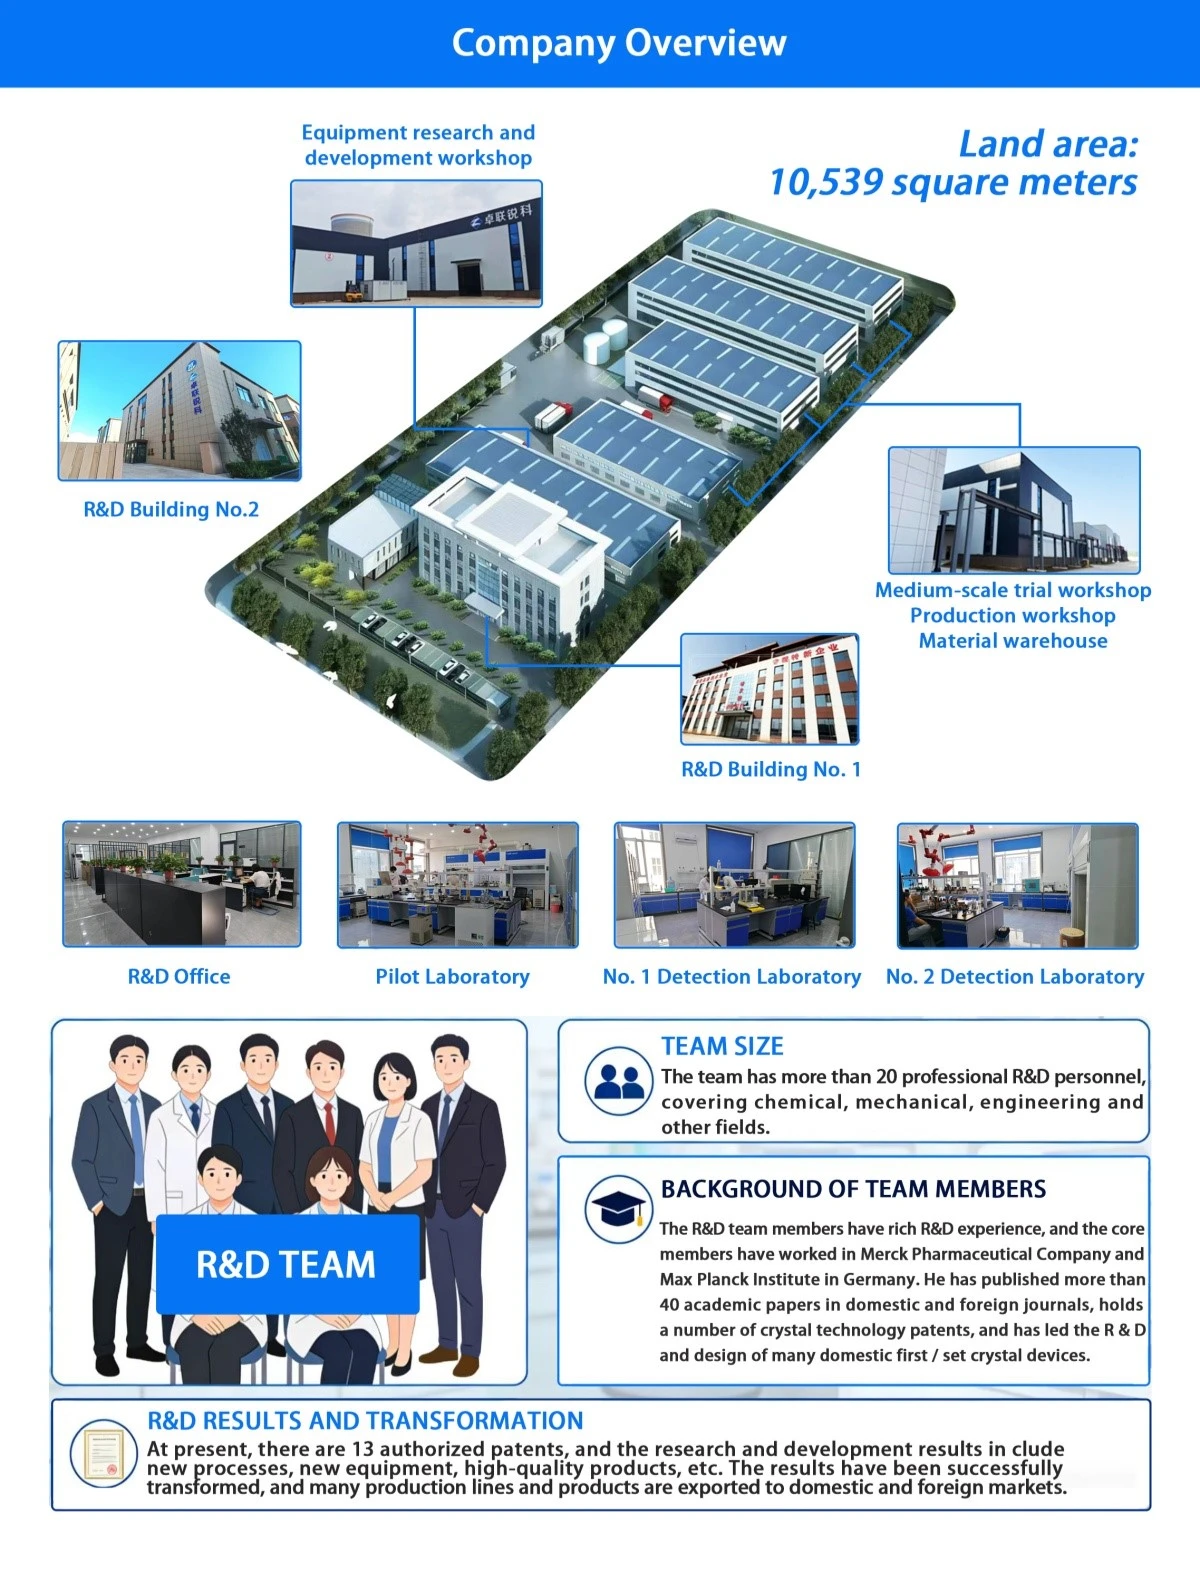
Founded in 2014, Shanxi Zhuolian Ruike Technology Co., Ltd. is a national-level high-tech enterprise and a provincial-level "Specialized, Refined, Unique, and Innovative" enterprise that specializes in crystallization processes and specialized equipment.
With outstanding R&D capabilities, the company operates a 1,100-square-meter independent laboratory, a 15,000-square-meter pilot plant, and a 3,000-square-meter equipment R&D workshop. Its pilot plant, with a total investment of 55 million yuan, has commenced operations, establishing a comprehensive technical system covering the entire process from small-scale trials-pilot-mass production.
The company's products focus on the pharmaceutical, chemical, and food industries, with flagship offerings including DTB crystallizers, continuous crystallization units for tetramethylpiperidine, MVR evaporators for sodium acetate trihydrate, and production units for molten-salt-grade nitrates.
In terms of equipment, the company is equipped with high-precision R&D and production machinery and offers customized design and manufacturing services. With annual revenue of 50 million yuan, technical services and high-end equipment account for over 60% of its business, filling a technological gap within the province and establishing a differentiated competitive advantage nationwide.
Company R&D Capabilities
We have a team of over 20 professional R&D personnel spanning multiple fields, including chemistry and engineering.
Team members possess extensive R&D experience; key members have previously worked at Merck & Co. in the U.S. and the Max Planck Society in Germany. They have published more than 40 academic papers in domestic and international journals, hold multiple patents for crystallization technologies, and have led the R&D and design of numerous crystallization units that were the first of their kind in China.
We operate state-of-the-art laboratories and pilot-scale R&D facilities equipped with advanced experimental equipment and instruments, providing robust support for our R&D efforts.
At present, We hold 13 authorized patents and have developed new processes, new equipment, and high-quality products.
Our R&D achievements have been successfully commercialized into multiple production lines, with products sold both domestically and internationally.
QA&QC
Q: Is customization available?
A: Yes
Q: Can you provide spare parts and remote support as needed?
A: Yes
Q: Can you provide photos or videos of the production process?
A: Yes
Q: Does the user interface support English and local languages?
A: Yes
Hot Tags: skid-mounted mvr evaporator, China skid-mounted mvr evaporator manufacturers, suppliers, factory


