
Learn About Magnesium Sulfate-Functions and Uses of Magnesium Sulfate
Physical and Chemical Properties of Magnesium Sulfate
Magnesium sulfate (MgSO₄) has a wide range of applications and is commonly used in medicine, obstetrics, agriculture, and industry, though its functions vary greatly. I'll explain them clearly for you.
Basic Appearance: Industrial magnesium sulfate is presented as colorless transparent monoclinic crystals or white fine crystalline powder. Common commercial specifications include heptahydrate, monohydrate and anhydrous types. After our precise crystallization and purification treatment, the product features smooth crystal surface, uniform particle distribution and high finished product cleanliness without impure spots.
Solubility Characteristics: Magnesium sulfate has moderate water solubility with obvious temperature sensitivity, showing a unique solubility curve different from other inorganic salts. It is slightly soluble in glycerol but insoluble in ethanol and most organic solvents. The neutral aqueous solution provides mild and stable reaction conditions for industrial purification and crystallization separation.
Stability & Hygroscopicity: The product boasts excellent chemical stability under normal temperature and pressure environments. Heptahydrate magnesium sulfate is prone to weathering and losing crystal water in dry air, while anhydrous products have weak hygroscopicity and outstanding storage stability, adapting to long-term transportation and long-cycle stockpiling requirements.
Thermal Decomposition Performance: Magnesium sulfate undergoes staged dehydration with temperature rise. It loses most crystal water below 200℃ and completely converts into anhydrous powder. Thermal decomposition occurs above 1124℃ to generate magnesium oxide and sulfur trioxide, with a wide safe temperature range for industrial dehydration and drying.
Product Index Advantages: Our customized magnesium sulfate products feature low impurity residue, stable pH value and controllable crystal water content. We can adjust bulk density and particle fineness to meet food grade, agricultural grade, industrial grade and pharmaceutical auxiliary grade standards.
Core Industrial Application Scenarios
Agricultural Planting Industry
As a high-quality magnesium and sulfur supplementary fertilizer, magnesium sulfate is widely used for soil improvement and crop nutrient supplementation. It effectively alleviates leaf yellowing and growth retardation caused by magnesium deficiency, promotes chlorophyll synthesis and crop metabolism, and is suitable for grain crops, cash crops and horticultural planting.
01
Food & Pharmaceutical Industry
High-purity food-grade magnesium sulfate serves as a food additive and quality improver, while pharmaceutical-grade products are used for pharmaceutical intermediates and medical auxiliary preparations, strictly complying with international food safety and pharmaceutical production standards.
02
Building & Material Industry
It acts as an excellent cement coagulant, flame retardant and building material additive. It can optimize the solidification performance of building materials, enhance structural compactness and fire resistance, and is widely used in lightweight building materials and fireproof material processing.
03
Chemical & New Material Industry
Used as a core raw material for synthesizing magnesium oxide, magnesium hydroxide and other magnesium-based fine chemicals, as well as a raw material for new environmental protection materials and battery auxiliary materials, with stable chemical activity and high synthesis matching degree.
04
Daily Chemical & Aquaculture Industry
Applied in the production of cosmetics and daily chemical additives to adjust product viscosity and stability. It also serves as water quality regulator and nutrient supplement in aquaculture to optimize aquatic growth environment.
05
Our Professional Magnesium Salt R&D Experience
Our team has long been dedicated to the technical research and industrial transformation of magnesium-series inorganic salts, forming an independent and mature technical system for magnesium sulfate crystallization, dehydration and purification, with technical routes completely different from sulfate and nitrate products of other metal ions.
We have undertaken numerous magnesium sulfate process upgrading and customized production projects, accumulating rich practical experience in raw material impurity separation, staged dehydration control, crystal morphology optimization and mother liquor resource recycling.
Aiming at industry pain points such as inconsistent crystal water content, low product purity, poor particle uniformity and low resource utilization rate in traditional production, we have developed targeted innovative processes to break through existing technical limitations and improve product comprehensive quality.
We have established a complete magnesium salt technical iteration mechanism, continuously optimizing process parameters to adapt to international high-standard product requirements and green environmental protection production specifications.
Standard Magnesium Sulfate R&D and Industrial Process
Raw Material Detection & Customized Scheme
Conduct full-component analysis of raw materials, detect soluble impurities, insoluble substances and metal ion content, combine client's target product grade and application scenarios, and formulate exclusive purification and staged crystallization schemes.
Laboratory Process Optimization
Optimize core parameters including solution concentration, constant temperature crystallization time, staged cooling rate and dehydration temperature gradient, screen efficient impurity removal processes, and precisely control crystal water content and particle growth state.
Pilot Scale-Up Verification
Carry out continuous pilot test simulation of industrial production, verify process stability, product index consistency and waste liquid recycling efficiency, eliminate scale-up effect risks, and optimize process parameters for mass production.
Industrial Process Landing & Commissioning
Formulate standardized industrial continuous production processes, output complete process technical packages, and provide one-stop services including supporting equipment selection, production line installation guidance, on-site commissioning and long-term production parameter optimization.
R&D Facilities and Site Strength
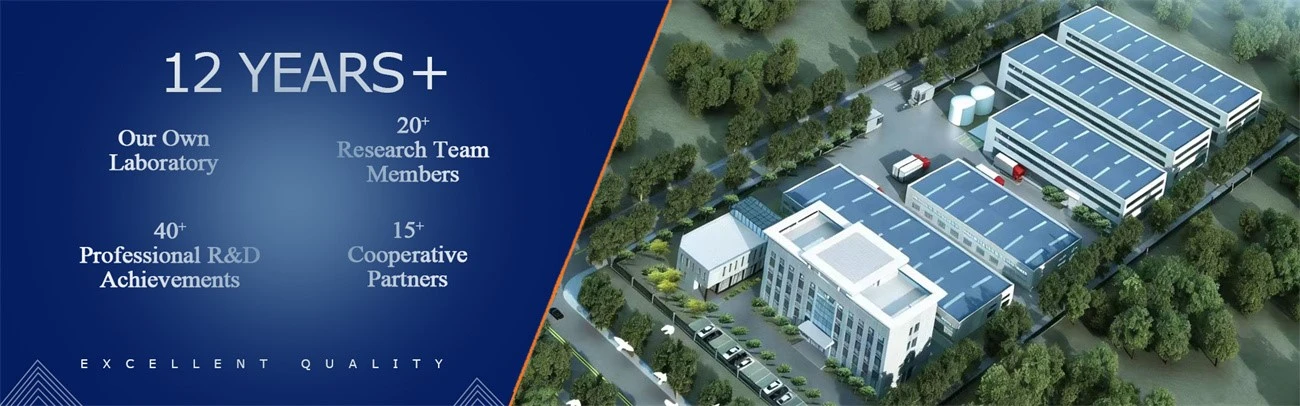
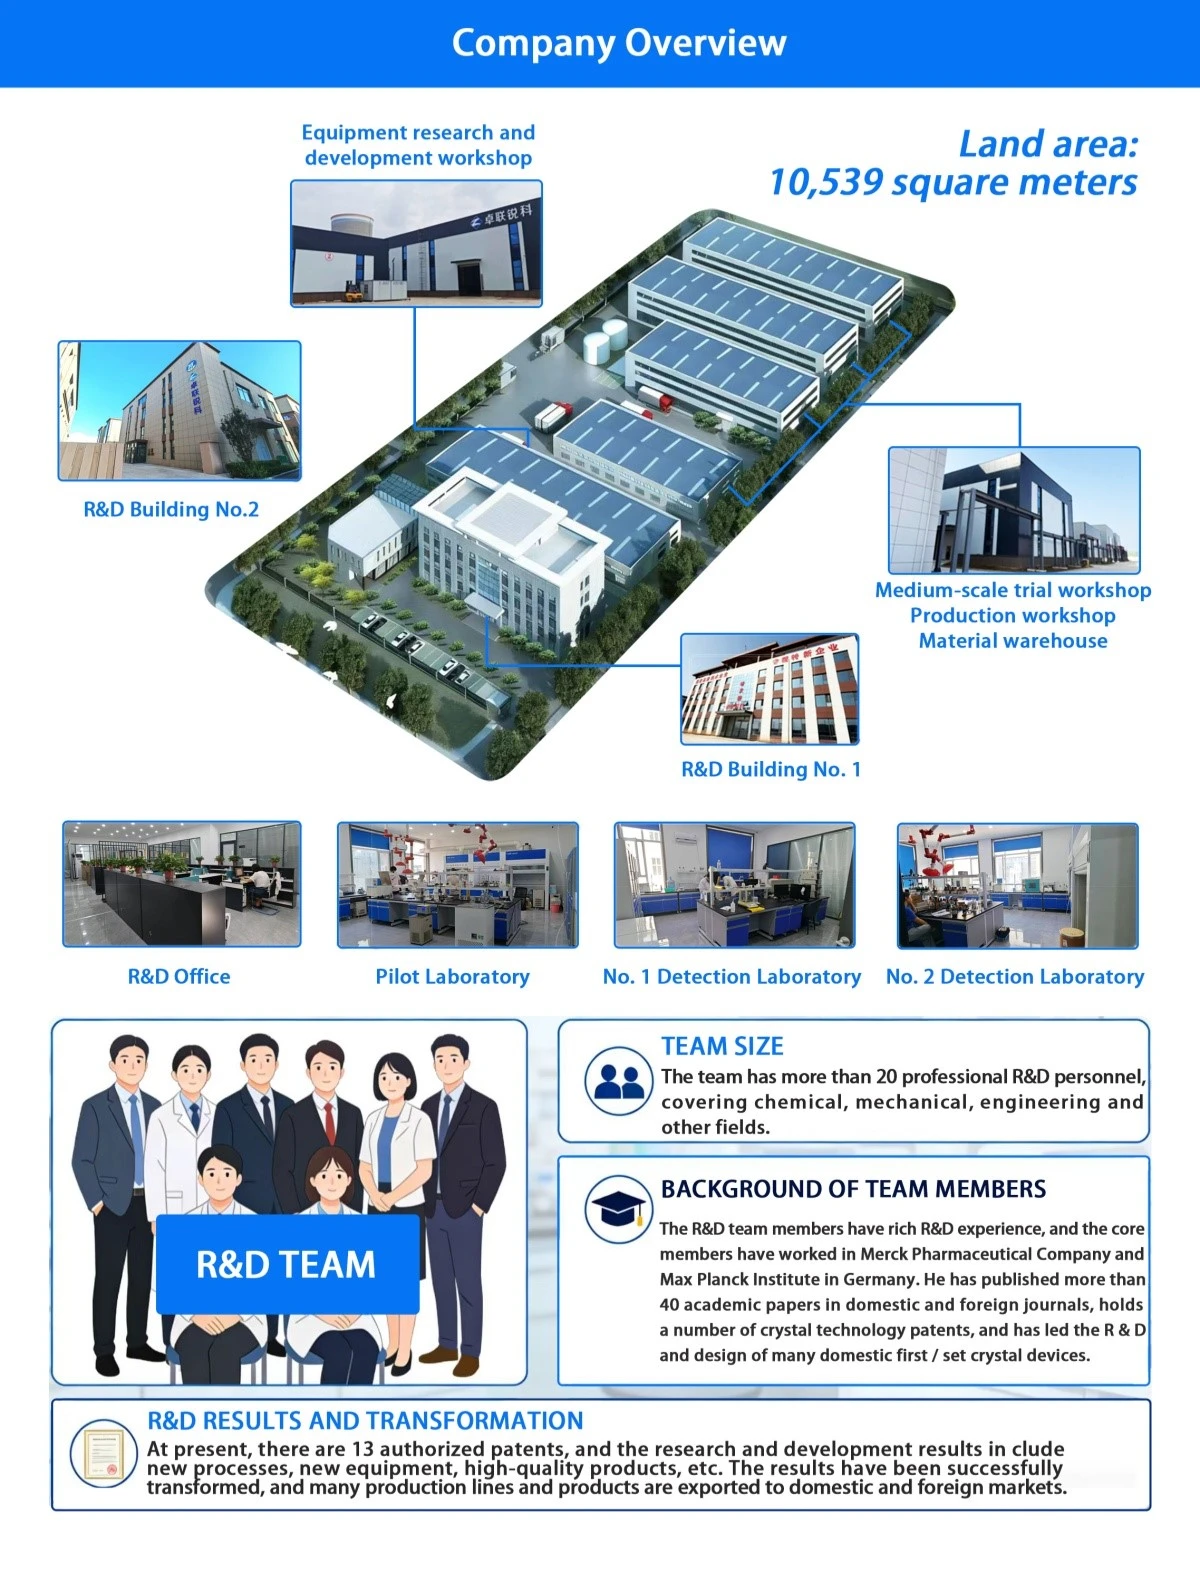
We are equipped with a professional magnesium salt dedicated R&D laboratory and independent pilot test base, equipped with staged dehydration equipment, constant-temperature crystallization systems and closed-loop mother liquor treatment devices customized for magnesium sulfate production characteristics.
The laboratory is equipped with high-precision professional testing instruments such as crystal water detectors, particle size distribution analyzers and trace impurity testers, realizing full-index accurate detection and quality control of finished magnesium sulfate products.
All R&D experiments and pilot tests adopt international industrial standard parameters, which can truly simulate the temperature, pressure and material circulation environment of large-scale factories, ensuring high consistency between experimental data and actual industrial production results.
The standardized laboratory implements partition management for raw material pretreatment, crystallization test, precision detection and sealed sample storage, effectively avoiding product weathering, secondary pollution and quality fluctuation, ensuring reliable and repeatable R&D results.
Product and Technical Core Advantages
Precise Index Control & High Purity: Adopting staged purification and targeted impurity removal technology, our magnesium sulfate products have extremely low trace impurity content. The crystal water content is precisely controlled, stably meeting food, pharmaceutical, agricultural and high-end industrial grade standards.
Optimized Crystal Morphology: Through graded cooling crystallization and flow field regulation technology, the finished product has uniform particle size, high bulk density and good fluidity, effectively solving the problems of fine powder excess and easy agglomeration of traditional products.
Green Production & High Yield: The optimized closed-loop circulation process realizes efficient recycling of mother liquor and waste water, greatly improves raw material utilization rate, reduces energy consumption and waste discharge, and achieves eco-friendly and high-efficiency production.
Complete Supporting Technology & Equipment: We provide customized special production equipment and complete set of mature process packages for magnesium sulfate, realizing integrated output of core technology and supporting equipment to meet clients' personalized production needs.
Full-Process Industrial Support: We provide comprehensive technical services from process design and equipment debugging to later production optimization and technical training, helping clients quickly realize stable large-scale production and market expansion, and enhance core market competitiveness.
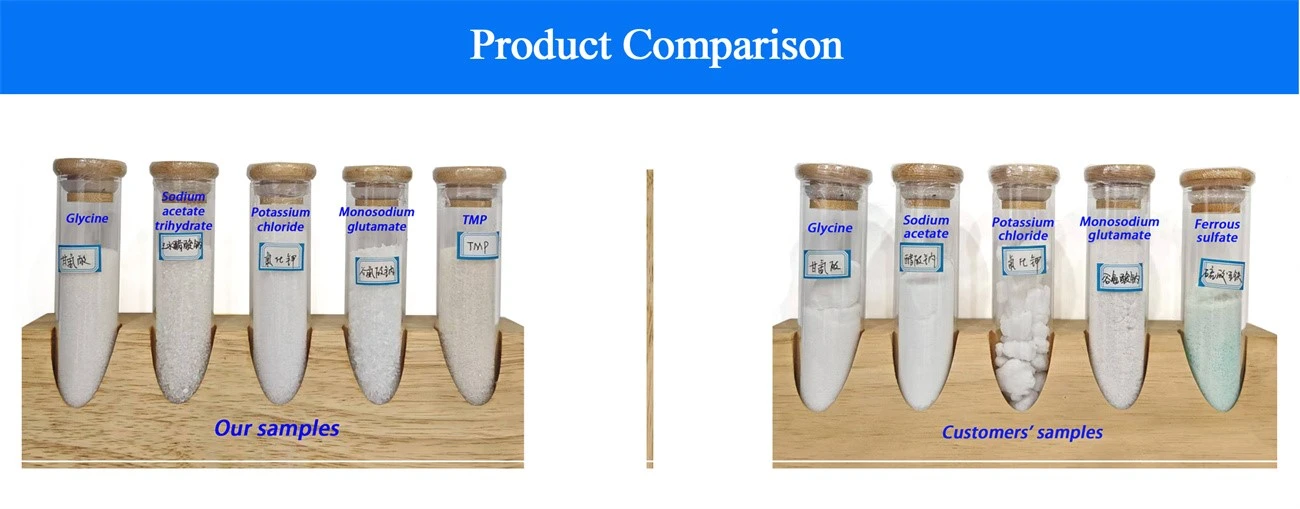
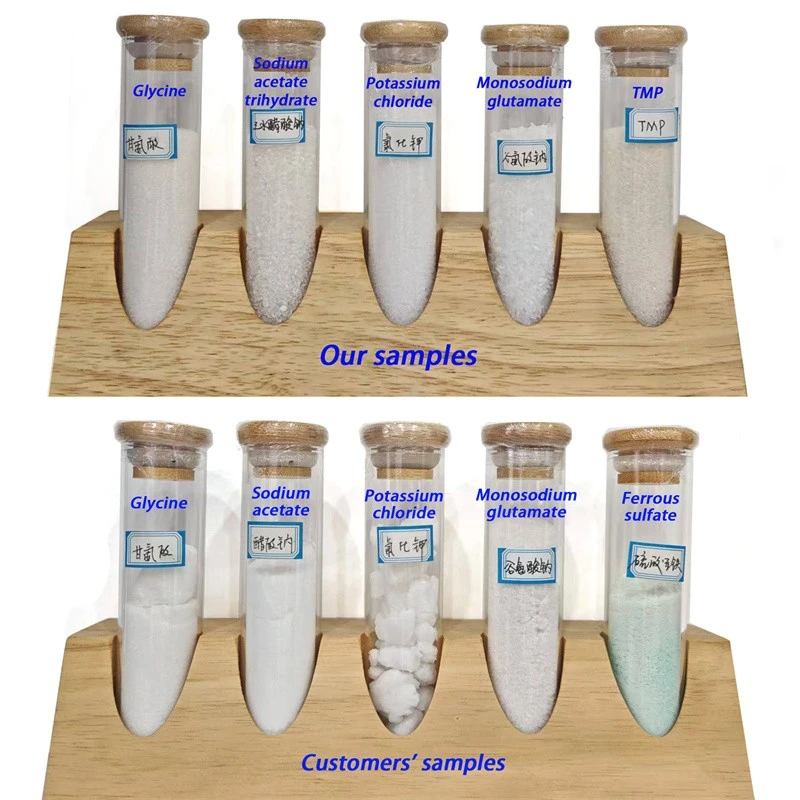
|
OUR SAMPLES |
CUSTOMERS' SAMPLES |
|
No caking |
Severe caking |
|
Large crystalline particles |
Small particles |
|
Uniform granules |
Uneven particle size |
|
Easy to transport and store |
Not suitable for transport or storage |
Related Keywords
Magnesium Sulfate process; Magnesium Sulfate technology; Magnesium Sulfate rd
ZLRK specializes in customized process R&D, technical optimization and industrial scale-up services for magnesium sulfate and magnesium-based inorganic salt products. With years of experience in inorganic salt crystallization engineering, we have built a unique technical system tailored for magnesium sulfate, which is completely different from nitrate crystallization, zinc sulfate and potassium sulfate production processes.
We target the typical industrial pain points of traditional magnesium sulfate production, including uncontrollable crystal water content, low finished product bulk density, excessive soluble impurities, unstable product grade and high residual mother liquor loss. Our team focuses on low-cost purification, precise crystallization control and green production process innovation to solve core industry technical bottlenecks.
We provide full-cycle one-stop industrial services covering laboratory formula debugging, impurity removal process optimization, pilot scale-up verification, customized process package output and complete supporting equipment integration. We support R&D and mass production of monohydrate, heptahydrate and anhydrous magnesium sulfate, helping global clients achieve standardized large-scale production and high-efficiency market promotion.
Hot Tags: magnesium sulfate process research and development, China magnesium sulfate process research and development manufacturers, suppliers, factory


