
Learn About Sodium Sulfate-Functions and Uses of Magnesium Sulfate
Physical and Chemical Properties of Sodium Sulfate
Sodium sulfate (Na₂SO₄) is primarily used in the pharmaceutical, industrial, light industrial, textile, and glass sectors.
Basic Appearance: Industrial sodium sulfate, also known as thenardite or anhydrous salt cake, appears as colorless transparent orthorhombic crystals or uniform white crystalline powder. Decahydrate sodium sulfate presents granular crystal form at room temperature. After our refined crystallization treatment, the product features clean surface, uniform granularity and no impurity spots, meeting international commercial grade standards.
Solubility Traits: Sodium sulfate exhibits unique temperature-dependent solubility, with rapid solubility rise within low-temperature range and gradual saturation in high-temperature environments. It is soluble in water and glycerol, and completely insoluble in ethanol and organic solvents, forming the core physical basis for our low-energy evaporation and selective crystallization technology.
Stability & Hygroscopicity: The product features excellent chemical inertness and room-temperature stability, with no oxidation or decomposition reaction under conventional storage conditions. Anhydrous sodium sulfate has extremely low hygroscopicity, while decahydrate products easily weather and lose crystal water in dry air, enabling flexible grading and customized production for diverse scenarios.
Thermal Characteristics: Sodium sulfate has a melting point of 884℃ and maintains stable chemical structure under conventional industrial heating temperatures. It features gentle dehydration transition and no harmful gas decomposition during processing, with safe and controllable industrial production conditions.
Product Grading Features: Our customized sodium sulfate products achieve stable purity grading, low water-insoluble content and controllable bulk density. We can adjust powder and particle proportion to adapt to detergent, papermaking, chemical synthesis and pharmaceutical auxiliary industrial standards.
Core Industrial Application Scenarios
Detergent & Daily Chemical Industry
As a key filler and diluent for synthetic detergents, sodium sulfate improves detergent powder fluidity and anti-caking performance, enhancing product stability and washing effect. It is widely applied in large-scale daily chemical formulation and mass production.
01
Paper & Pulp Industry
Serves as an essential auxiliary agent in kraft pulp manufacturing, promoting fiber swelling and delignification, improving pulp yield and paper texture uniformity. It is a stable and low-cost core raw material for modern paper industry.
02
Textile & Dyeing Industry
Used as a dyeing auxiliary and levelling agent for cotton and chemical fiber fabrics, it optimizes dye adsorption uniformity, reduces color difference and improves dyeing rate, widely used in industrial textile printing and dyeing processing.
03
Chemical & Pharmaceutical Industry
Acts as a fundamental raw material for synthesizing sodium silicate, sodium sulfide and other fine chemicals. High-purity grades can be used for pharmaceutical intermediates and laboratory chemical reagents, ensuring high reaction stability.
04
Building & New Material Industry
Applied in glass manufacturing, ceramic firing and cement additives, playing a role in clarifying, fluxing and strengthening material compactness, improving finished product surface finish and structural durability.
05
Mature Sodium Sulfate R&D & Industrial Experience
Our company has long focused on process optimization and industrial transformation of sodium sulfate products, accumulating extremely mature technical experience covering natural mineral extraction, synthetic purification and waste liquid recycling processes, forming a stable and replicable technical system.
We have completed multiple large-scale sodium sulfate production line upgrading and technical renovation projects, proficient in solving industry common problems such as high evaporation energy consumption, uneven crystal particle distribution, unqualified soluble impurities and low finished product qualification rate.
Different from lab-only theoretical research, our technical team focuses on industrial practicability and market landing. All optimized processes have been fully verified in actual production, with stable process parameters and strong anti-interference ability, suitable for long-term continuous factory production.
We have rich experience in product grade customization and market adaptation, capable of adjusting production schemes according to regional environmental protection standards and downstream customer demands, helping clients quickly match market access requirements and accelerate product promotion.
Standardized Sodium Sulfate R&D & Production Process
Raw Material Analysis & Scheme Formulation
Conduct full-index detection of raw ores, brine or synthetic raw materials, analyze impurity components and water quality indicators, combine client's production scale and target product grade, and formulate targeted low-energy crystallization and purification schemes.
Laboratory Optimization & Parameter Screening
Optimize core parameters including evaporation concentration ratio, cooling crystallization gradient, seed crystal addition and impurity removal sequencing, eliminate process defects, and improve product purity and particle uniformity.
Pilot Scale-Up & Stability Verification
Simulate factory continuous production conditions for batch pilot tests, verify process stability, energy consumption level and product consistency, eliminate scale-up risks, and lock mature industrial production parameters.
Industrial Landing & Production Guidance
Output standardized and operable full-set process packages, support complete equipment docking and production line commissioning, provide long-term production parameter optimization guidance to ensure stable and efficient mass production.
R&D Facilities and Industrial Site Advantages
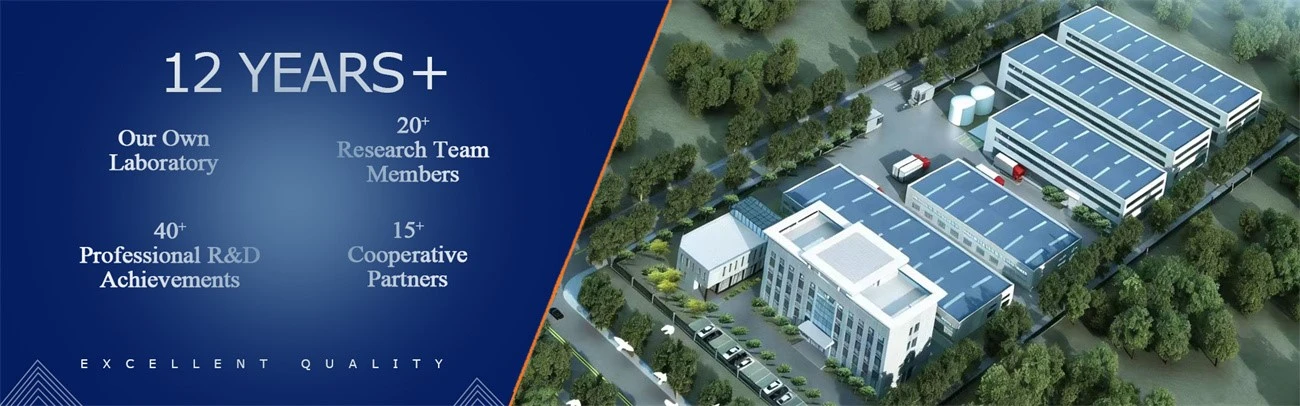
We are equipped with a professional sodium sulfate process R&D laboratory and independent pilot test workshop, with dedicated evaporation concentration systems, gradient crystallization equipment and low-energy drying devices tailored for sodium sulfate production characteristics.
The laboratory is equipped with high-precision particle size analyzers, purity detectors and moisture testing instruments, realizing full-coverage accurate detection of finished product indexes and ensuring strict quality control standards.
All R&D and pilot tests adopt industrial standard operating parameters, which can highly restore the actual operating environment of large-scale production lines, ensuring that experimental results are directly adaptable to factory mass production.
The standardized site implements partition management for raw material processing, crystallization test, finished product detection and sample storage, avoiding cross-contamination and quality fluctuation, providing reliable hardware support for process maturity verification.
Product & Technical Core Advantages & Landing Support
Mature & Stable Process: Our sodium sulfate production technology has been fully industrially verified, with simple operation, strong process stability and low failure rate, completely avoiding the instability problems of new immature processes.
High Purity & Uniform Quality: Adopting graded purification and precise crystallization control technology, finished products feature low impurity, uniform particle size and stable grading, fully meeting the strict quality requirements of downstream high-end industries.
Energy-Saving & Cost-Effective: The optimized low-energy evaporation and closed circulation process effectively reduces production energy consumption and waste discharge, improves raw material utilization rate, and creates obvious cost advantages for clients' market competition.
Full-Set Equipment & Process Support: We provide matched customized production equipment and complete mature process packages, realizing one-stop integration of technology and equipment, reducing clients' independent R&D and transformation costs.
Strong Industrial Landing & Promotion Ability: Focusing on technical achievement transformation, we provide full-cycle services from process debugging, production stabilization to product grade optimization and market adaptation guidance, helping clients quickly achieve large-scale stable production and rapid market promotion.
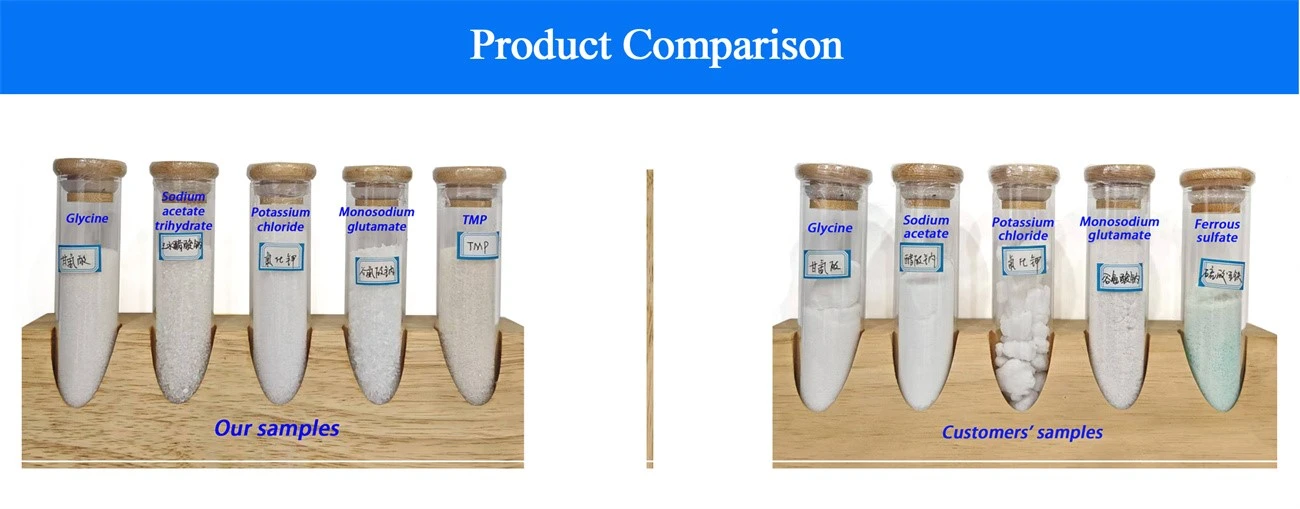
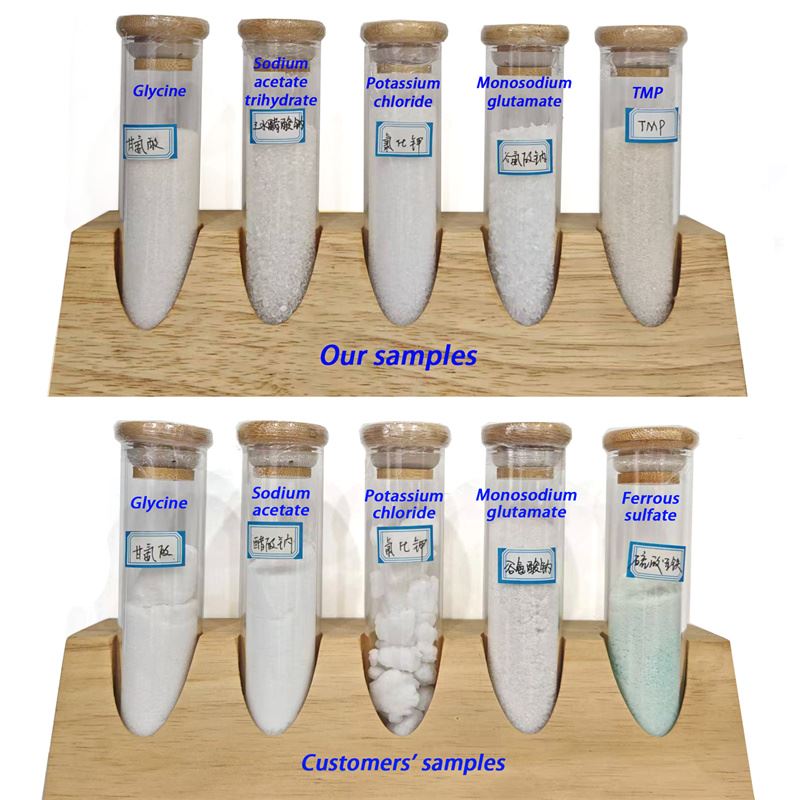
|
OUR SAMPLES |
CUSTOMERS' SAMPLES |
|
No caking |
Severe caking |
|
Large crystalline particles |
Small particles |
|
Uniform granules |
Uneven particle size |
|
Easy to transport and store |
Not suitable for transport or storage |
Related Keywords
Sodium sulfate crystallization process; Sodium sulfate crystallization technology; Sodium sulfate crystallization rd
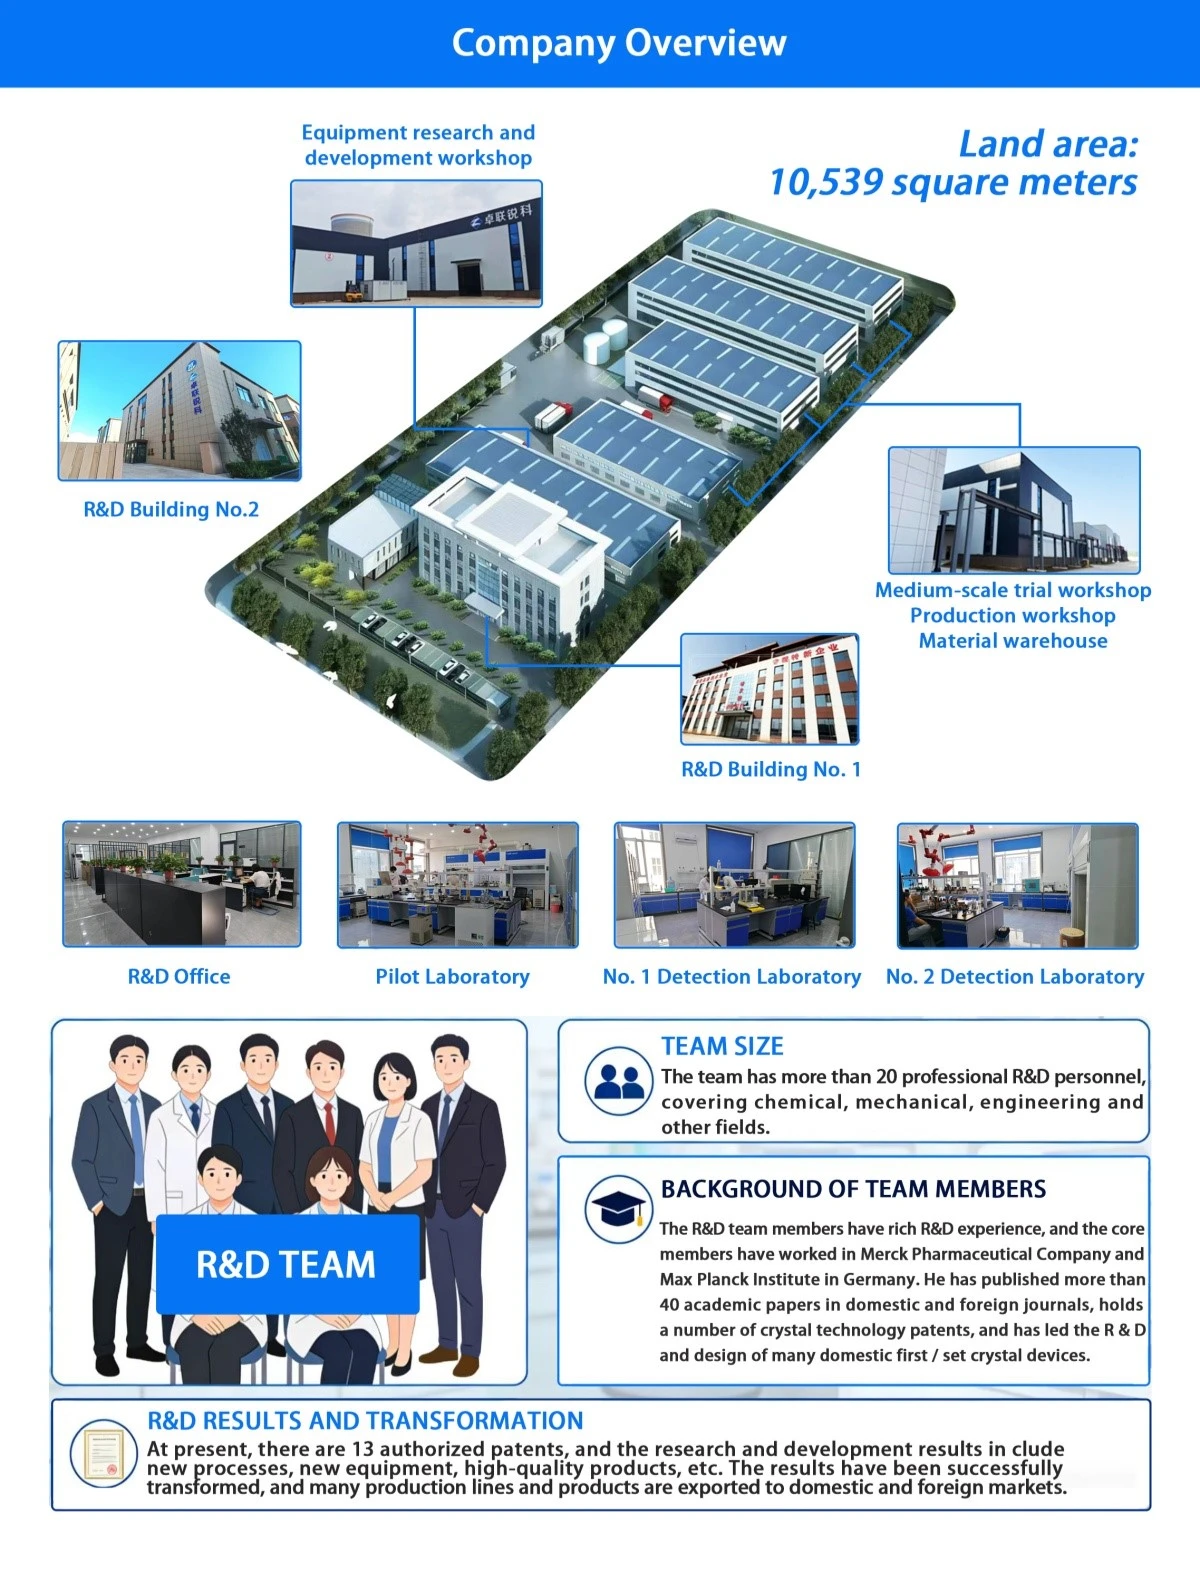
Shanxi Zhuolian Ruike Technology delivers mature, industrialized process R&D and full-scale production upgrading services for sodium sulfate, one of the most widely used general inorganic salts. Different from high-hygroscopic nitrates and variable-transition metal sulfates, sodium sulfate features stable mineral crystallization characteristics and strict industrial grading standards, requiring highly stable and scalable production technologies.
Backed by years of inorganic salt engineering experience, our company boasts fully mature sodium sulfate production processes and rich industrial project experience. We precisely solve common industry pain points including low purity consistency, unstable particle grading, high energy consumption in evaporation, excessive fine powder and low resource utilization in traditional mirabilite and synthetic production lines.
We focus on technical transformation achievement conversion and market landing promotion, providing one-stop industrial solutions covering process customization, purification optimization, pilot verification, complete equipment matching and production line commissioning. We support stable mass production of industrial-grade, high-purity and anhydrous sodium sulfate, helping global clients quickly realize product standardization, cost reduction and large-scale market popularization.
Hot Tags: sodium sulfate process research and development, China sodium sulfate process research and development manufacturers, suppliers, factory


