
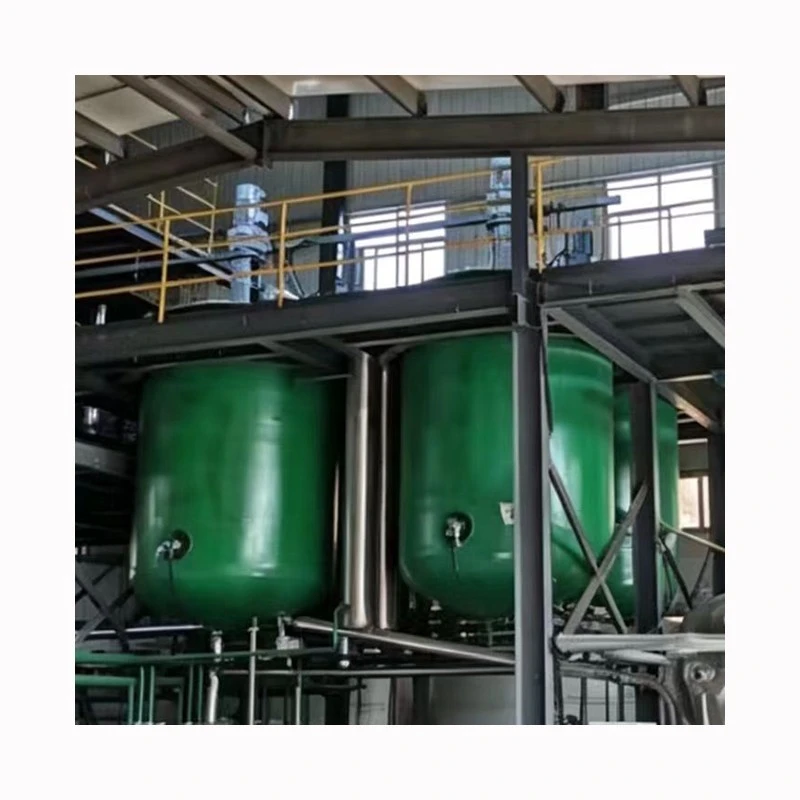
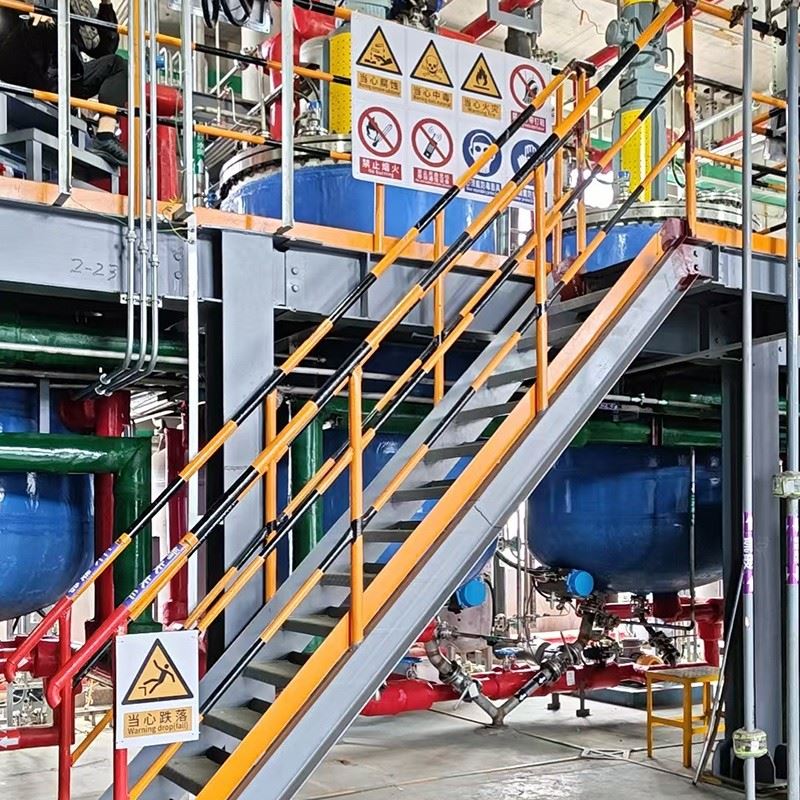
22.5m³ DTB Crystallizer Product Overview
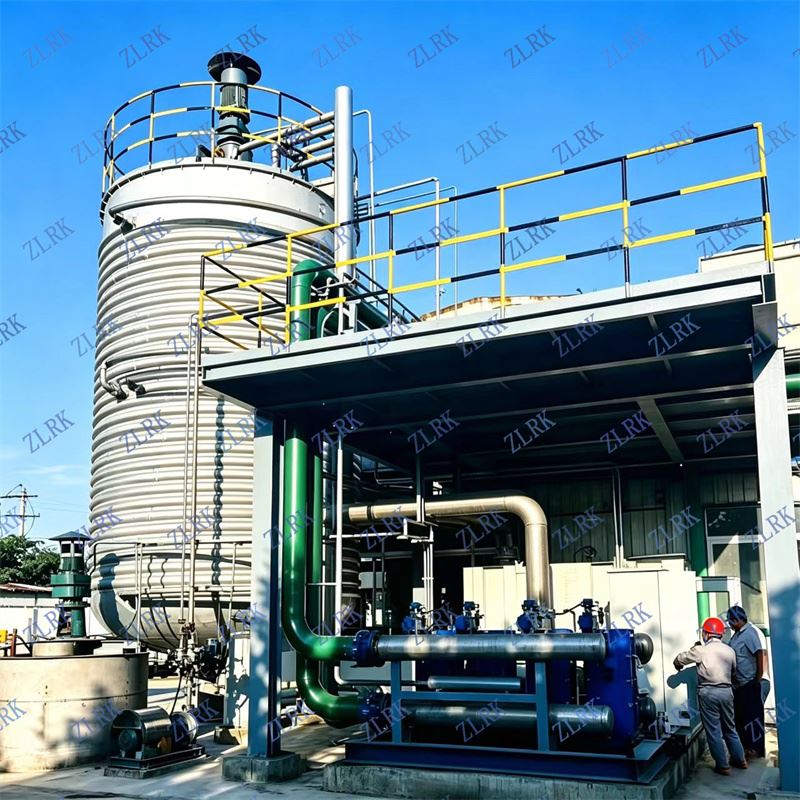
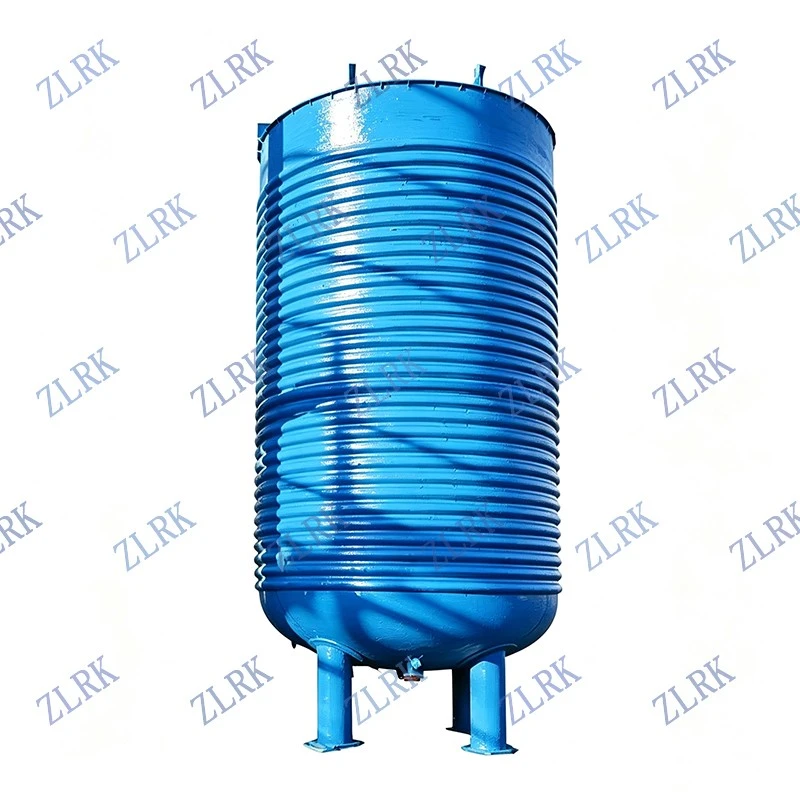
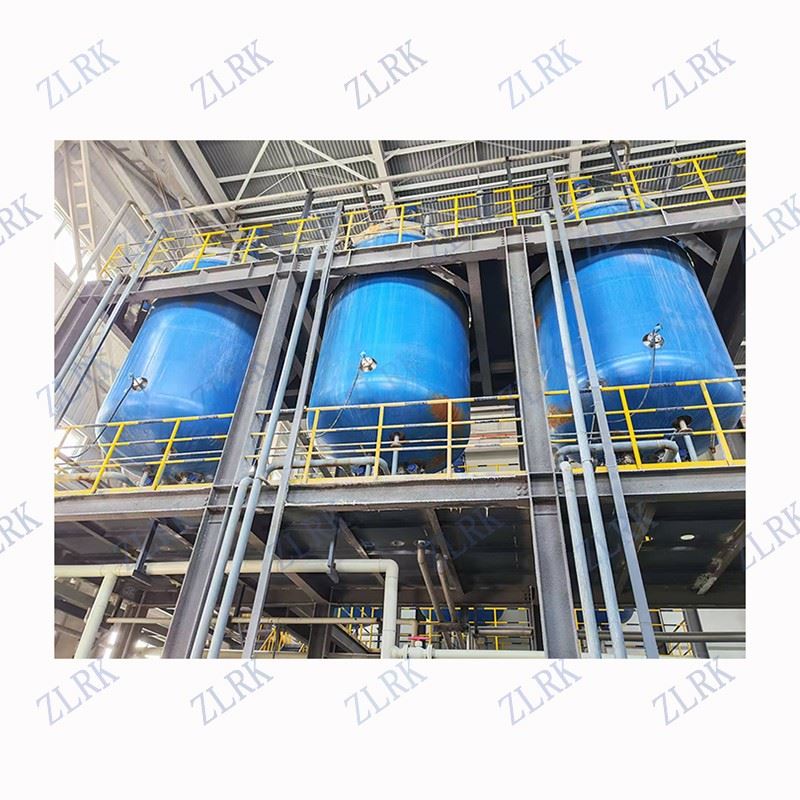
The 22.5m³ DTB crystallizer is a large-scale, high-capacity continuous crystallization unit designed for long-term stable operation. Its core advantages include uniform particle size, high purity, and ease of post-processing; large scale + high capacity + continuous and stable operation; low energy consumption, ease of operation, and long service life; broad coverage, strong resistance to interference, and high reliability. It is suitable for demanding crystallization applications in the chemical, food, and pharmaceutical industries.
Core Components
Draft Tube
Equipped with an internal agitator/axial impeller that forces the slurry to flow upward, creating a stable and controllable internal circulation.
Annular Baffle Zone
An annular channel on the outer side of the draft tube where the slurry flows downward, facilitating classification and clarification.
Clarification Zone / Sedimentation Zone
The upper region where fine crystals are discharged via clear liquid overflow, eliminating fine crystals and preventing the product from becoming too fine.
Slurry Zone / Crystallization Chamber
The lower region is a high-concentration slurry zone where crystals grow and are graded.
Heat Exchange System
Typically employs external coolers or heat exchangers for circulating heat exchange; built-in heat exchange coils may also be used.
Vacuum System
Used for evaporation cooling and to control supersaturation.
Key Features
1.Large and uniform crystal size
Stable operation with low supersaturation, reducing secondary nucleation and resulting in a narrow product particle size distribution (uniform CSD).
2.Resistant to wall scaling and scaling buildup
The flow field is well-organized with no areas of severe turbulence, significantly reducing scaling on the vessel walls.
3.Capable of continuous, stable operation
Suitable for large-scale industrial continuous production.
4.Controllable Fine Crystallization
Built-in fine-crystal elimination function effectively controls product particle size.
5.Wide Range of Applicable Systems
Suitable for inorganic salts, organic acids, evaporation crystallization, cooling crystallization, salt recovery, wastewater recycling, and more.
DTB Crystallizer Evaporation Capacity
10m³ DTB Crystallizer, 22.5m³ DTB Crystallizer, 30m³ DTB Crystallizer, 75m³ DTB Crystallizer, 85m³ DTB Crystallizer; OSLO Crystallizer; FC Continuous Crystallizer.
(Designed according to user requirements)
DTB Crystallizer Equipment Materials
SUS304; 316L; titanium alloy; Q235B, etc.
Product-Related Keywords
Wastewater crystallizer; syrup crystallizer; metal salt crystallizer
Product Specification
|
Crystallizer Type |
DTB Crystallizer |
FC Continuous Crystallizer |
OSLO Crystallizer |
|
Core Circulation Method |
Internal slurry circulation |
External slurry circulation |
External mother liquor circulation |
|
Crystal Growth Zone |
Inside the flow guide tube |
Within the entire fluidized bed of the cylinder |
Upper settling and growth zone of the crystallizer |
|
Fine-Grain Treatment |
Settling zone around the baffles + leaching column; fine crystals are eliminated via recirculation |
Fine crystals are broken down by circulation pumps, and dissolution occurs naturally due to supersaturation |
External fine crystal removal heater; fine crystals are recirculated separately for dissolution |
|
Crystal Grain Size |
Medium to large, 0.5–1.5 mm; good uniformity |
Medium, 0.3–1.0 mm, with a tendency toward finer particles |
Maximum crystal size: 1.0–3.0 mm; most uniform particle size |
|
Nucleation Control |
Low agitation, low supersaturation, minimal secondary nucleation |
High shear force from circulation pumps leads to frequent secondary nucleation |
No pump shear; minimal nucleation; highest crystal purity |
|
Susceptibility to Scarring |
External heat exchange surfaces; slurry does not contact heat exchange surfaces, reducing scaling |
The slurry flows through the heat exchanger, causing high-speed scouring but prone to scaling and blockage |
Only the mother liquor passes through the heat exchanger, resulting in virtually no scaling |
|
Energy Consumption Characteristics |
Internal circulation, low-speed agitation, lower energy consumption |
High-flow external circulation pump; highest energy consumption |
High mother liquor circulation flow rate, moderate energy consumption |
|
Typical Advantages |
Simple structure, stable operation, easy maintenance, high overall cost-effectiveness |
High circulation volume and processing capacity; suitable for high-viscosity/high-solids-content materials |
Largest and purest crystals, best product consistency; the top choice for high-end crystallization |
|
Typical Disadvantages |
Upper limit of crystal size is lower than that of the OSLO |
Relatively fine grain size, high energy consumption, and high risk of scaling |
Complex equipment, high cost, large footprint |
|
Examples of Suitable Materials |
Ammonium sulfate, potassium chloride, magnesium sulfate, sodium sulfate, boric acid |
Sodium chloride, urea, diammonium phosphate, high-solids-content inorganic salts |
Citric acid, lysine, pharmaceutical intermediates, high-end fine chemicals |
Product Properties-22.5m³ DTB Crystallizer
Wide Range of Applicable Materials
Suitable for evaporation crystallization, cooling crystallization, and vacuum flash crystallization; ideal for materials with steep solubility curves and a tendency to form scale, such as sodium chloride, nitrates, ammonium sulfate, vitamin C, and monosodium glutamate.
01
Meets GMP and Cleanroom Requirements
The design features no dead corners, is easy to clean, and provides reliable sealing, making it suitable for clean production environments in the pharmaceutical and food industries.
02
Significant Economies of Scale
A single unit can meet medium- to large-scale production demands, reducing the number of units, pipelines, and control points, and lowering total investment and O&M costs.
03
More Stable Circulation and Classification
A large chamber combined with a large flow-guiding cylinder ensures more uniform fluid distribution, superior classification performance, and better consistency in crystal quality.
04
Compatible with MVR and Multi-Effect Evaporation
Efficiently integrates with MVR and multi-effect evaporation systems to further reduce overall energy consumption, making it suitable for applications such as zero-discharge of high-salt wastewater and salt-nitrate separation.
05
Typical Applications
- Inorganic salts, such as sodium sulfate, sodium chloride, ammonium chloride, ammonium sulfate, and nitrates.
- Chemical intermediates and organic acids.
- Food additives and sweeteners.
- Lithium extraction from salt lakes and salt chemical industry.
- Zero-discharge of industrial wastewater and recovery of salts from evaporation and crystallization.
Company R&D Capabilities
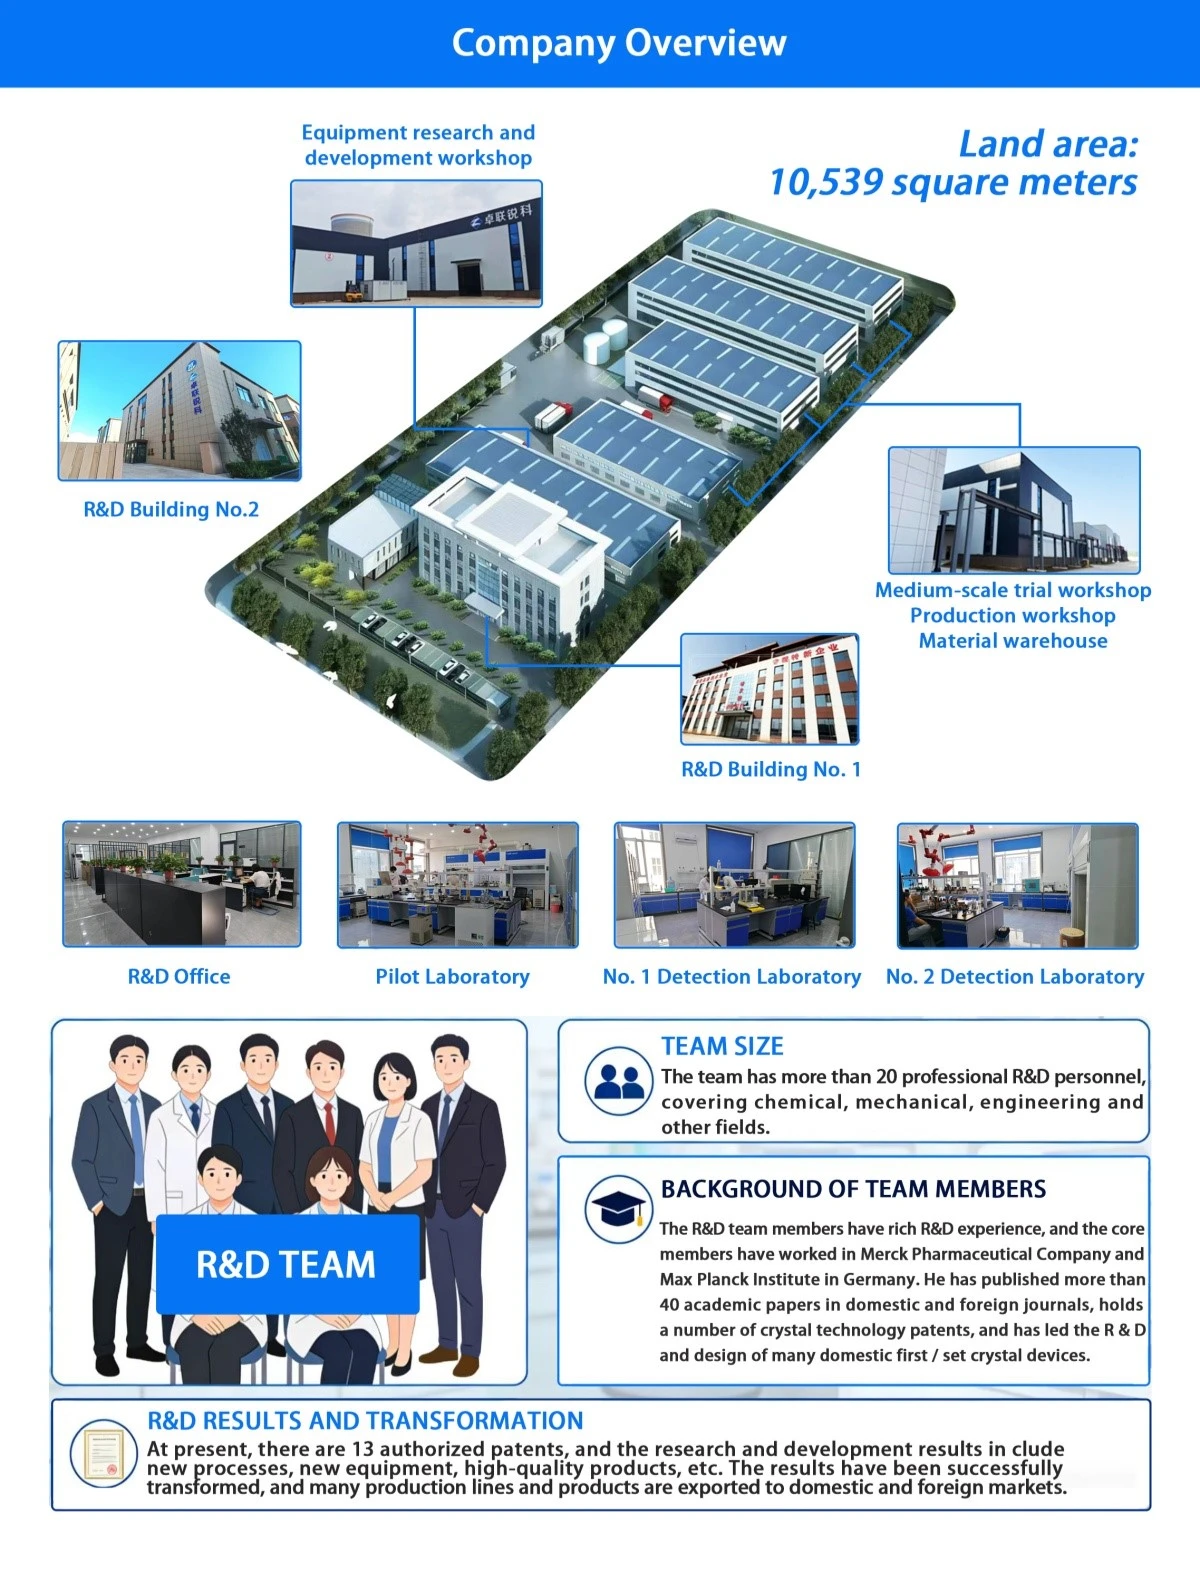
We have a team of over 20 professional R&D personnel spanning multiple fields, including chemistry and engineering.
Team members possess extensive R&D experience; key members have previously worked at Merck & Co. in the U.S. and the Max Planck Society in Germany. They have published more than 40 academic papers in domestic and international journals, hold multiple patents for crystallization technologies, and have led the R&D and design of numerous crystallization units that were the first of their kind in China.
We operate state-of-the-art laboratories and pilot-scale R&D facilities equipped with advanced experimental equipment and instruments, providing robust support for our R&D efforts.
At present, We hold 13 authorized patents and have developed new processes, new equipment, and high-quality products.
Our R&D achievements have been successfully commercialized into multiple production lines, with products sold both domestically and internationally.
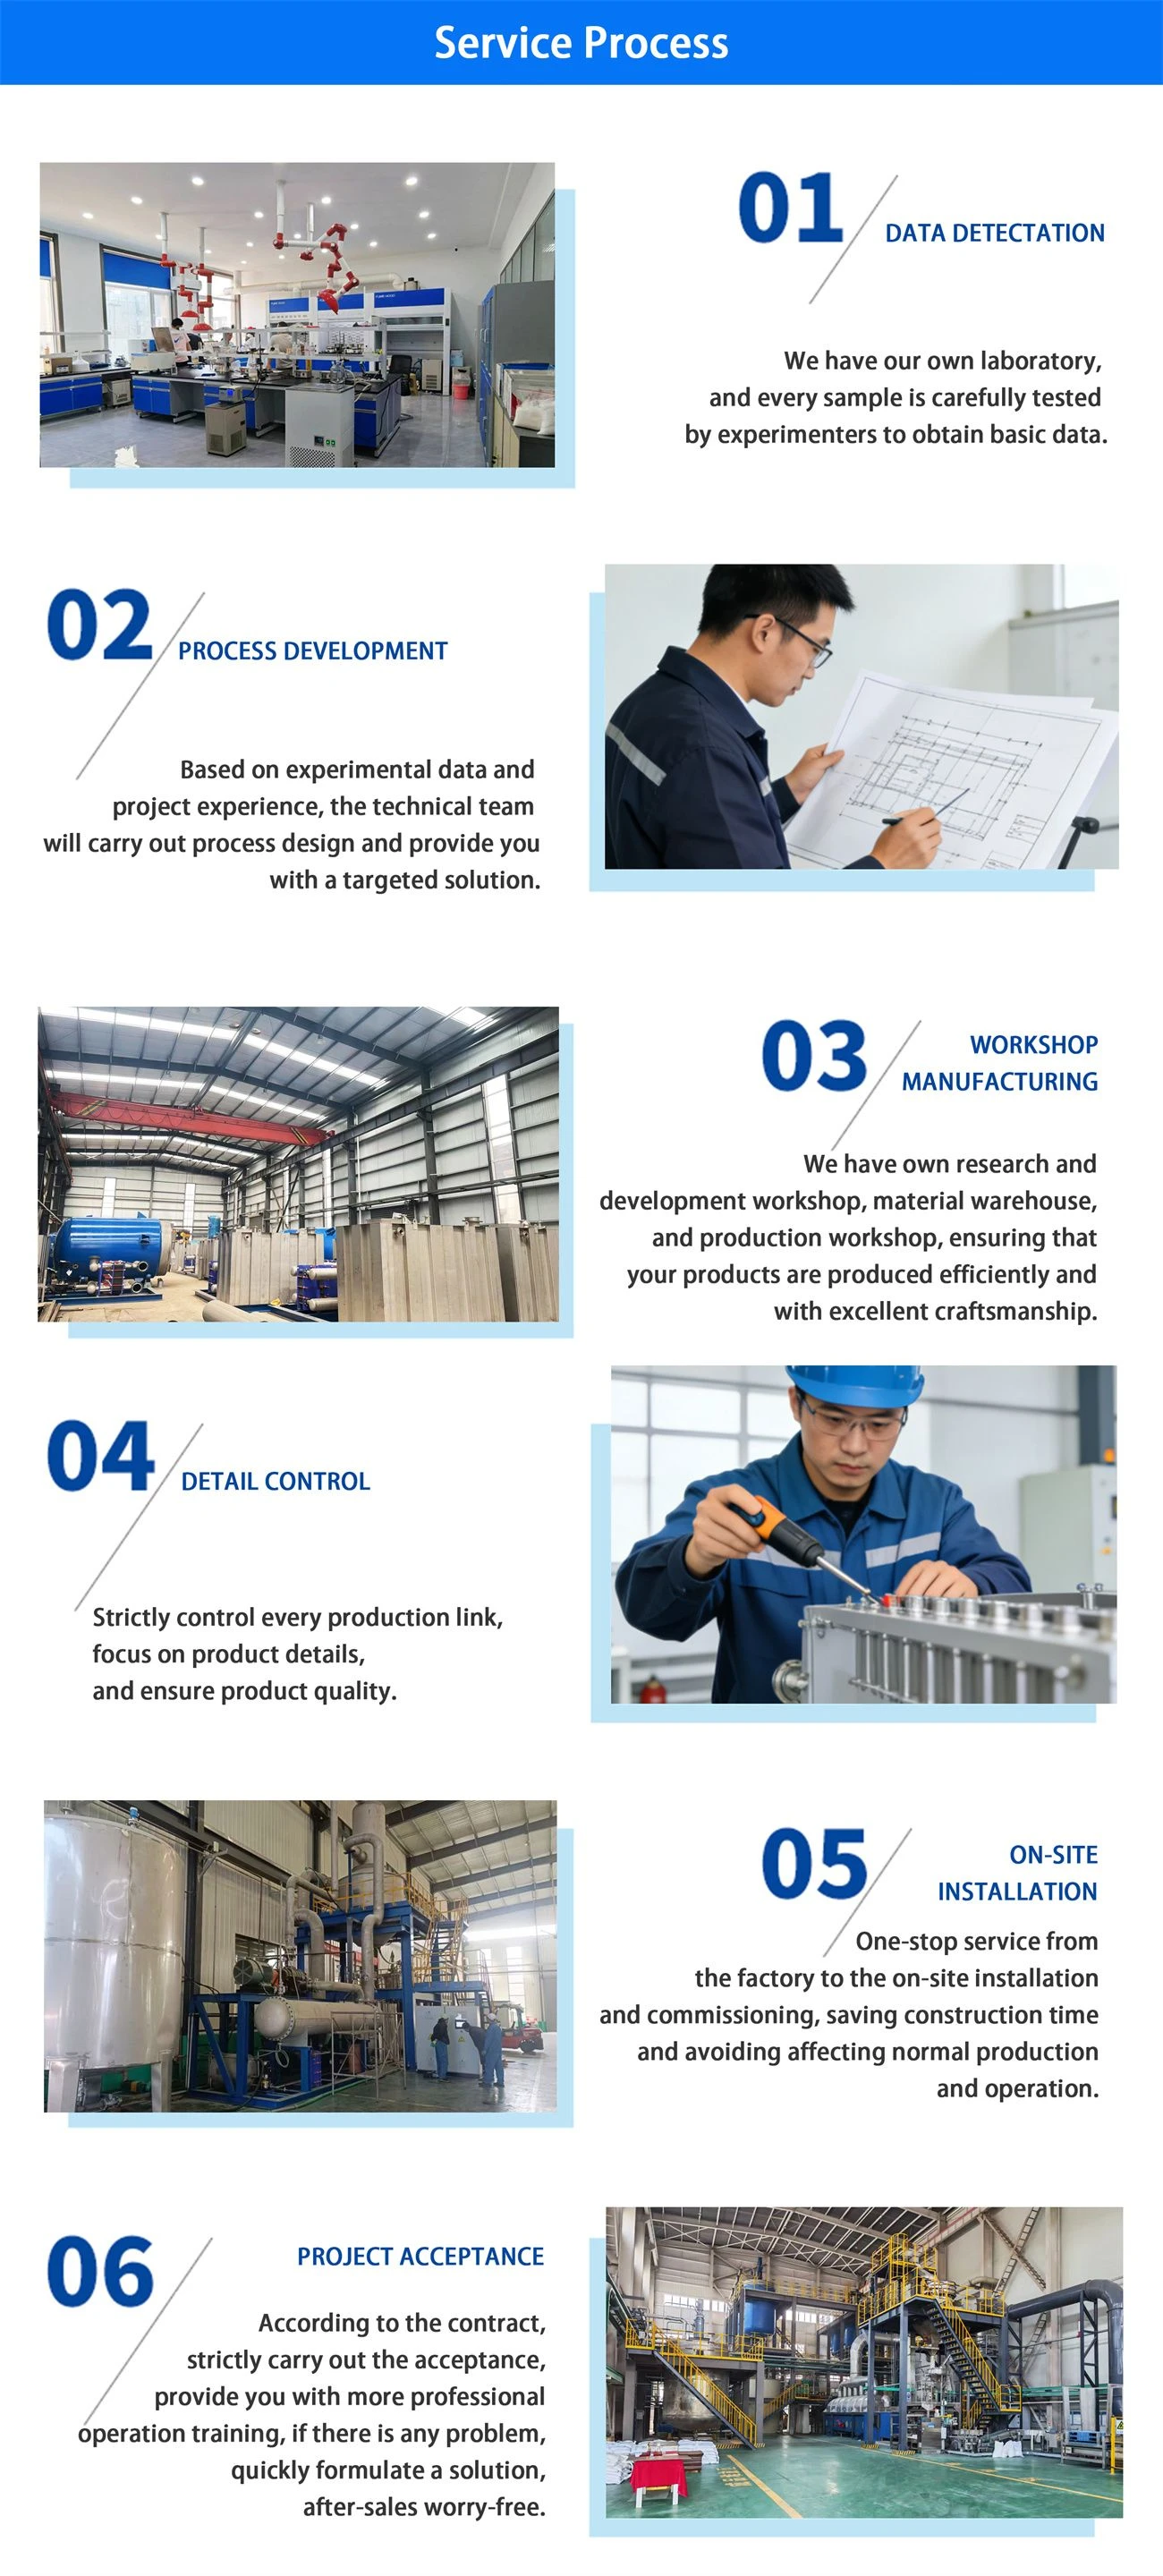
Service Process
Collect experimental data: We have our own laboratory, and every sample is carefully tested by experimenters to obtain basic data.
Process development: Based on experimental data and project experience, the technical team will carry out process design and provide you with a targeted solution.
Workshop manufacturing: We have our own research and development workshop, material, warehouse and production workshop, ensuring that your products are produced efficiently and with excellent craftsmanship.
Detail control: Strictly control every production link, focus on product details and ensure product quality.
On-site installation: One stop service from the factory to the on-site installation and commissioning, saving construction time and avoiding affecting normal production and operation.
QA&QC
Q: Is customization available?
A: Yes
Q: Can you provide spare parts and remote support as needed?
A: Yes
Q: Can you provide photos or videos of the production process?
A: Yes
Q: Does the user interface support English and local languages?
A: Yes
Hot Tags: 22.5m³ dtb crystallizer, China 22.5m³ dtb crystallizer manufacturers, suppliers, factory


