
75m3 DTB Crystallizer for Ultra-Large-Scale 24/7 Industrial Crystallization Production
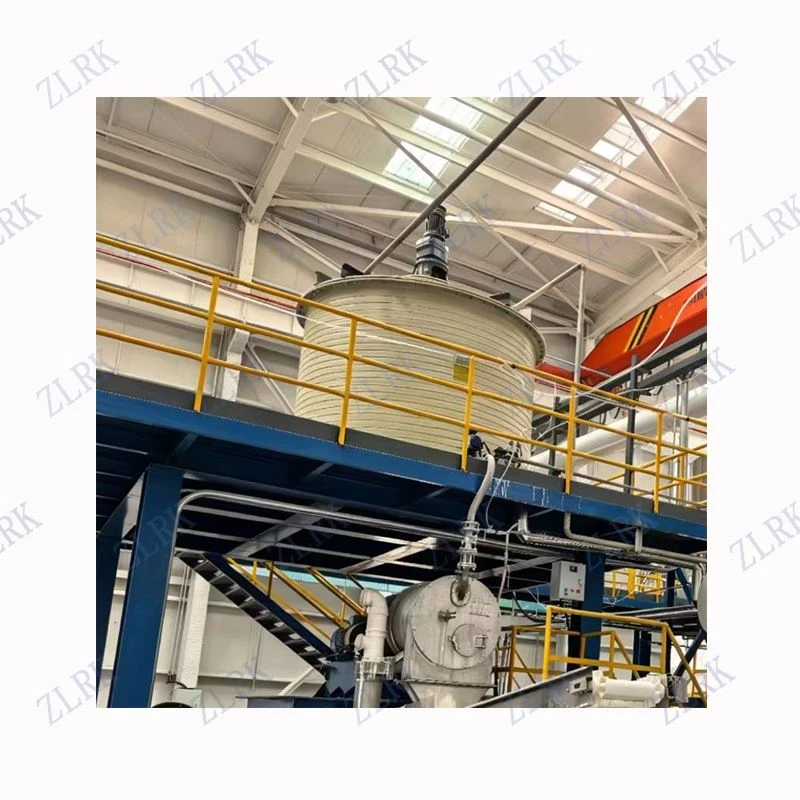
Shanxi Zhuolianruike Technology Co., Ltd. (ZLRK) delivers professional grade 75m3 DTB (Draft Tube Baffle) Crystallizer tailored exclusively for super-large industrial parks, high-load zero-discharge projects and mass chemical raw material production.
As our flagship ultra-large capacity crystallization equipment, the 75 cubic meters DTB crystallizer breaks through the output limitations of medium and conventional large-scale crystallization devices. It is specially engineered for scenarios requiring 24-hour continuous operation, ultra-high material throughput and stable large-grain crystal batch production. Different from 10m3 and 30m3 standard models suitable for medium production lines, this 75m3 upgraded version adopts ultra-large tank body structure, high-power circulating system and multi-stage crystal classification technology, perfectly matching the super-scale production demands of modern heavy industry while maintaining low energy consumption and stable operating performance.
Product Specification
|
Crystallizer Type |
DTB Crystallizer |
|
Core Circulation Method |
Internal slurry circulation |
|
Crystal Growth Zone |
Inside the flow guide tube |
|
Fine-Grain Treatment |
Settling zone around the baffles + leaching column; fine crystals are eliminated via recirculation |
|
Crystal Grain Size |
Medium to large, 0.5–1.5 mm; good uniformity |
|
Nucleation Control |
Low agitation, low supersaturation, minimal secondary nucleation |
|
Susceptibility to Scarring |
External heat exchange surfaces; slurry does not contact heat exchange surfaces, reducing scaling |
|
Energy Consumption Characteristics |
Internal circulation, low-speed agitation, lower energy consumption |
|
Typical Advantages |
Simple structure, stable operation, easy maintenance, high overall cost-effectiveness |
|
Typical Disadvantages |
Upper limit of crystal size is lower than that of the OSLO |
|
Examples of Suitable Materials |
Ammonium sulfate, potassium chloride, magnesium sulfate, sodium sulfate, boric acid |
Product Brief & Working Principle
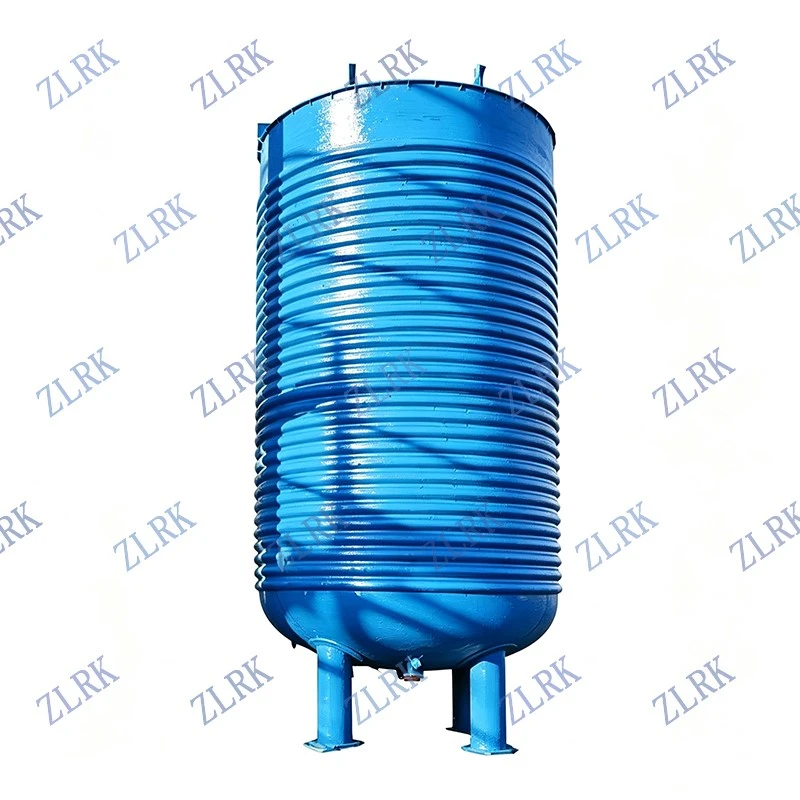
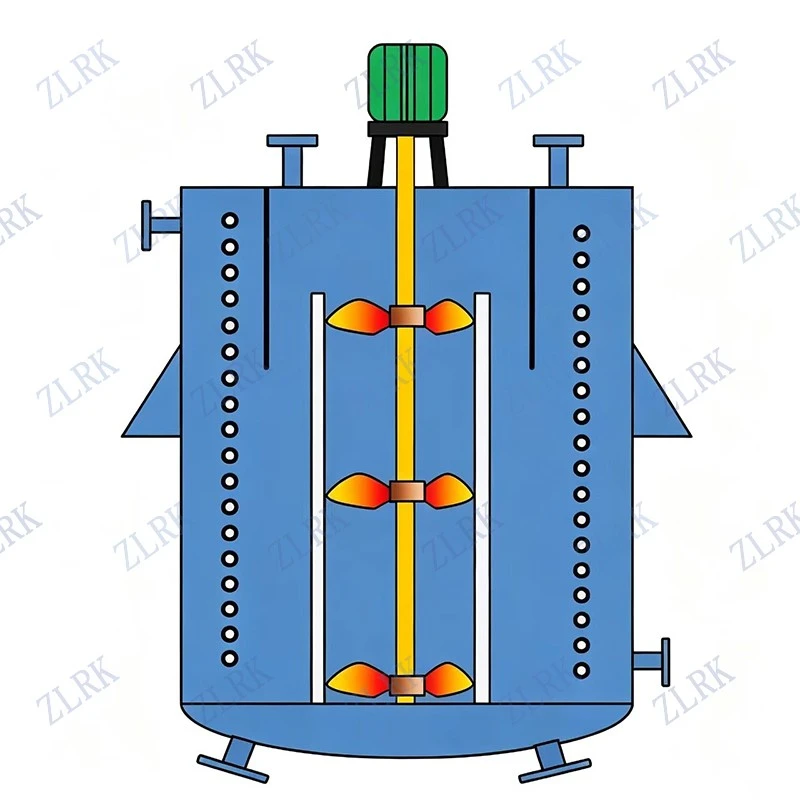
The 75m3 DTB crystallizer is a high-efficiency suspension classification crystallization system designed for super-large flow industrial materials. The equipment adopts an integrated reinforced pressure-bearing tank body with ultra-large effective volume, equipped with an extended super-large draft tube, multi-group annular baffle assemblies and variable-frequency high-torque circulating impellers. The overall structural layout eliminates flow dead zones and material stratification problems easily occurring in large-volume equipment, realizing full-tank uniform circulation and stable supersaturation balance.
In industrial operation, the mass raw material liquid is continuously and quantitatively fed into the central draft tube. Driven by the low-speed high-power circulation system, the solution forms a stable laminar rising flow. Through vacuum evaporation or gradient cooling, the liquid reaches uniform supersaturation, providing a stable growth environment for crystal particles. Relying on the ultra-large tank capacity, materials obtain sufficient growth residence time to ensure full particle maturation. Mature large-particle crystals settle down by gravity for centralized continuous discharge, while fine crystals and uncrystallized mother liquor are screened by multi-stage baffles and delivered to the fine crystal dissolution system for secondary circulation treatment. The whole process realizes uninterrupted feeding, growth, classification and discharging, solving the problems of unstable output and uneven particle size of traditional large-scale crystallization equipment.
With ultra-large processing capacity, super-stable continuous operation performance and strong material adaptability, the 75m3 DTB crystallizer is mainly applied to super-large industrial projects that cannot be covered by conventional specifications, covering core heavy industry fields:
Super-Large Chemical Base Production: Suitable for mass crystallization and purification of industrial raw materials such as sodium chloride, sodium sulfate, ammonium sulfate and potassium nitrate. It supports round-the-clock batch production of chemical bases, effectively improving overall factory output and product consistency.
Industrial Park Wastewater Zero-Discharge: Ideal for centralized high-salt wastewater treatment in chemical industrial parks, printing and dyeing clusters and electroplating industrial zones. It efficiently separates and recycles various soluble salts in wastewater, realizing resource reuse and meeting ultra-high environmental protection standards.
New Energy Mass Manufacturing: Applied to large-scale recycling and crystallization of lithium, nickel and cobalt salt solutions in power battery production, as well as purification and forming of new energy raw materials, adapting to the mass production rhythm of new energy super factories.
Heavy Industry Fine Chemical Refining: Used for crystallization and purification of large-batch fine chemical intermediates and inorganic salt products. The stable low-turbulence environment ensures high purity and uniform particle size of finished products.
Our Core Product Advantages
1. Ultra-Large Volume & Super High Yield
The 75m3 super-large effective volume achieves a qualitative leap in single-machine processing capacity, replacing the parallel operation of multiple 30m3 equipment. It simplifies production line layout, reduces equipment investment and site occupation, and greatly lowers manual operation and maintenance costs. It is the most cost-effective solution for super-large batch crystallization production.
2. Multi-Stage Classification & High-Quality Crystal Output
Equipped with customized multi-group baffle classification structure and intelligent fine crystal elimination system, the equipment precisely controls solution supersaturation and avoids excessive nucleation. The ultra-long material residence time ensures full crystal growth. The finished products feature uniform particle size, high density and extremely low fine powder rate, effectively improving downstream product grade and market competitiveness.
3. Reinforced Anti-Scaling & Super Stable Operation
The tank body adopts integral thickened molding and mirror polishing process, with optimized internal fluid trajectory design. It avoids local material over-concentration and wall adhesion under high-load operation. Matched with automatic circulating flushing configuration, it effectively suppresses scaling and blockage, supports long-term uninterrupted operation, and reduces shutdown maintenance frequency.
4. High Adaptability & Intelligent Customization
Based on the standard 75m3 structure, we provide diversified material upgrades including 316L stainless steel, duplex stainless steel and pure titanium to adapt to strong acid, strong alkali and high-corrosion working conditions. It can be matched with full PLC automatic control, remote data monitoring and automatic discharge systems to realize unmanned intelligent production.
Professional R&D and Design Strength
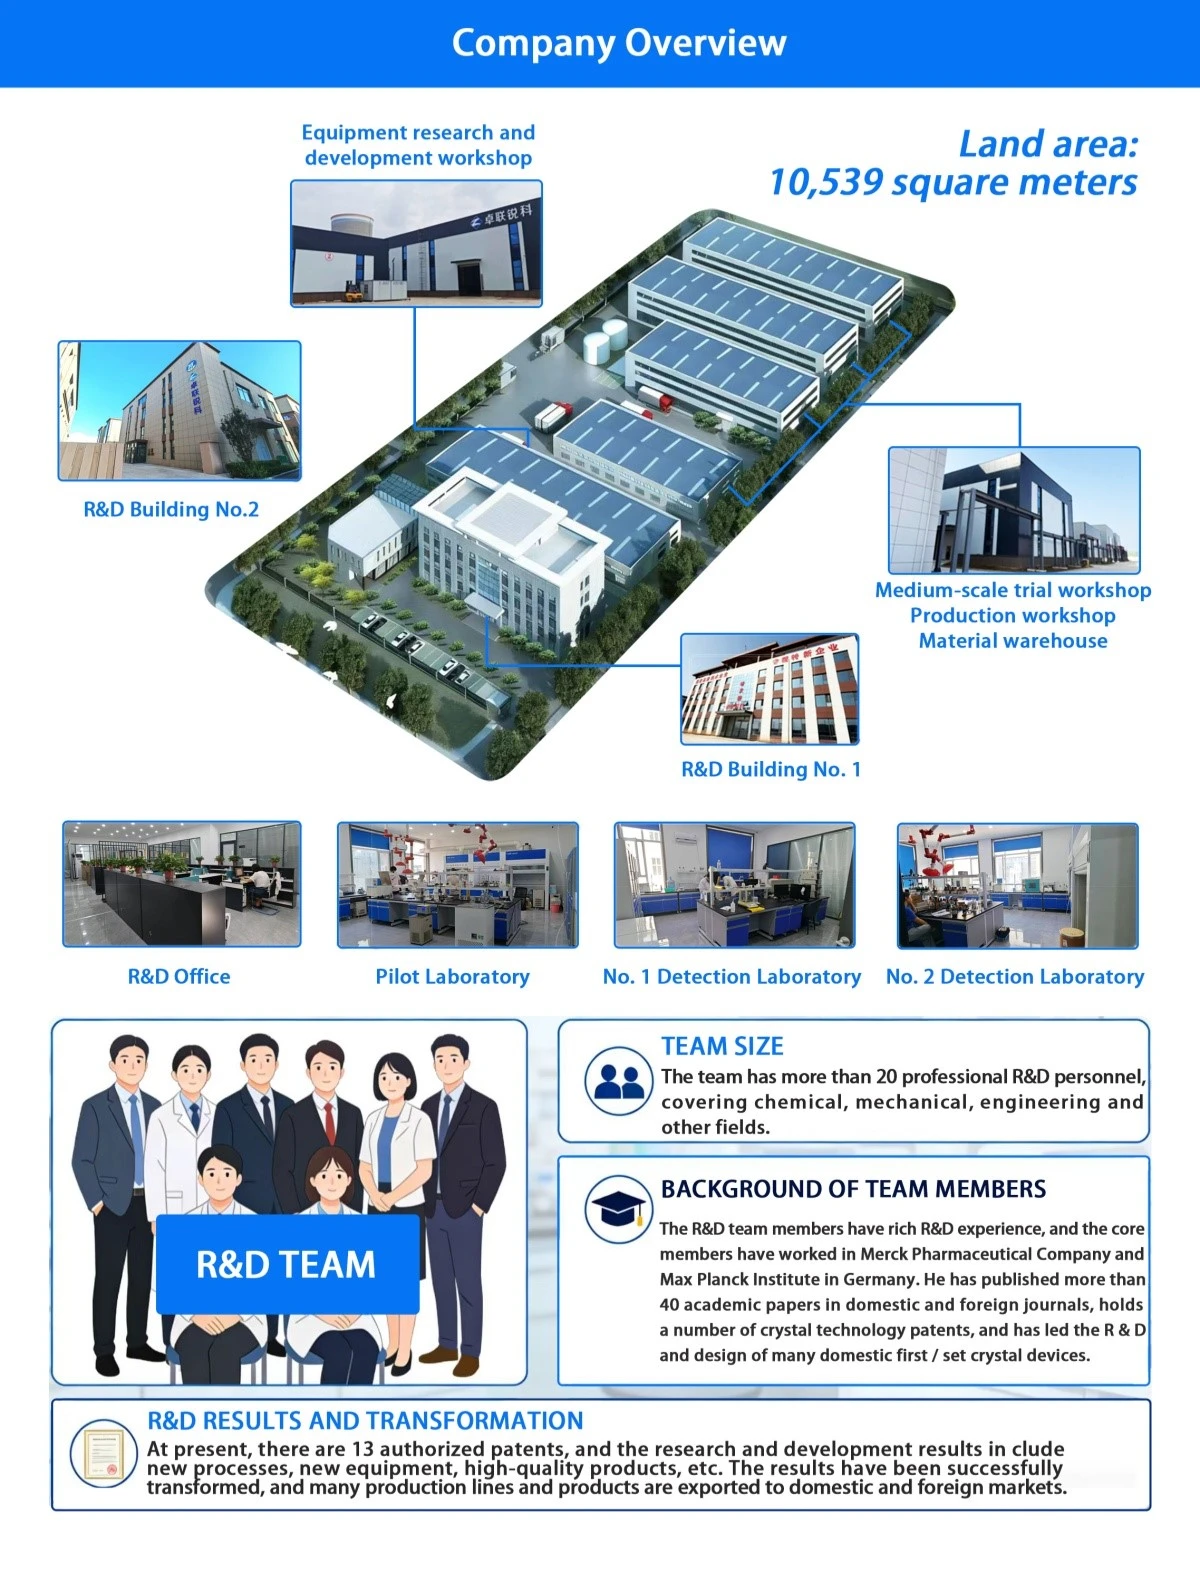
Our technical team has rich experience in the design of super-large industrial crystallization equipment. For the 75m3 ultra-large DTB crystallizer, we adopt finite element fluid simulation and pressure mechanical finite element analysis to iteratively optimize core parameters such as draft tube specification, baffle angle, circulating power and flow field distribution. The reinforced tank body structure strictly meets industrial pressure-bearing and safety standards, solving the technical pain points of uneven flow field and unstable pressure of traditional ultra-large crystallization equipment. All equipment undergoes strict pressure testing, welding flaw detection and simulated working condition debugging before delivery, and can realize personalized structural optimization according to customer unique material characteristics and production indicators.
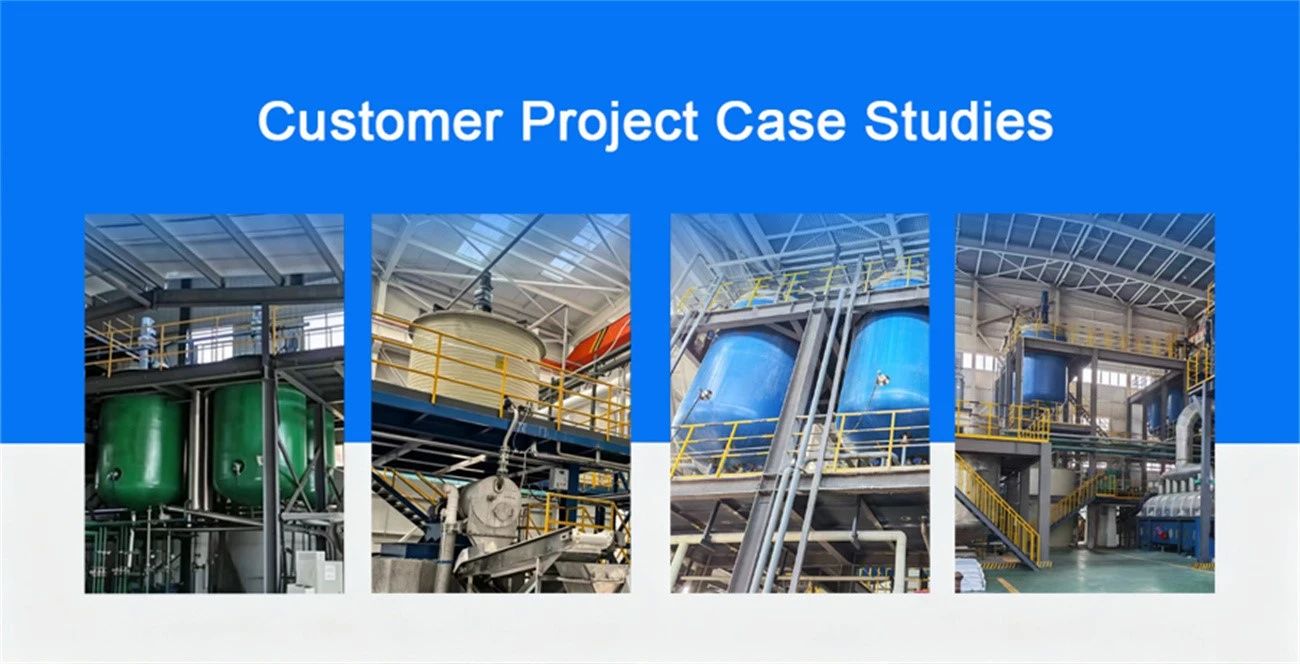
Our 75m3 DTB ultra-large crystallizers have been successfully applied in many domestic and foreign super-large chemical parks and environmental protection zero-discharge projects. We have accumulated mature engineering experience in high-load continuous crystallization, super-large flow material treatment and high-purity salt recovery. All equipment operates stably in long-term high-intensity industrial scenarios, with low failure rate and high production efficiency, winning long-term strategic cooperation and high recognition from global industrial customers.
Full-Lifecycle After-Sales Service
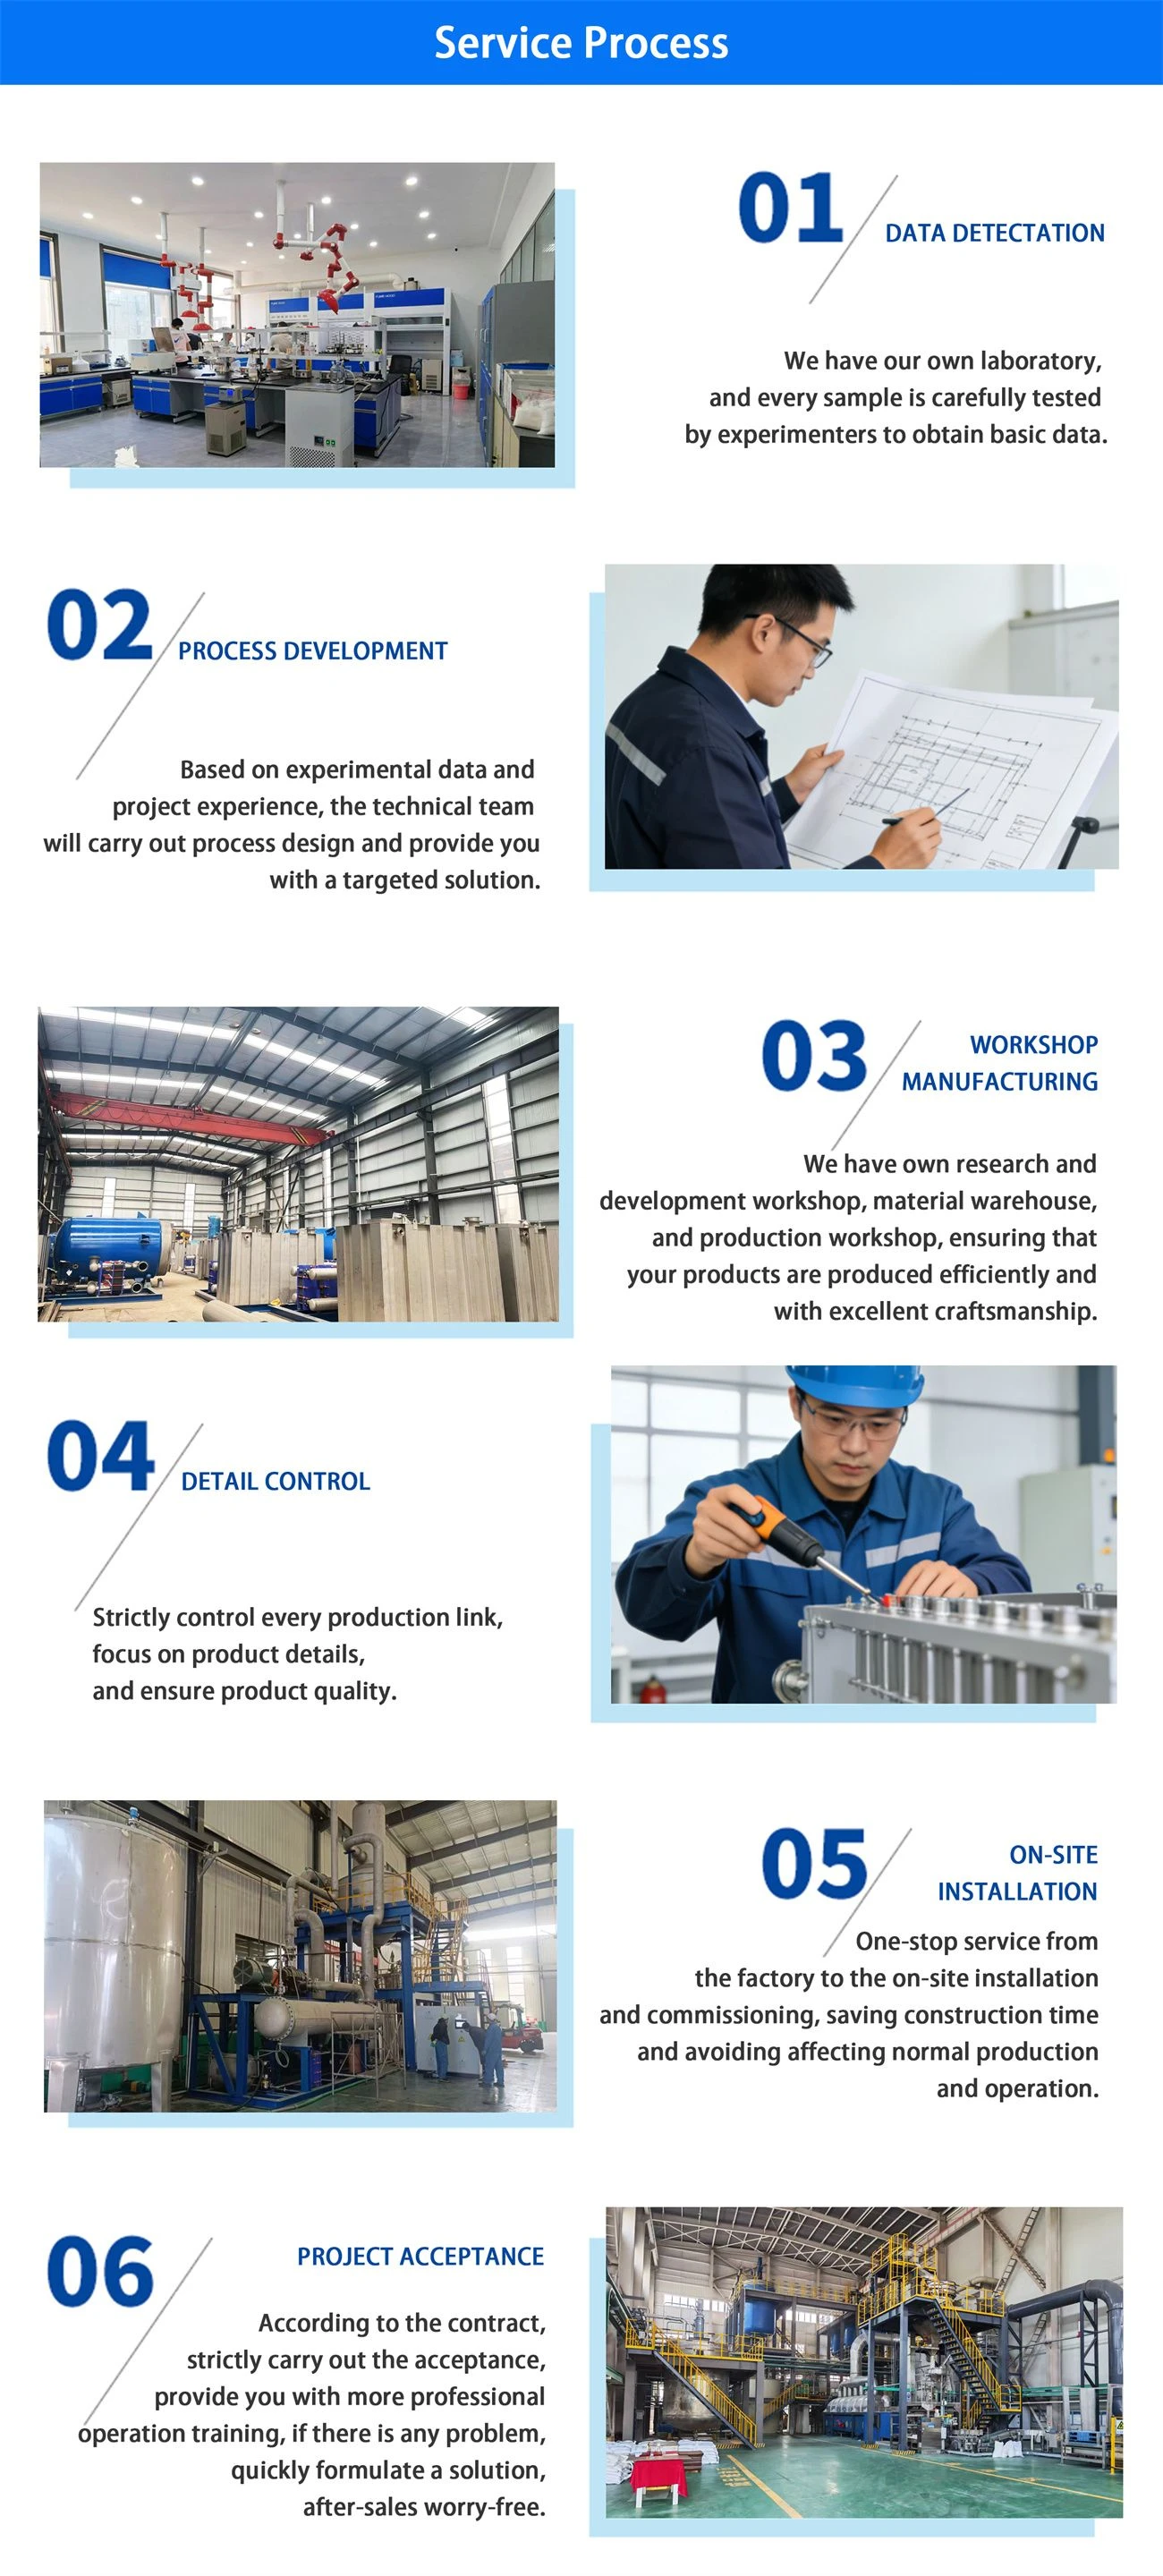
We provide one-stop full-cycle supporting services for all 75m3 DTB crystallizer products. Pre-sale, we offer free working condition analysis, process scheme customization and parameter matching optimization. In-production, we implement full-process quality supervision to ensure compliance with international industrial standards. After-sale, we provide complete installation guidance, on-site commissioning, operator training and long-term fault maintenance, spare parts supply and technical upgrade services, fully guaranteeing the long-term stable and efficient operation of customer production lines.
Contact us for professional technical parameters, real project cases and exclusive factory quotation to customize your ultra-large crystallization production solution!
Hot Tags: 75m³ dtb crystallizer, China 75m³ dtb crystallizer manufacturers, suppliers, factory


