
þ85m3 DTB Crystallizer for Full-Scale Continuous Industrial Crystallization & Salt Recovery
Shanxi Zhuolianruike Technology Co., Ltd. (ZLRK) presents the 85m3 DTB (Draft Tube Baffle) Crystallizer, a high-flow premium-grade crystallization unit engineered for full-scale industrial manufacturing and large-volume wastewater resource recovery. Positioned between standard large-capacity and ultra-heavy industrial models, the 85 cubic meters DTB crystallizer fills the market gap for high-throughput, high-precision crystallization projects that demand balanced output stability and flexible load adjustment. Unlike conventional fixed-volume crystallizers with single operating modes, this 85m3 model features upgraded flow field layout, optimized gradient crystallization logic and enhanced load resistance structure. It is perfectly suited for modern industrial scenarios requiring variable-flow continuous production, high-purity crystal grading and long-cycle unattended operation, delivering higher operational flexibility and economic benefits for global large-scale production bases.
þProduct Overview & Working Principle
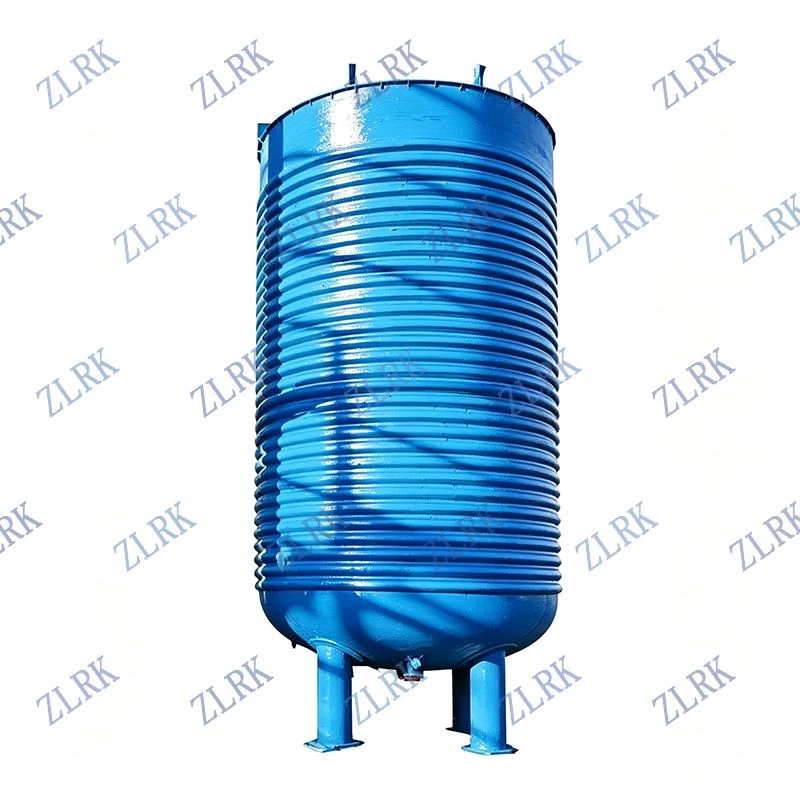
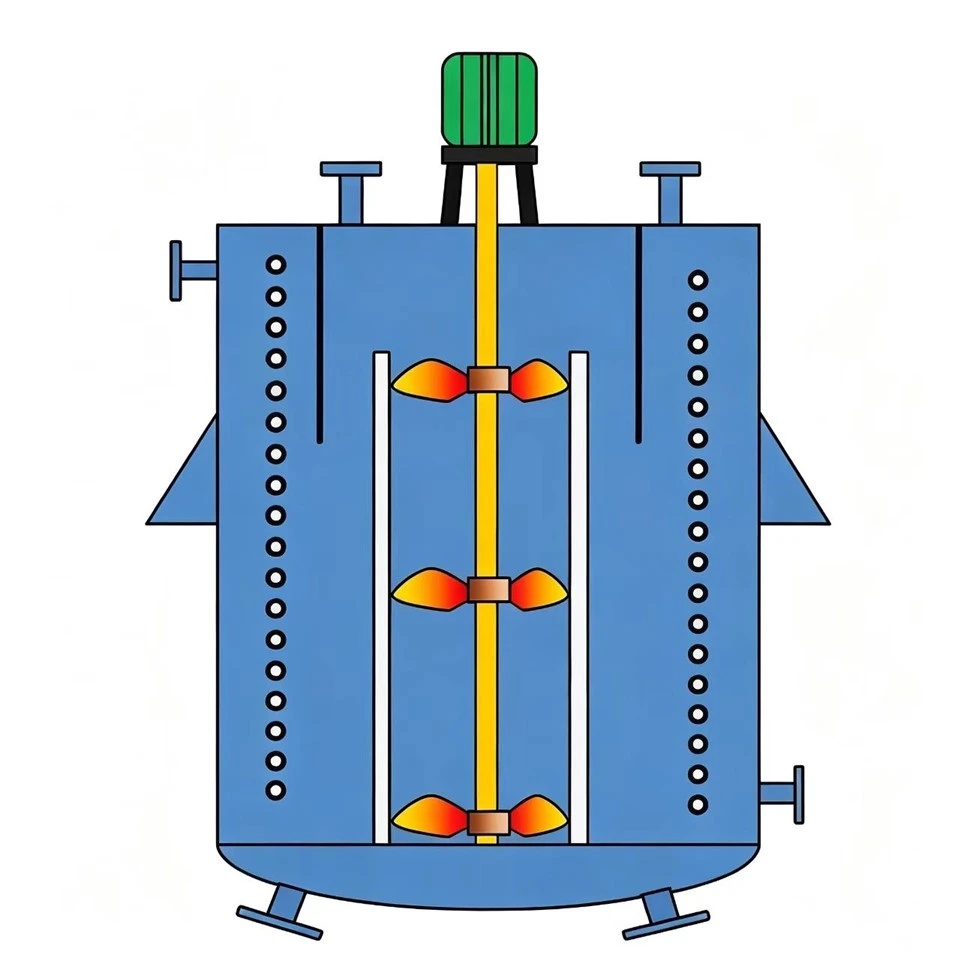
The 85m3 DTB crystallizer is an advanced suspended particle classification crystallization system optimized for variable industrial working conditions. It adopts an integrally forged pressure-resistant tank body with standardized 85m3 effective working volume, paired with an enlarged variable-diameter draft tube, multi-layer segmented baffles and frequency-conversion adaptive circulating impellers. The upgraded structural design effectively solves common defects of traditional large crystallizers, such as poor flow field uniformity, insufficient crystal grading precision and limited load adjustment range, achieving full-tank dynamic balance of solution supersaturation.
During formal operation, process feed liquid is stably injected into the central draft tube through a closed quantitative feeding system. Driven by adaptive low-shear circulation power, the solution rises steadily in a layered flow state, forming uniform supersaturation via vacuum evaporation or temperature-controlled cooling. Benefiting from the reasonable volume gradient design, crystal particles achieve staged growth in independent growth zones, avoiding particle collision and fragmentation. Qualified large-size crystals settle and are discharged automatically, while micro-fine crystals and mother liquor pass through segmented baffles into the fine crystal dissolution circulation loop for reprocessing.
The entire working process realizes dynamic circulation of feeding, nucleation, graded growth and automatic discharging, supporting 24-hour continuous stable production with outstanding product consistency.
With flexible load adaptability, high-precision crystal classification and large-flow processing capacity, the 85m3 DTB crystallizer covers diversified high-standard industrial scenarios, serving as a core equipment for medium-to-super scale production lines:
Industrial Salt Large-Scale Refining: Ideal for standardized crystallization and purification of potassium sulfate, magnesium chloride, industrial sodium salt and other inorganic salts. It supports continuous mass production with controllable particle size, helping enterprises obtain high-grade industrial salt products.
Park-Level Wastewater Resource Recovery: Suitable for centralized treatment of mixed high-salt wastewater from chemical, pharmaceutical and textile industries. It efficiently separates mixed salts, realizes wastewater zero discharge and resource recycling, and complies with international environmental compliance standards.
Lithium & New Energy Material Purification: Applied to crystallization recovery of battery-grade salt solutions and pretreatment of new energy raw materials. The low-shear growth environment protects material activity and meets strict purity requirements for new energy manufacturing.
Biochemical & Fine Chemical Production: Adaptable to crystallization of heat-sensitive biochemical products and fine chemical intermediates. Its precise temperature and supersaturation control effectively preserves product quality and improves finished product yield.
Exclusive Product & Manufacturer Advantages
1. Balanced Large Flow & Flexible Load Regulation
The 85m3 optimized volume achieves a perfect balance between ultra-large processing capacity and operational flexibility. It supports 30%–100% variable load adjustment, adapting to fluctuating feed liquid concentration and flow rate in industrial production. Compared with fixed large-volume equipment, it avoids energy waste under low-load conditions and solves the insufficient output problem of medium-sized units, greatly improving overall production cost performance.
2. Segmented Grading & Ultra-Low Fine Crystal Rate
Equipped with self-developed multi-layer segmented baffle grading technology, the equipment realizes staged screening and growth of crystal particles. The intelligent supersaturation closed-loop control system inhibits excessive secondary nucleation effectively. Finished crystals feature uniform particle size, high bulk density and ultra-low fine powder content, reducing subsequent filtration and drying pressure and improving final product qualification rate.
3. Anti-Fouling Structure & High Operational Stability
The internal tank adopts super smooth polishing and streamlined flow channel optimization, eliminating material dead corners and local enrichment. Matching the timed circulating flushing and fine crystal automatic elimination system, it greatly reduces scaling and blockage risks. The whole unit supports long-term continuous operation with minimal manual intervention, lowering enterprise daily maintenance and downtime losses.
4. Diversified Customization & Intelligent Compatibility
Based on the standard 85m3 main body, we provide targeted material customization including 304/316L stainless steel, duplex steel and pure titanium to adapt to corrosive, high-viscosity and special working conditions. It can be freely matched with intelligent PLC automatic control, remote monitoring, automatic alarm and unmanned discharging systems to build modern intelligent crystallization production lines.
Advanced R&D & Custom Design Capabilities
Our technical team adopts advanced CFD fluid simulation and structural mechanical stress analysis to complete iterative optimization for the 85m3 DTB crystallizer.
We independently optimize core parameters such as draft tube flow velocity, baffle spacing angle, circulating shear force and tank pressure tolerance, solving the industry pain points of unstable grading and low efficiency of variable-load crystallization equipment. Each unit undergoes strict hydraulic pressure testing, welding nondestructive inspection and simulated working condition debugging before delivery. We support personalized structural optimization and process parameter adjustment according to customers' unique material characteristics, production capacity goals and site conditions, realizing tailored industrial crystallization solutions.
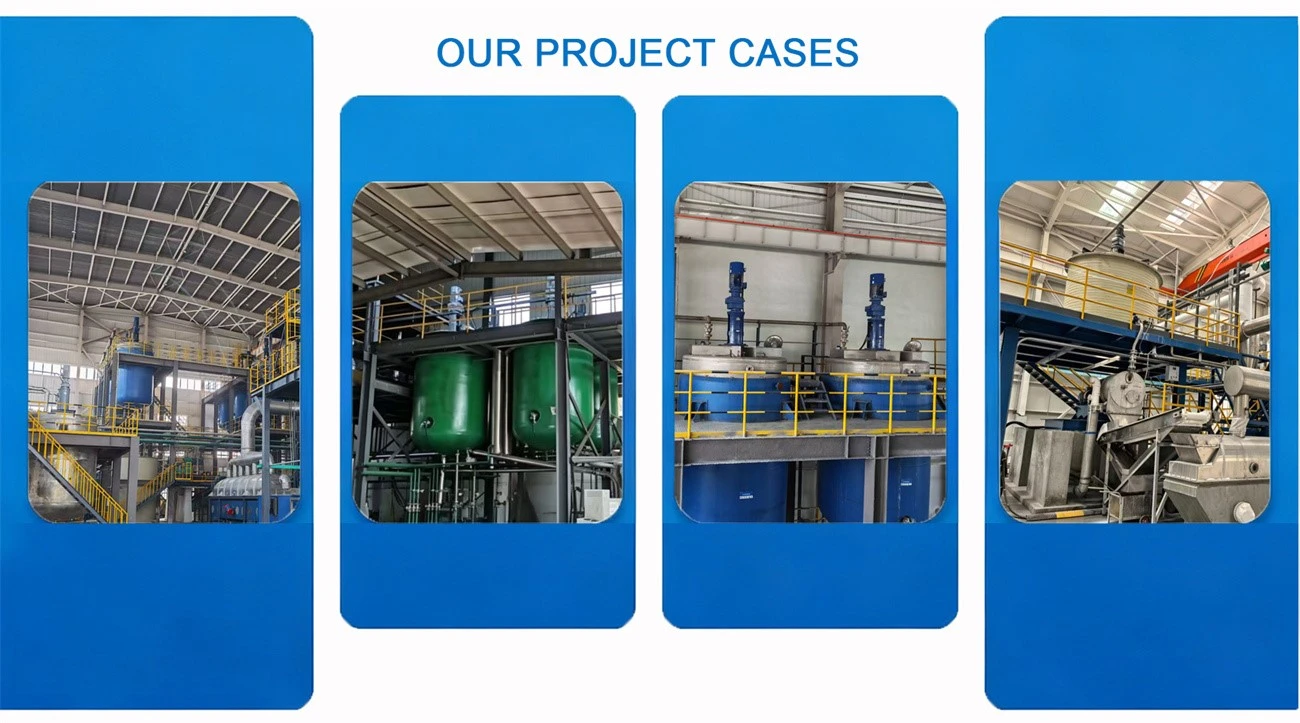
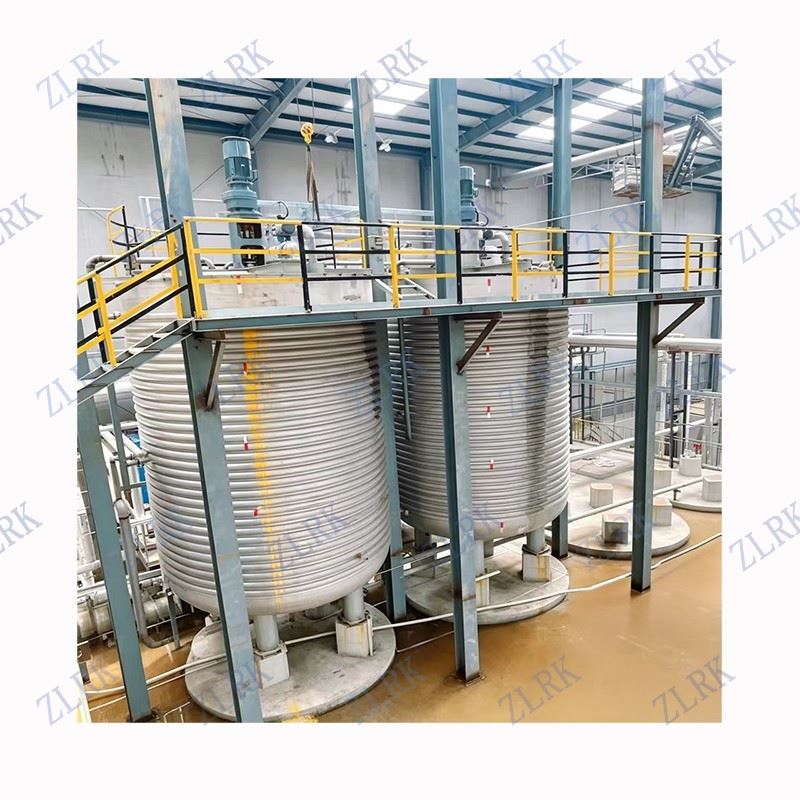
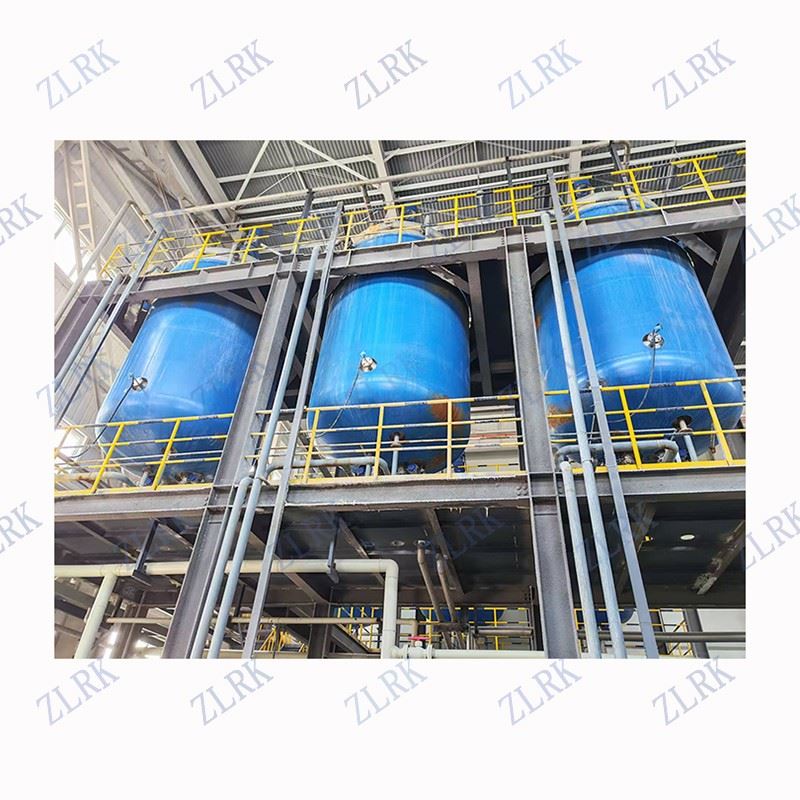
Our 85m3 DTB crystallizers have been widely applied in domestic and overseas chemical parks, environmental protection zero-discharge projects and new energy material production bases. We have accumulated rich practical experience in variable-load continuous crystallization, mixed salt separation and high-purity material refining. All delivered equipment maintains stable and efficient operation in complex industrial environments, with low failure rate and long service life. Our reliable product performance and professional engineering services have earned long-term trust and stable cooperative relationships with global industrial clients.
Full-Lifecycle Standard After-Sales System
We provide full-process one-stop services for all 85m3 DTB crystallizer users. In the pre-sale stage, we offer free working condition assessment, process scheme design and parameter matching optimization. During production, strict quality control and standardized assembly procedures are implemented to ensure international-grade product quality. After delivery, we provide detailed installation manuals, remote technical guidance, on-site commissioning and operator training. We also offer long-term regular maintenance, fault rapid response, original spare parts supply and technical upgrade services to fully guarantee the long-term stable and efficient operation of customer production lines.
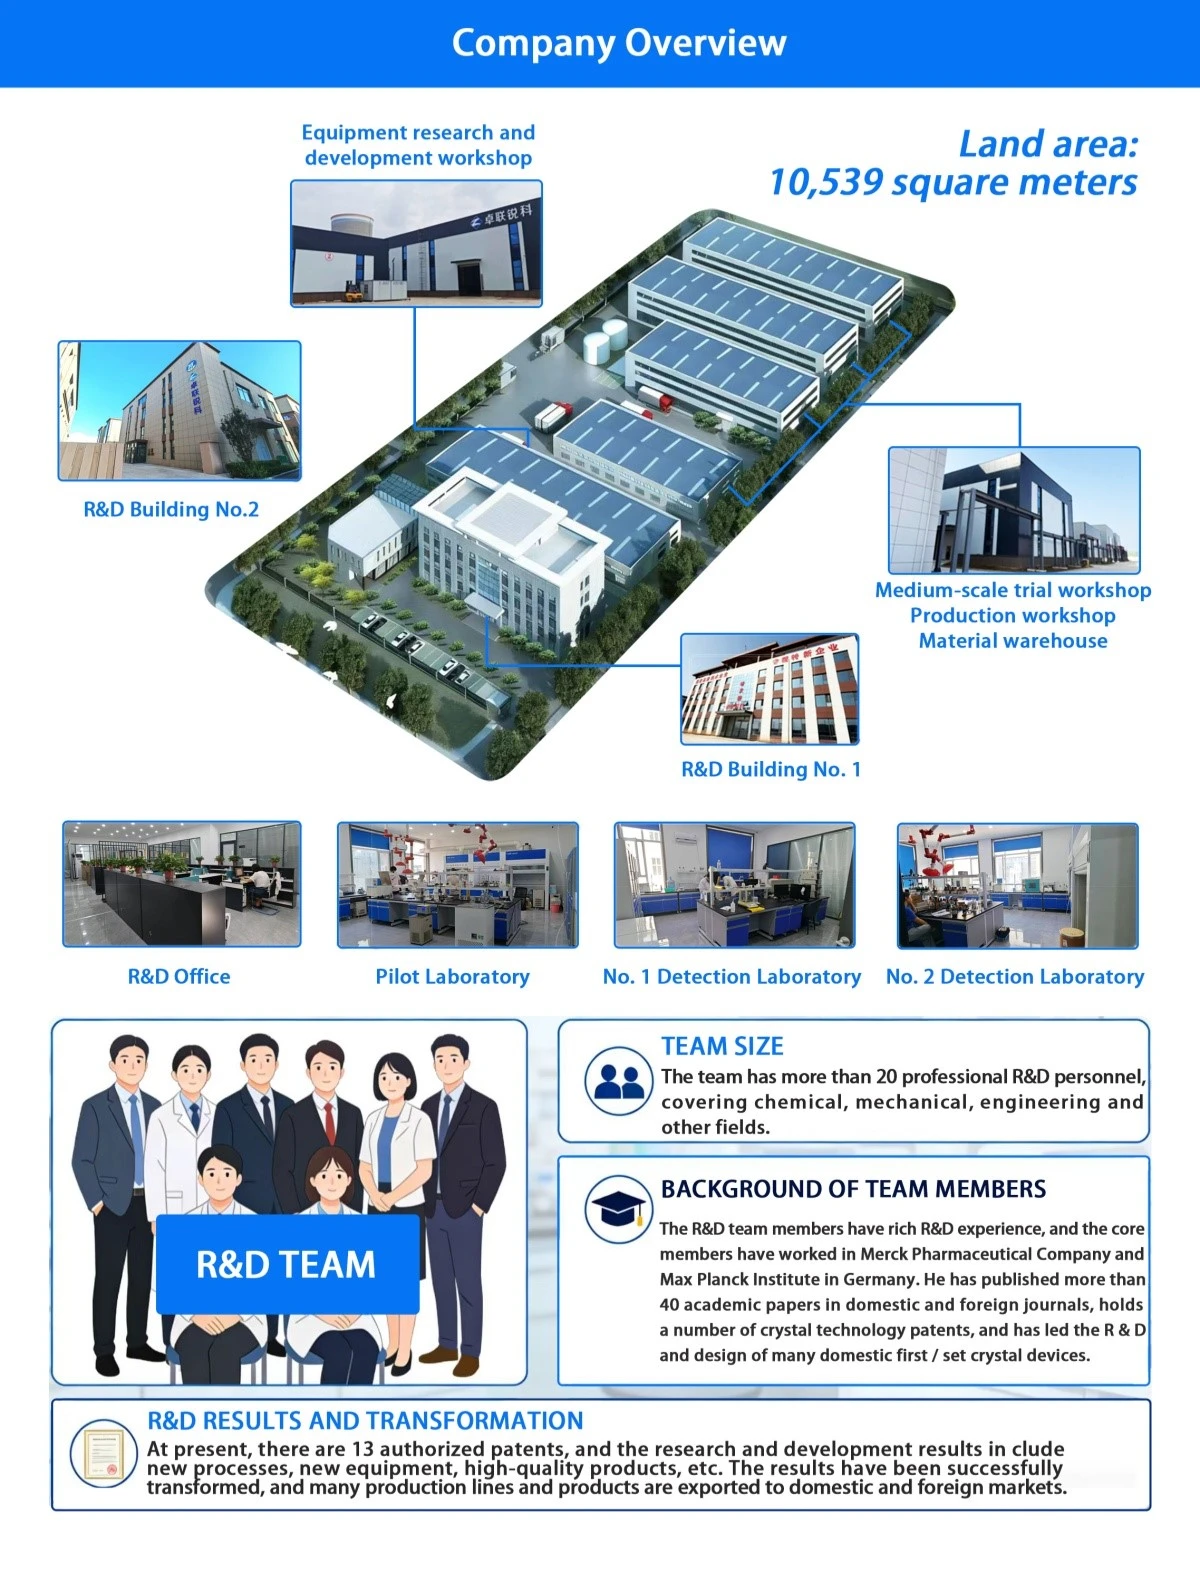
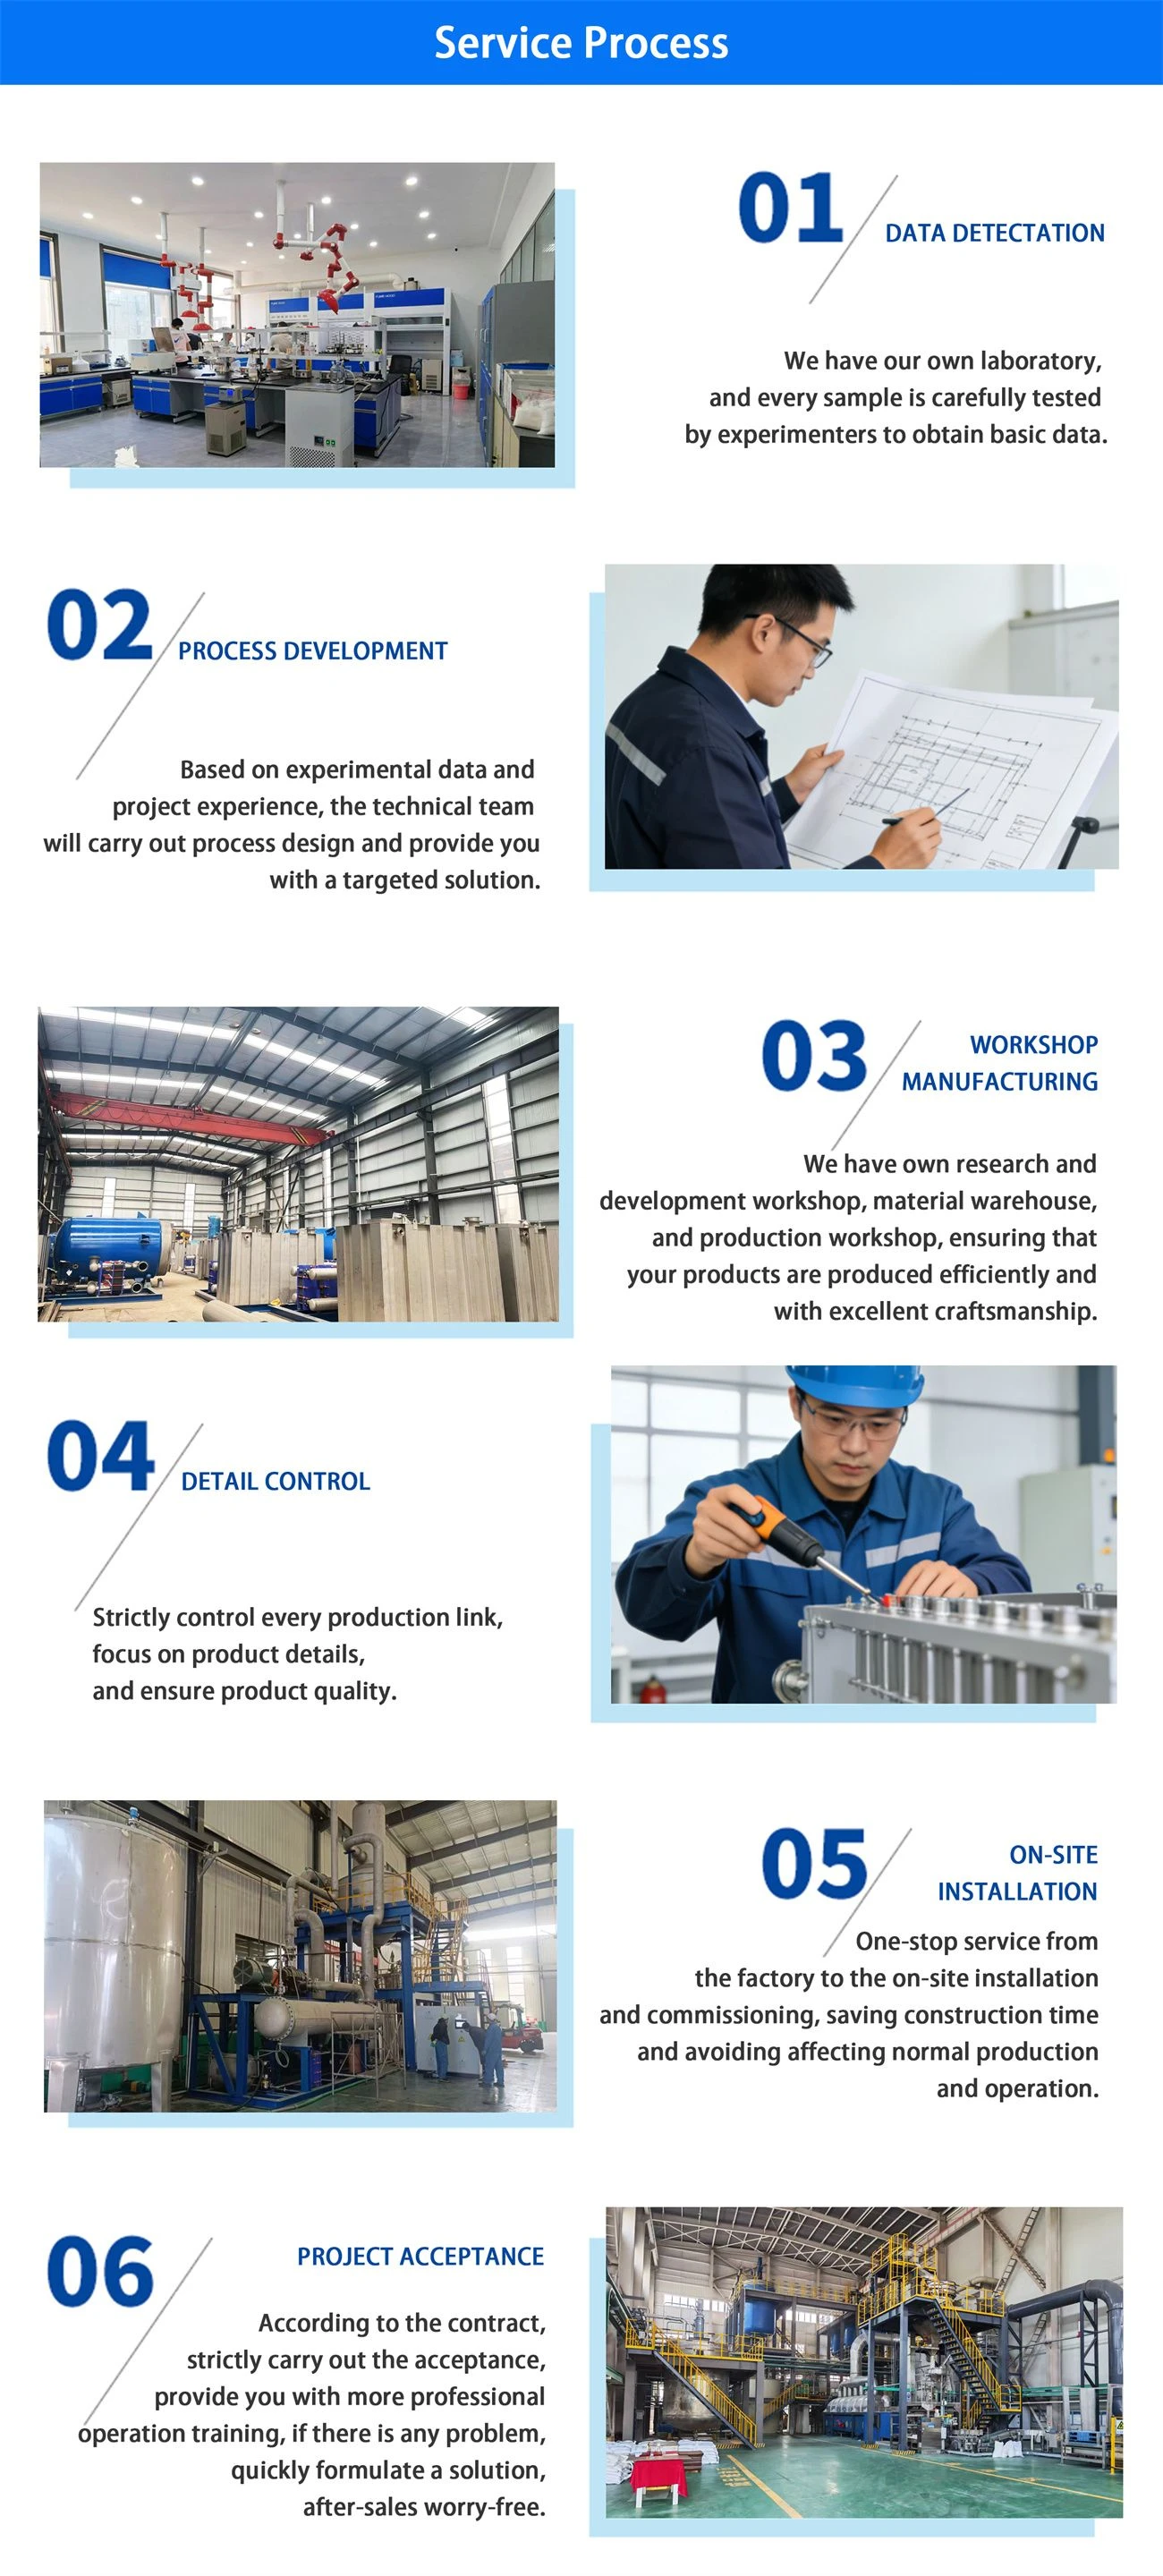
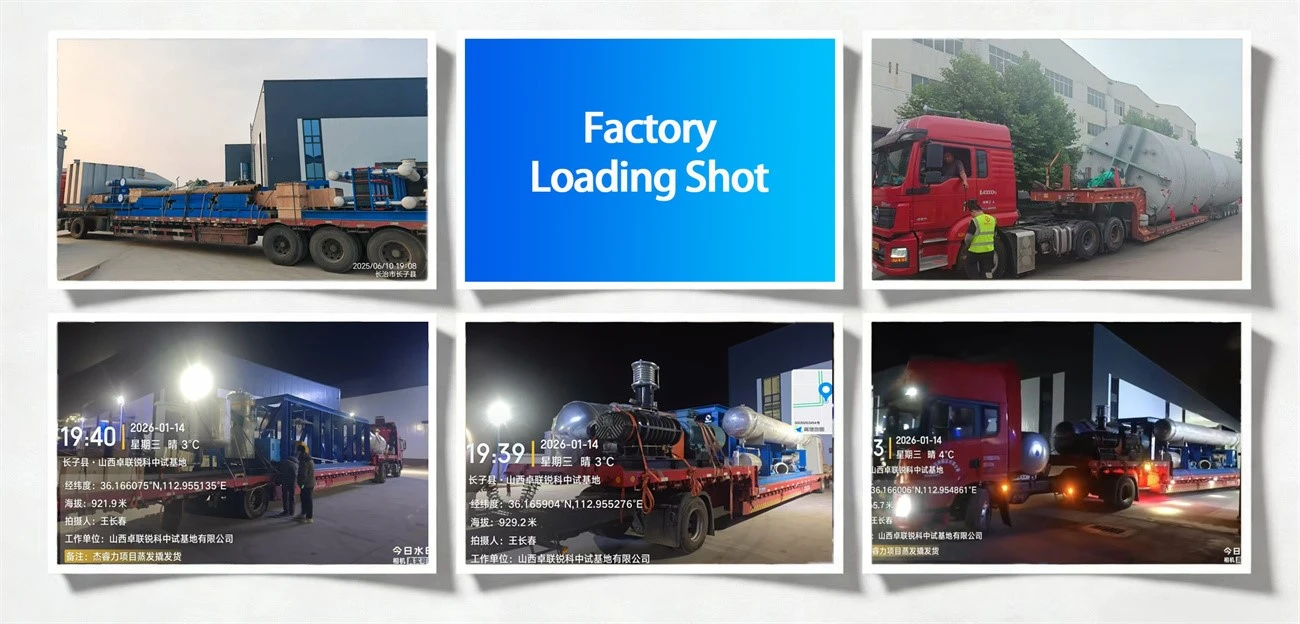
Get in touch with us for detailed equipment parameters, authentic project cases and competitive factory quotations to customize your exclusive large-scale crystallization solution!
Hot Tags: 85m³ dtb crystallizer, China 85m³ dtb crystallizer manufacturers, suppliers, factory


