
OSLO Crystallizer Product Overview
The OSLO crystallizer is a classic graded suspension crystallization device that is widely used in the chemical, metallurgical, and pharmaceutical industries.
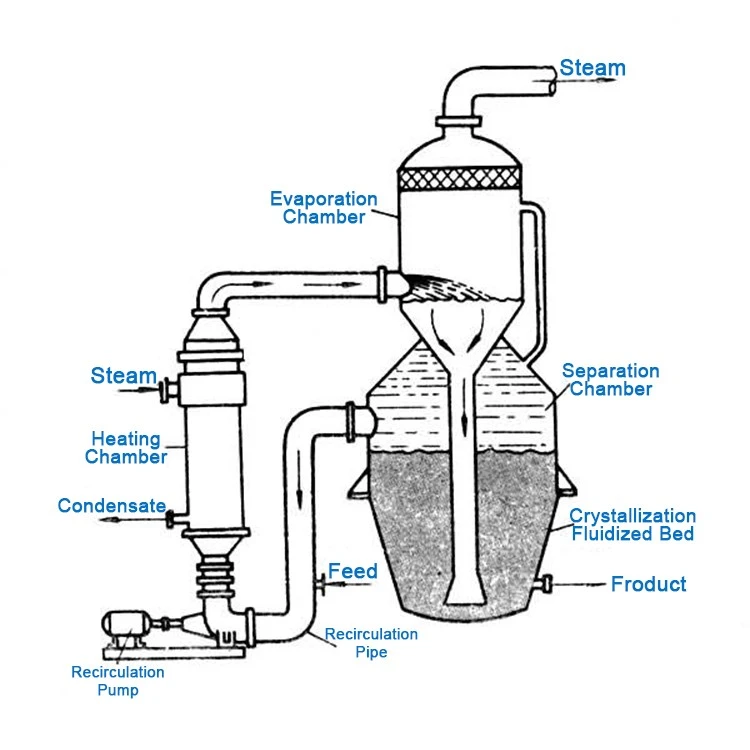
OSLO Crystallizer for High-Purity Large-Crystal Industrial Continuous Crystallization: Developed for global industrial high-standard crystallization scenarios, the OSLO Crystallizer is a professional classified suspension growth-type crystallization equipment, uniquely designed for large-particle, uniform-size crystal production and low-fine-powder material purification.
Different from conventional turbulent crystallization devices, this OSLO-type unit adopts a core fluidized bed graded growth structure, separating crystal nucleation and growth zones independently to eliminate particle fragmentation and secondary nucleation chaos. It is a high-value solution targeted at mid-to-high-end industrial fields that prioritize crystal consistency, high purity and low loss, widely applicable to standardized production and resource regeneration of inorganic salts, new energy materials and fine chemicals.
Product Profile & Working Principle
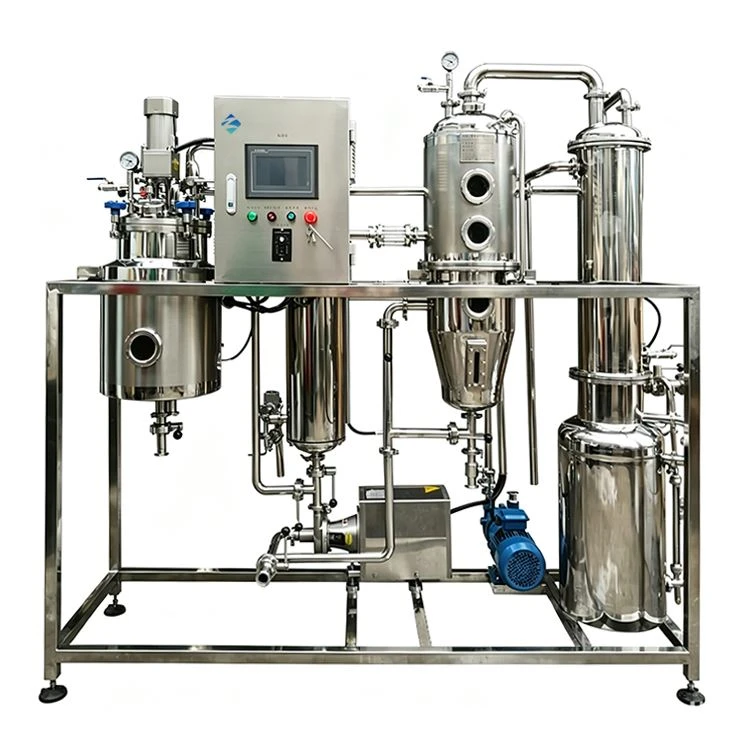
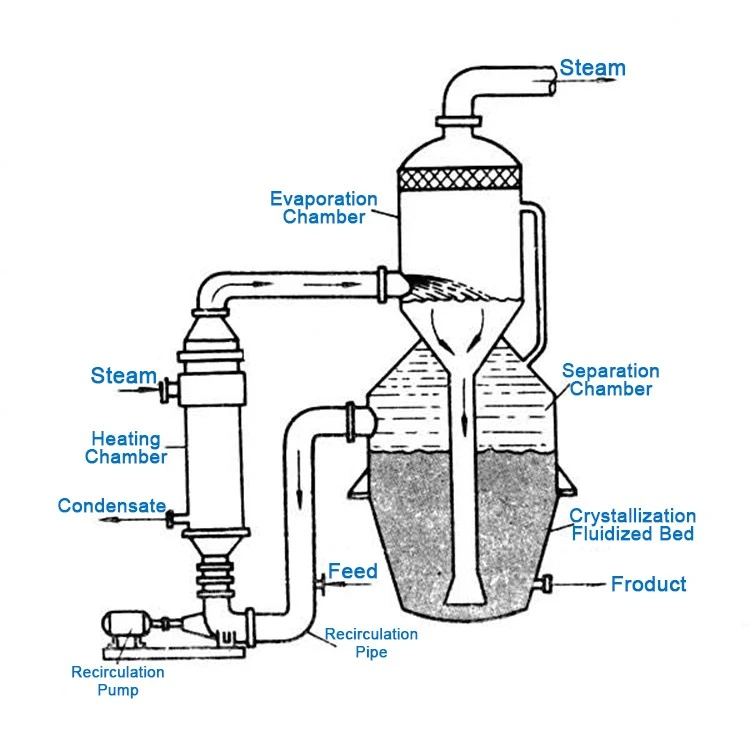
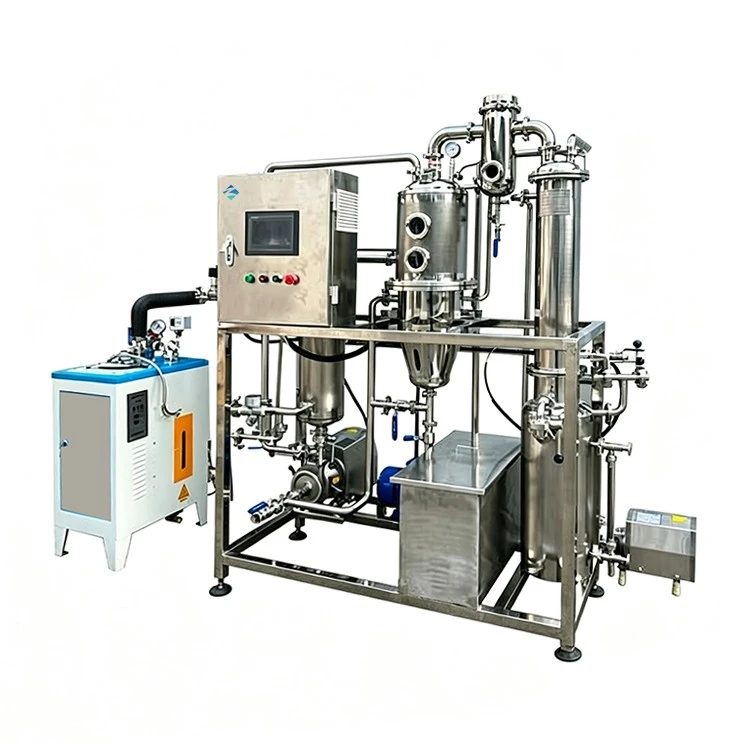
The OSLO Crystallizer features a modular split structure consisting of a super-classification settling chamber, independent growth tower, external circulation heat exchange system and intelligent liquid supply module. Its core technological advantage lies in the classified suspension working mode, which completely differentiates it from traditional mixed crystallization equipment. The equipment precisely isolates the nucleation stage and crystal growth stage, creating a stable low-turbulence fluidized bed environment for crystal particle growth.
In continuous operation, clarified mother liquor and fresh feed liquid are evenly delivered to the upper growth tower after temperature adjustment and evaporation via the external heat exchanger. Under stable laminar circulation, solution supersaturation is accurately controlled within the optimal range for crystal growth rather than nucleation. Tiny microcrystals float upward with the circulating liquid and are redissolved, while qualified crystal particles sink steadily under gravity, achieving natural graded settling and layered growth. The whole process avoids mechanical shear damage to crystals, ensuring finished products with uniform particle size, high compactness and extremely low fine crystal residue, supporting stable 24/7 continuous industrial operation.
With its unique advantages of large crystal particle formation, high purification precision and stable continuous operation, the OSLO Crystallizer covers high-standard industrial production and environmental resource recovery scenarios, serving as key core equipment for high-end manufacturing lines:
High-Grade Inorganic Salt Production: Perfect for crystallization and purification of sodium chloride, ammonium sulfate, potassium chloride and other high-purity industrial salts. It stably produces large uniform crystal particles, effectively improving product grade and market competitiveness for salt manufacturing enterprises.
Industrial Wastewater Resource Reuse: Suitable for targeted treatment of single-component high-salt wastewater in chemical, printing and dyeing industries. It realizes efficient salt-water separation and clean resource recovery, meeting international zero-discharge environmental standards and reducing enterprise resource consumption costs.
New Energy Raw Material Refining: Widely used in purification and crystallization of lithium carbonate, lithium hydroxide and other battery raw materials. The low-shear growth structure protects material structural activity, effectively removing impurities and meeting ultra-high purity requirements for new energy battery materials.
Fine Chemical & Pharmaceutical Intermediate Crystallization: Adaptable to crystallization of heat-sensitive and high-value fine chemical products. Accurate supersaturation and temperature control prevents product decomposition and deterioration, significantly improving finished product yield and purity stability.
Exclusive Manufacturer & Product Core Advantages
1. Independent Zonal Growth, Ultra-Uniform Crystal Size
Adopting exclusive nucleation-growth separation technology, the OSLO Crystallizer builds a stable fluidized bed growth environment. It effectively suppresses disorderly secondary nucleation caused by liquid turbulence and mechanical stirring. The finished crystals feature uniform particle size distribution, fewer fine powders and higher bulk density, greatly reducing the pressure of subsequent filtration, drying and screening processes and lowering overall production loss.
2. External Circulation Heat Exchange, High Energy Efficiency & Stable Operation
Equipped with an independent external heat exchange system, the equipment avoids scaling and local overheating problems of built-in heat exchange structures. The circulating liquid fully contacts the heat exchange medium with high heat utilization efficiency, realizing precise and stable temperature control. The whole system operates with low resistance and low energy consumption, adapting to long-cycle uninterrupted industrial production and reducing operational energy costs.
3. Low Shear Structure, No Particle Fragmentation
Different from traditional stirred crystallizers, the OSLO model relies on natural liquid circulation and gravity settling for crystal growth and separation, without violent mechanical stirring. The low-shear operating environment completely avoids crystal particle collision and fragmentation, ensuring the integrity of large-particle crystals and improving the rate of high-quality finished products.
4. Customized Adaptation & Intelligent Upgradability
We provide personalized material customization including 304/316L stainless steel, titanium alloy and duplex steel to adapt to corrosive, high-temperature and high-viscosity working conditions. The equipment can be matched with intelligent PLC automatic control, real-time data monitoring, automatic feeding and discharging linkage systems, realizing unmanned intelligent operation of the whole production line.
Professional R&D & Precision Design Capabilities
Our R&D team relies on advanced CFD fluid dynamic simulation and thermal field analysis technology to conduct targeted optimization for OSLO crystallizer flow field, heat exchange efficiency and graded settling performance.
We iteratively optimize core parameters such as growth tower height, circulation flow rate and settling chamber gradient, solving the industry pain points of uneven crystal growth, low heat exchange efficiency and easy scaling.
All equipment undergoes strict pressure resistance testing, air tightness inspection and simulated working condition debugging before delivery. We support personalized structural adjustment and process parameter customization according to customer material characteristics, production capacity requirements and site layout, providing one-stop targeted crystallization technical solutions.
Global Industrial Project Practice Experience
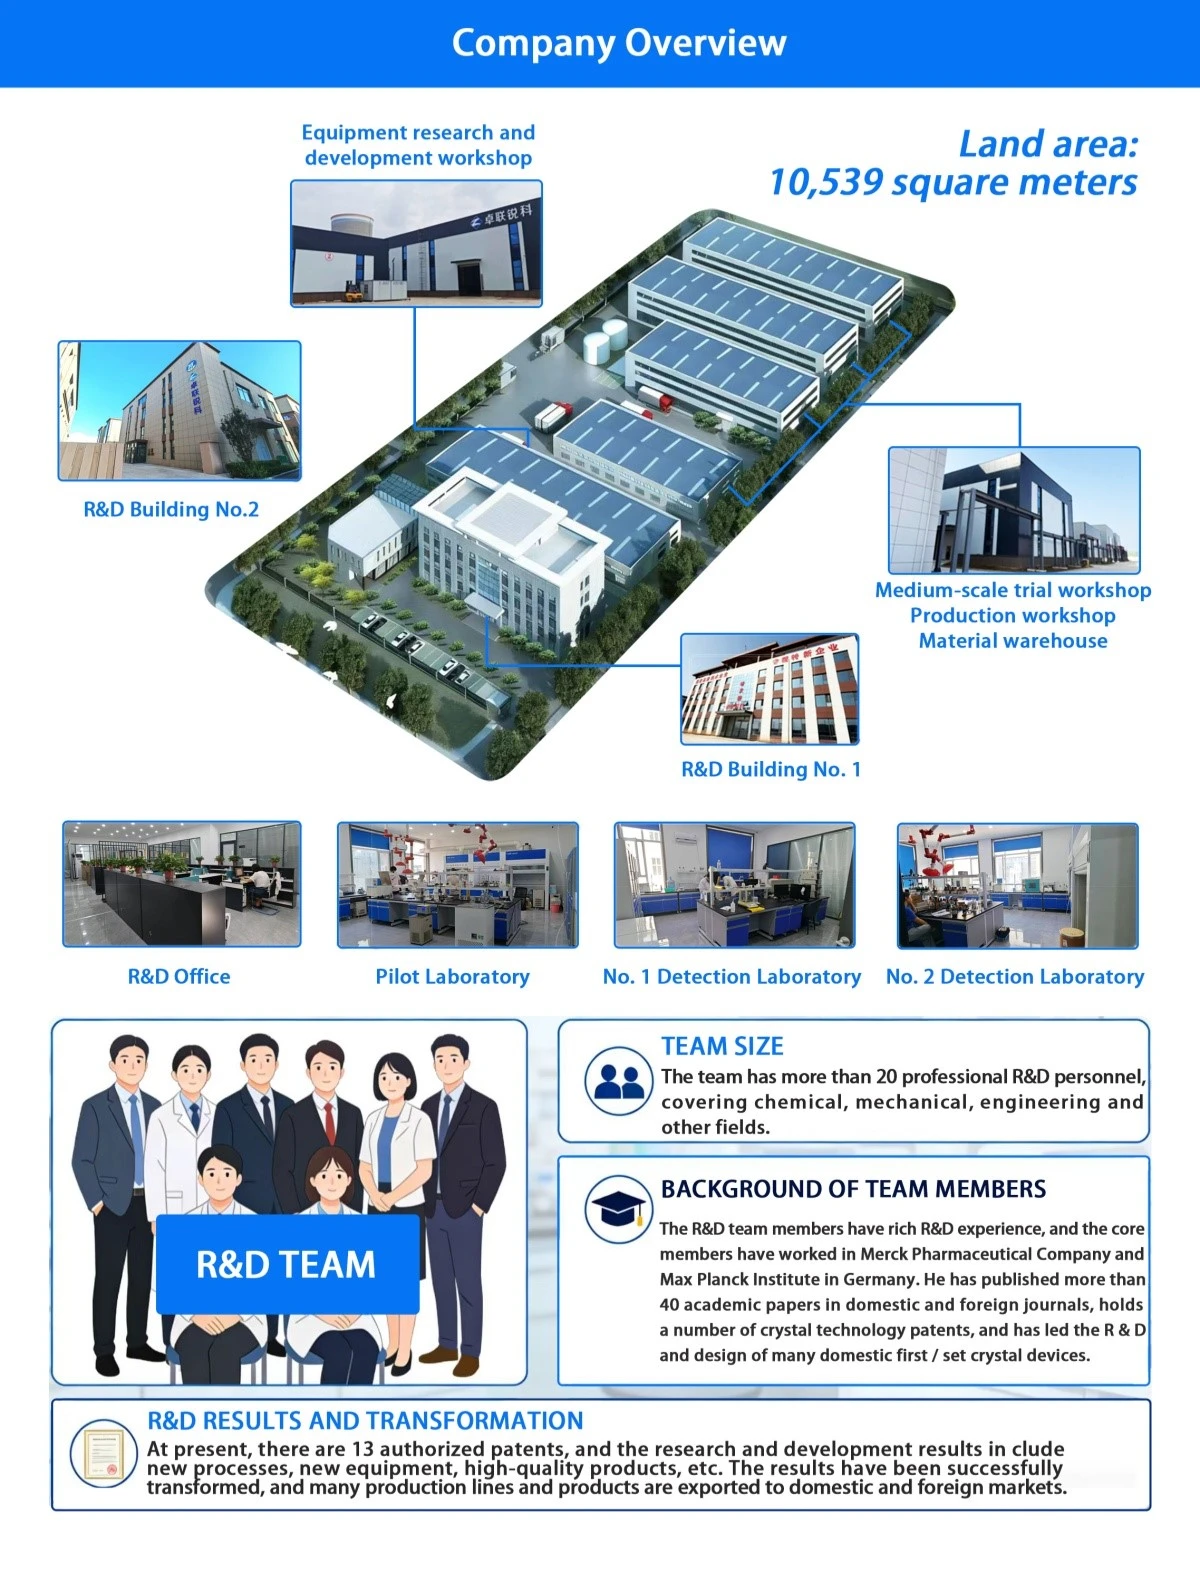
Our self-developed OSLO crystallizers have been successfully applied in dozens of industrial projects across domestic and overseas markets, covering new energy material bases, fine chemical parks and environmental protection zero-discharge projects. We have accumulated mature practical experience in high-purity crystal production, single salt precise separation and long-term stable operation of equipment in complex working conditions. All delivered equipment maintains low failure rate, stable performance and long service life in actual production, winning consistent recognition and long-term cooperative intentions from global industrial customers with reliable product quality and professional engineering service capabilities.
Full-Cycle Professional After-Sales Service System
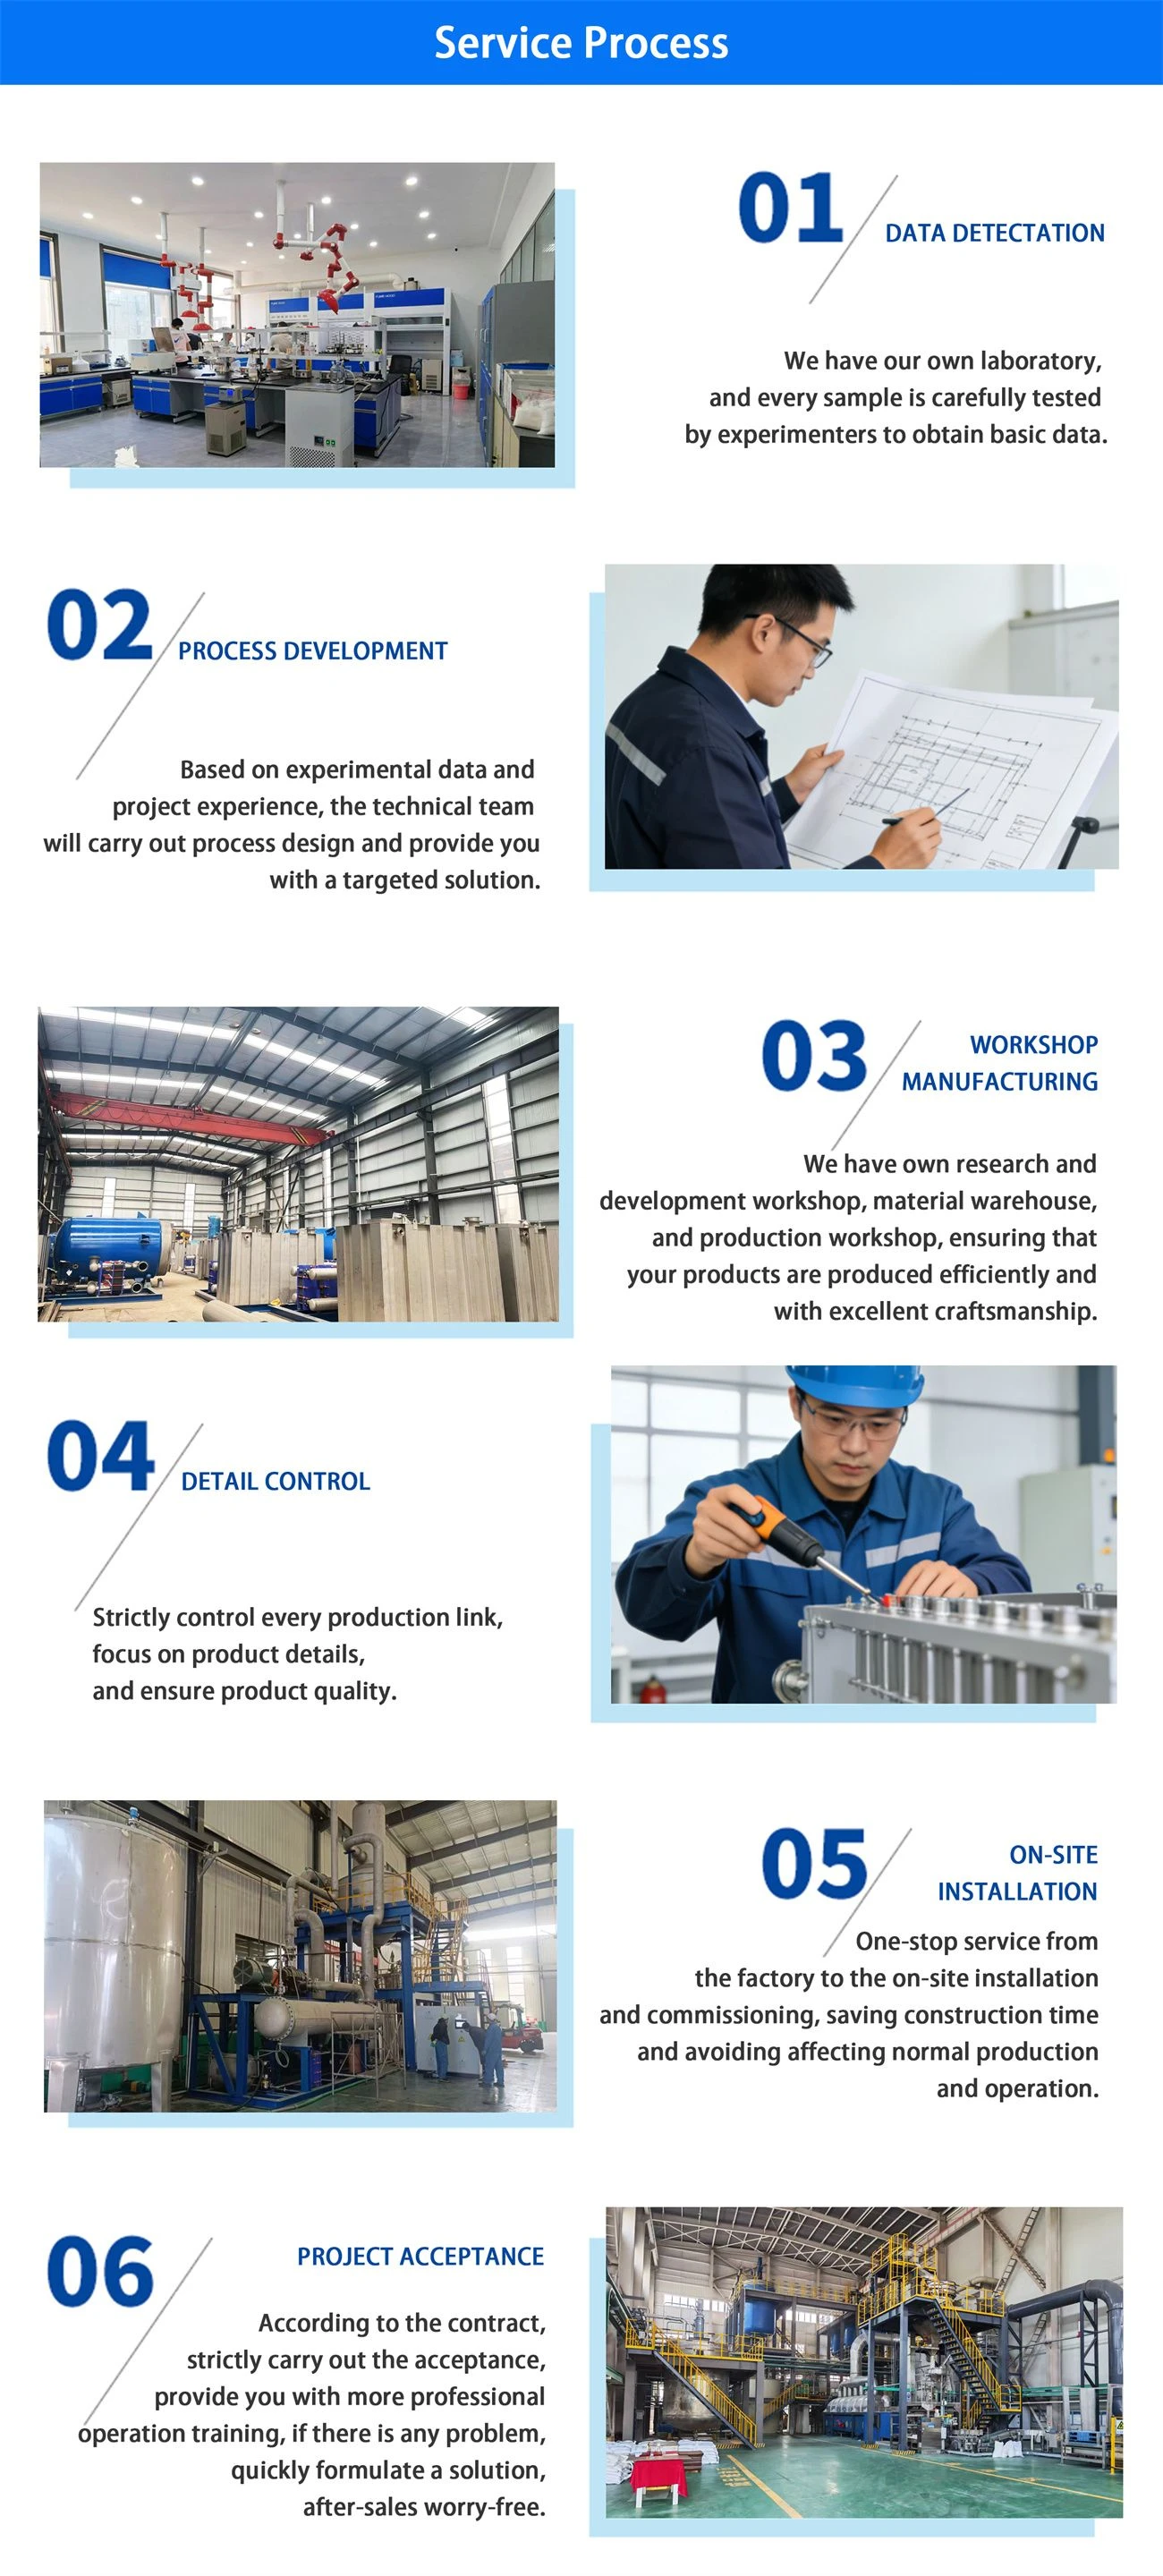
We provide full-lifecycle one-stop supporting services for all OSLO crystallizer users. In the pre-sale stage, we offer free working condition investigation, process scheme demonstration and production capacity matching optimization. During production and processing, we implement standardized quality inspection procedures to strictly control every production link. After equipment delivery, we provide detailed installation guidance, on-site commissioning and professional operator training. In the after-sale stage, we offer long-term regular equipment maintenance, rapid fault response, original spare parts supply and technical upgrade services, fully ensuring the stable, efficient and long-term operation of customer production lines.
Product-Related Keywords
Crystallization Equipment; Crystallization System; 0.5 tons–10 tons per hour OSLO Crystallizer.
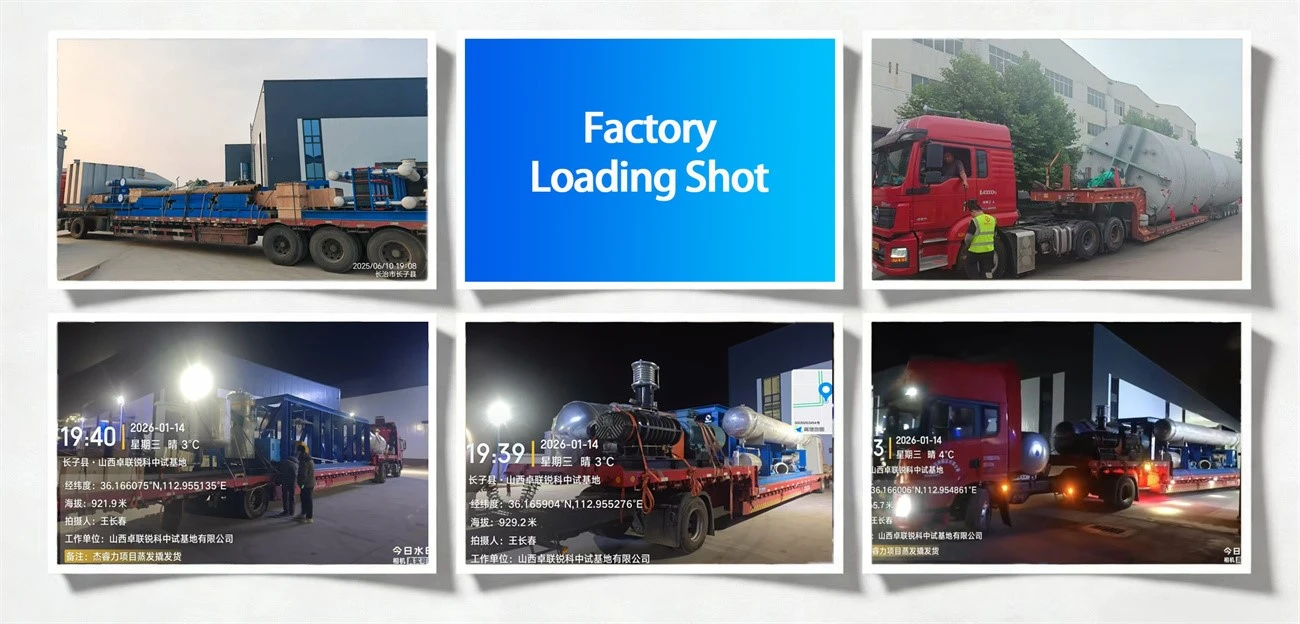
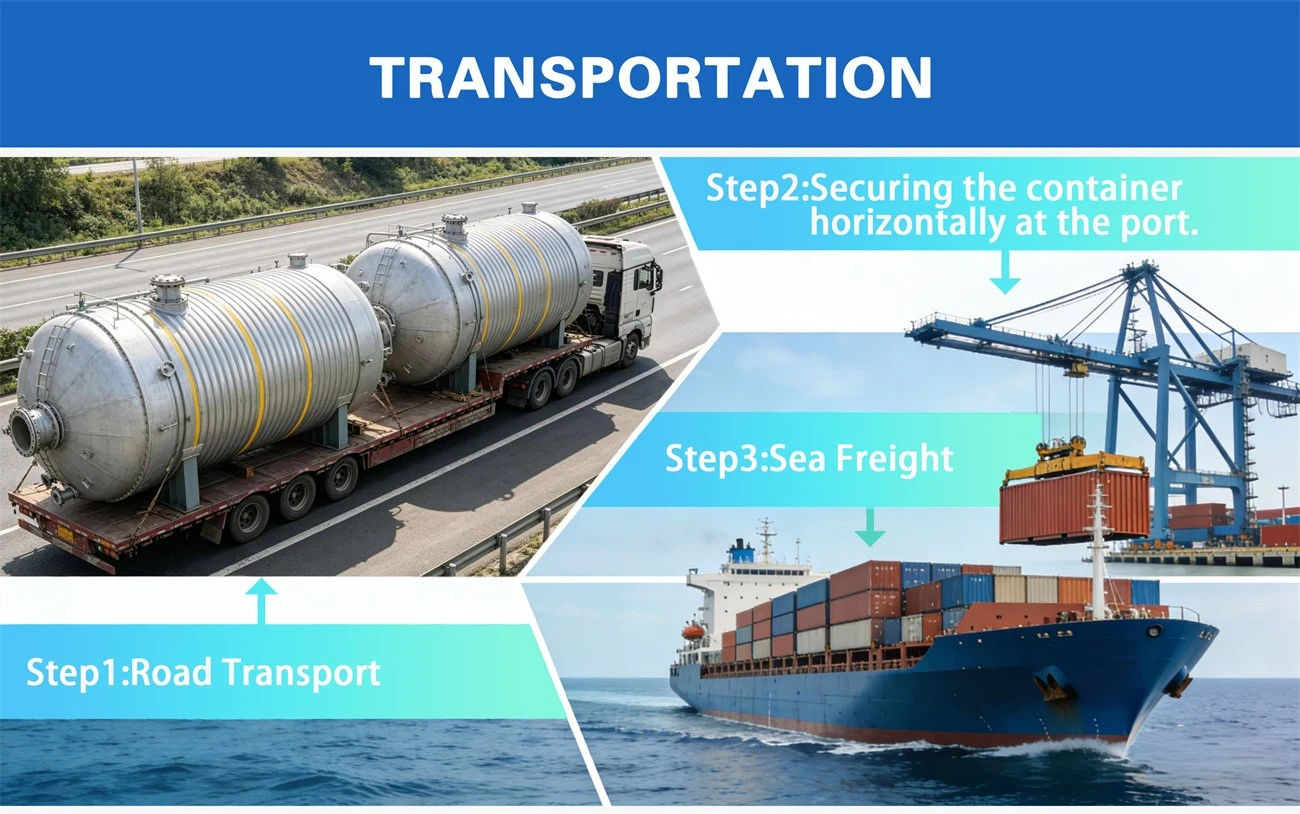
Packing, Loading and Transportation
Contact our team now to obtain detailed equipment specifications, real overseas project cases and factory preferential quotations, and customize your exclusive high-efficiency OSLO crystallization production solution!
Hot Tags: oslo crystallizer, China oslo crystallizer manufacturers, suppliers, factory


